Monthly Archives

August 2026

Why this is a real problem

Battery systems look simple on paper but they fail in predictable ways when corners are cut. If you ignore a few safety checks you’ll end up troubleshooting during a heatwave or a blackout — and that’s exactly what utilities saw during recent California heatwaves. For anyone sizing or operating systems, integrate a home energy management system early so you can see limits, alarms, and trends before people notice the problem.

Top safety features to verify — practical checklist

Start by confirming these items with vendors and site teams. Don’t assume they’re built-in just because the datasheet looks tidy.- Battery Management System (BMS): cell balancing, cell-level volt/temperature monitoring, and clear fault outputs. Know the fault states and what they trip.- Thermal runaway detection: smoke/temperature sensors placed at cell modules, with automated isolation logic.- Hardware disconnects: accessible AC and DC rapid disconnects and clear labelling for first responders.- Venting and enclosure rating: confirm IP/NEMA rating and planned ventilation routes for any off-gassing.- Fire suppression compatibility: active suppression must match battery chemistry; checklist the agent, activation triggers, and service intervals.- Cooling controls: verify cooling capacity for worst-case ambient temps, not just nameplate ratings.- Overcurrent protection: breakers/fuses sized for both normal and fault conditions with proper coordination.- Firmware & logging: automatic update policies, signed firmware, and persistent logs for faults and state-of-charge history.- Commissioning tests: full-load, simulated-fault, and safe-failure-mode tests with documented passes.- Training & SOPs: one-line diagrams, emergency isolation steps, and hands-on drills for installers and facilities staff.

Integration pitfalls that cause incidents

Most problems happen at the interfaces. Check these common weak spots.- Incorrect inverter handshake: limits not enforced lead to overcharge or unintentional islanding.- Poor telemetry: delayed alarms mean a small fault becomes big. Link this to smart energy management solutions for centralized view and automated responses.- Misassigned responsibilities: operations thinks vendor handles firmware; vendor thinks integrator does site commissioning.- Oversized strings without proper fusing: big energy + small protective device equals a bad day.

How to evaluate alternatives quickly

You’re choosing between pre-integrated cabinets, rack systems, and modular micro-packages. Trade-offs:- Pre-integrated cabinets: faster install, but inspect internal wiring and spare parts list.- Rack systems: more customization; require tighter commissioning discipline.- Modular micro-packages: easier to expand, but watch for cumulative thermal effects.Pick the option that matches your maintenance model, not just upfront cost. Run the same commissioning checklist regardless of the form factor.

Common commissioning mistakes to avoid

Don’t skip the simple tests that matter.- Skipping simulated-faults: a system that never sees a fault during commissioning will fail unpredictably in the field.- Ignoring degraded-cell behavior: test under partial-charge and elevated temperature.- Not validating alarms end-to-end: alarms should reach operators and trigger the intended automated actions.- No post-install training: handover docs must match the installed system, not the spec sheet.

Quick on documentation and accountability

Demand these deliverables before sign-off: updated as-built drawings, test logs with timestamps, firmware versions, spare-parts list, and a named on-site contact who’s trained. Make maintenance intervals and escalation paths part of the contract.

Final take — what actually protects people and assets

Start with the problem: unknown faults turn routine installs into emergencies. Verify BMS behavior, thermal controls, disconnects, and end-to-end telemetry. Validate the whole chain with commissioning tests and clear operator procedures so the system behaves predictably under stress. Practical, documented steps beat fancy feature lists every time, which is why teams often compare real-world performance and specs with Ktech as part of deployment planning — it helps match product capabilities to the procedural protections you need.
0 comments
0 FacebookTwitterPinterestEmail

Wake-up call: what’s actually at risk?

Too many projects start soft and end up stranded. You want a system that stands up under pressure — not excuses. Ask whether their proposal centers on reliable hardware like a 150kW battery inverter sized to handle realistic peak slices, and watch how they react. I’ve seen designs that failed basic resilience checks after Hurricane Maria in Puerto Rico; that’s the kind of real-world lesson that should make you strict about specs and testing.

Ten direct questions that expose weak vendors

Don’t accept fluff. Use these sharp, specific questions to separate talkers from doers:- How will you size and justify the diesel storage hybrid system architecture for our load profile and fuel constraints? – What’s the expected round-trip efficiency and thermal derate for the batteries at our site temperatures? – How do you manage islanding and seamless transfer under fault conditions? Provide test records. – Who owns commissioning tests, and can you share a commissioning checklist with pass/fail criteria? – What maintenance tasks are critical in year one and which ones the owner must schedule? Include intervals and skill level required. – Show fault-history examples: how did you diagnose and fix at least two past failures? – What are the firmware update and cybersecurity procedures for inverters and controllers? – Provide lifecycle cost projections: capital, fuel, replacement, and disposal, with assumptions. – What local permitting or interconnection hurdles have you cleared for similar projects? Name the jurisdiction. – What training and on-site handover do you deliver — and what documentation stays with the owner?

Why each question matters — and what a good answer sounds like

Bad answers dodge specifics. Good answers give numbers, documents, and timelines:- Sizing: they should quote worst-case peak, contingency margins, and a sequence-of-operations diagram. – Efficiency & temperature: expect a degradation table and thermal management plan. – Islanding: insist on test logs showing <30 ms transfer without load interruption or a clear plan if not possible. – Commissioning: a supplier should hand you signed test reports, not an invoice alone. – Maintenance: require a tiered checklist — daily, monthly, annually — with recommended spare parts. – Failure history: credible teams narrate past incidents and the corrective steps; that’s proof they learned. – Cybersecurity: firmware policy + secure remote access and role-based accounts. No vague “we secure it.” – Lifecycle costs: numbers with assumptions. If they can’t model fuel savings and replacement timing, they’re guessing. – Permitting: name-check a local authority where they completed interconnection. – Training: expect on-site, hands-on sessions and digital manuals you can search.

Common traps that kill projects

Spot these and stop the bleed:- Under-rated components that survive lab tests but fail in hot, dusty field conditions. – One-off custom control code without source custody or rollback plans. – No spare-parts kit or long lead-time items locked to a single supplier. – Commissioning left as a checkbox — no real performance verification. – Overly optimistic lifetime assumptions for batteries and diesel gensets. Fix these now. Push vendors to commit in writing.

What competent teams deliver — proof, not promises

Look for these deliverables:- Detailed sequence-of-operation diagrams and protection settings. – Signed commissioning reports with witnessed tests. – A spare-parts list, procurement lead times, and a training package with competency checks. – Clear warranty coverage: components, BMS, and workmanship — with response SLAs. I’ve led commissioning teams and watched how documentation separates reliable builds from risky ones. Experience shows the difference.

Negotiation moves that actually change outcomes

Be relentless. Tie payment milestones to verified performance. Require a two-week performance window where fuel use, ramp rates, and islanding behavior must meet the contract. Ask for penalties or holdbacks for missed targets. Demand access to telemetry during the warranty period. Vendors that balk here aren’t confident in their work.

Final push — make decisions like you mean business

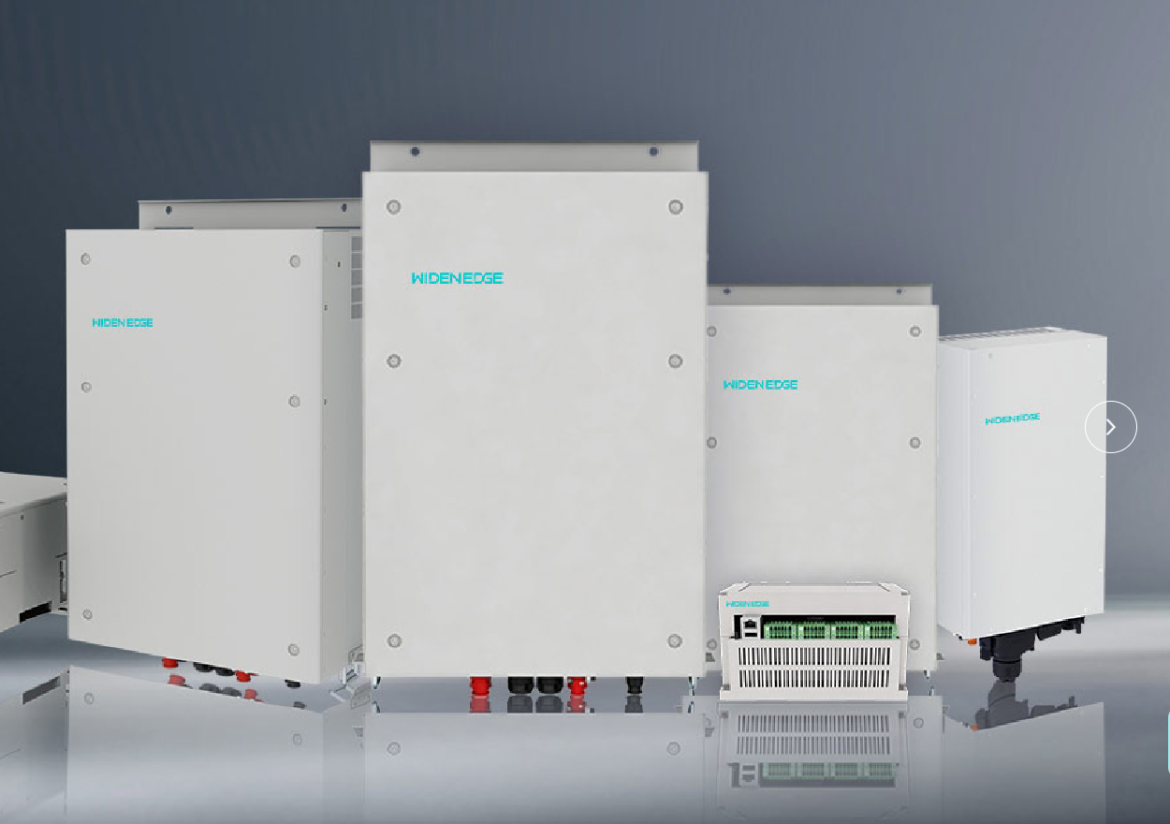
Stop being polite. Ask the hard questions. Require test evidence. Hold vendors accountable for spares, training, and clear operations. The right supplier will give firm numbers, signed reports, and a plan that fits your risk tolerance. If you want a partner who designs, tests, and stands by the outcome, consider teams with field-proven processes and a pragmatic approach from design to handover, like those you’ll find at WidenEdge.

0 comments
0 FacebookTwitterPinterestEmail

Why Procurement Teams Favor Enclosed Powder 3D Systems Over Open Alternatives

Comparative logic behind the purchasing tilt

Procurement teams at multinational R&D groups focus on predictable outcomes, not hype, which is why fully enclosed powder systems often top shortlists. Enclosures control the build chamber environment and help standardize repeatability across locations — a real advantage when teams in Munich and Singapore must reproduce the same prototype geometry. For many of these teams, moving from an experimental fdm 3d printer workflow to a controlled powder-based cell reduces variation and failure rates during scale-up.

Safety, compliance, and operational risk

Powder handling is a hard constraint: containment, inert gas management, and filtration matter. Enclosed machines cut airborne particle exposure and make it simpler to document engineering controls for EHS reviews. R&D procurement prioritizes systems that log chamber pressure, oxygen ppm, and purge cycles because those metrics feed into safety audits and traceability. The payoff is fewer shutdowns and clearer compliance artifacts during internal audits and partner reviews.

Performance: repeatability, throughput, and part quality

Teams measure machines by cycle-to-cycle consistency more than peak speed. Enclosed powder systems deliver consistent layer resolution, tighter tolerances, and predictable thermal histories. That translates to fewer surprises during post-processing and more reliable mechanical properties from one batch to the next. Real-world anchors matter: space agencies’ ISS 3D printing experiments underscored how controlled environments produce mission-critical parts with consistent properties — a lesson procurement teams use when evaluating industrial builds.

Cost of ownership and lifecycle thinking

Upfront capital is one line item; maintenance, consumables, and qualification time are recurring costs. Enclosures often reduce waste and scrap, because part failures due to contamination or uncontrolled humidity drop substantially. Procurement models factor in downtime for recoating, filter replacement, and calibration—those predictable intervals let teams plan spares and staffing. Over five years, lower scrap rates and fewer re-runs can tilt total cost of ownership decisively.

Operational production teardown: what buyers actually test

When procurement runs a technical evaluation, they teardown workflows: build preparation, printer run, post-process, inspection. They track powder reuse cycles, sieving rates, and the time for depowdering and sintering. In these teardowns they also validate digital workflow compatibility — slicing software, build plate nesting, and data integrity. For transparency I’ve seen labs log {main_keyword} and {variation_keyword} side-by-side during pilot runs to compare material behavior and throughput. Industry terms matter here: powder bed fusion, sintering, and post-processing are tested end-to-end so the procurement team understands real throughput, not vendor claims.

Common mistakes teams make — and practical alternatives

Too many evaluations focus on max resolution or marketing benchmarks instead of operational metrics. Teams sometimes skip climate conditioning tests in their own facilities — a mistake, because humidity and ambient contaminants vary by site. Open powder benches can look attractive on price, but they demand more facility upgrades. Alternatives like binder jetting or high-end FDM can work for low-to-medium mechanical demands, but they trade off consolidation and isotropy. If post-processing capacity is limited, choosing a system with more integrated depowdering and automated part handling pays dividends. — A quick aside: operational ergonomics matter as much as throughput; technicians notice this first.

Golden rules for evaluation

Rule 1: Measure reproducibility per build cycle. Track dimensional variance and mechanical property scatter across five identical builds.

Rule 2: Quantify maintainability. Log mean time between service events and time-to-qualified-run after a consumable swap.

Rule 3: Confirm digital and materials ecosystem fit. Validate slicer output, material traceability, and powder reuse strategy using an actual part program.

Final take and where Raise3D fits

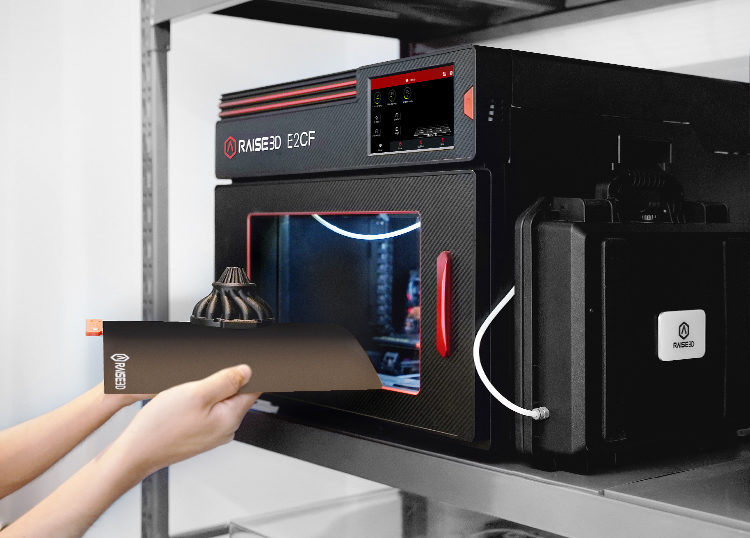
Procurement teams choose enclosed powder systems because they convert technical risk into measurable operational metrics; that’s the bridge between lab prototypes and reproducible product parts. When those teams need a vendor that balances modular workflow, reliable enclosure engineering, and a supportive supply chain, they often evaluate vendors that can demonstrate those operational strengths—one practical example being the integration and support around the raise3d pro3 plus during pilot runs. Trust comes from consistent data, not promise. Raise3D. –

0 comments
0 FacebookTwitterPinterestEmail

A buying guide to Sunjoy Hardtop Gazebos that starts with how a two-tier or gable roof changes the look for model by model shopping

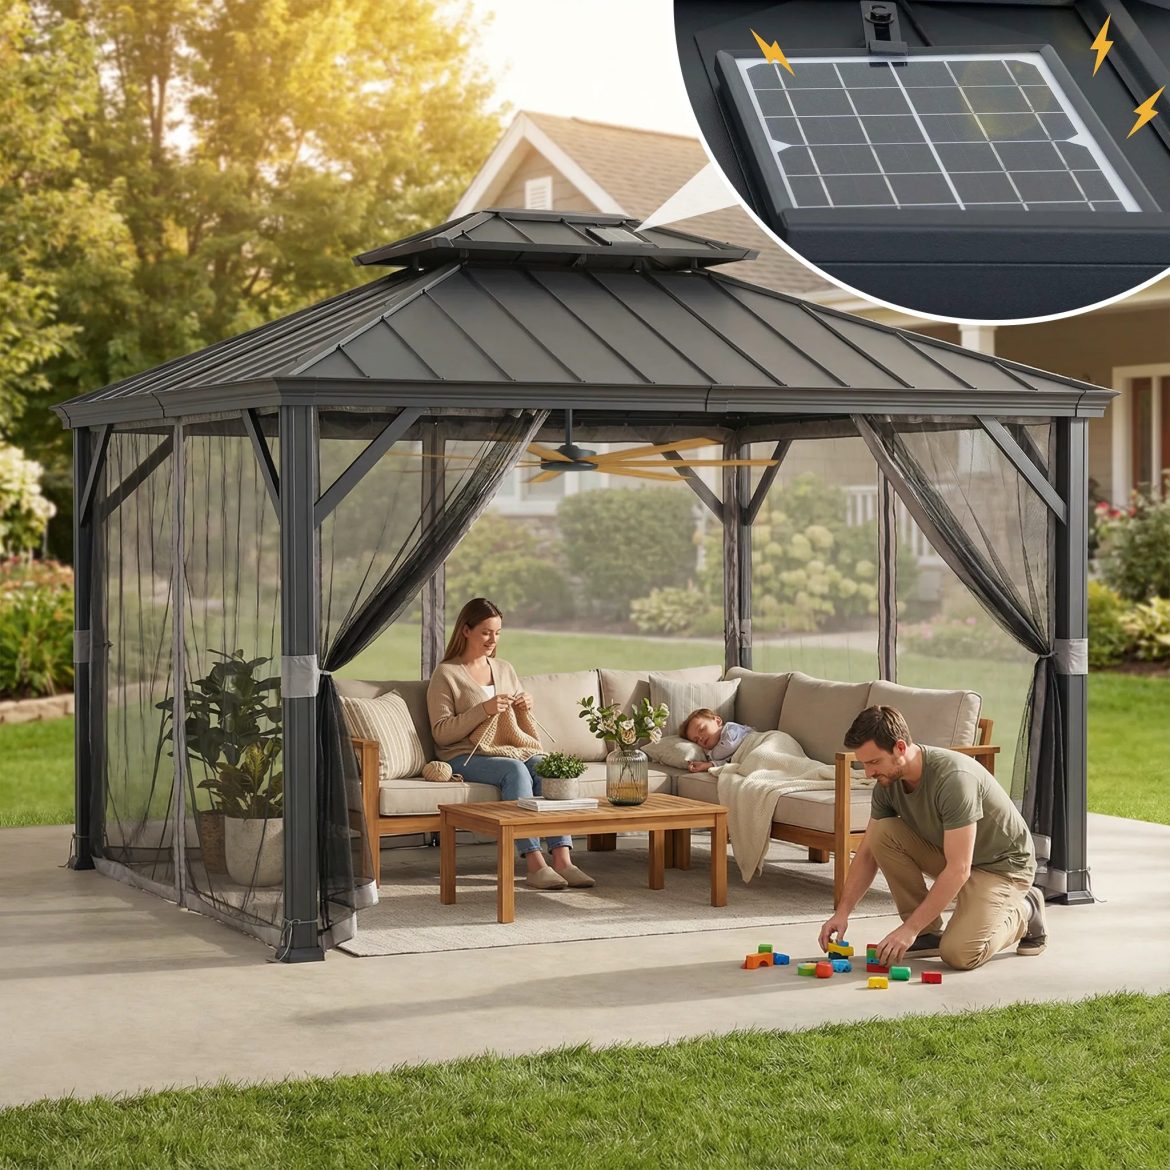
When patio plants, seating, and entertaining all compete for room, SUNJOY hardtop gazebos need to be judged as part of the whole outdoor layout. The roof is not only a shelter detail. Its shape becomes a visible part of the garden, so compare the roofline with the scale, style, and purpose of the space before focusing on individual features.

A102008100 13x15 Gable Roof Gazebo Day

Start with the visual job of the roof

A two-tier roof creates a layered profile. That can make a gazebo look more detailed and visually substantial than a simple single-plane roof. A gable roof presents a peaked form, which may suit a garden organized around strong lines, repeated angles, or a central dining area. These are design observations, not guarantees about how any one model will look in your yard. The surrounding fence, trees, furniture, and viewing distance will affect the result.

For patio gardeners, the best starting question is not simply, “Which roof style is attractive?” Ask what the structure should do visually. If the gazebo will sit behind planting beds, a more articulated roof may become a focal point. If it will share a compact patio with containers and furniture, a highly prominent roof could draw attention away from the rest of the space. Use photographs and dimensions from the specific listing to test that relationship rather than treating a collection label as a complete specification.

Compare the space before comparing the models

Map the intended footprint first. Mark the area for chairs, a table, planters, walking paths, and access around the structure. Then consider the sightlines from the house and the main garden paths. A roof can change the apparent scale of a gazebo even when the footprint seems suitable. This is especially important in a compact yard, where the structure may be viewed from several short distances.

Next, decide how often the space will be used. A gazebo intended for regular outdoor dining deserves a different review from one considered mainly as a visual feature beside a garden. List the activities before reviewing product pages: reading, eating, hosting, gardening tasks, or storing outdoor accessories. The list will help you separate essential space from attractive but unnecessary details.

Keep the comparison model-specific. The collection labels several roof styles, including two-tier and gable, as well as hip, octagon, and shed. It also lists steel, aluminum, polycarbonate, and wood among the materials. Those are useful filters for narrowing the search, but they are collection-level labels. Confirm the roof style and material on the exact model listing before treating either as part of your final choice.

Use the page evidence without overreading it

For an outdoor hardtop gazebo, the roof label can guide the first visual comparison, but it should not answer every practical question. Review the product page for the model’s stated dimensions, listed construction details, and included components. Avoid assuming that two models with similar roof names have the same configuration. A gable on one listing may not correspond to the same proportions or material combination as a gable on another.

Accessories can also shape the buying decision. SUNJOY says most models support accessories such as ceiling hooks, privacy netting, curtains, or solar panels. That does not mean every accessory applies to every model. Treat the statement as a reason to inspect the selected listing, not as a promise of universal compatibility. For a gardener, ceiling hooks may matter if the planned arrangement includes hanging items. Privacy netting or curtains may matter if the gazebo borders a neighboring property or a busy part of the yard. Solar panels may be relevant only when the selected model and intended setup support that use.

The page also includes a hard-top versus soft-top comparison covering roof materials, weather-related claims, maintenance expectations, and use contexts. This comparison can help frame the category decision, but it should not replace the details for the model under consideration. In particular, do not turn a general category statement into a guarantee about a particular roof, installation, or setting.

A practical inspection sequence

Before choosing, work through four checks. First, compare the roof silhouette with the garden’s existing forms. Second, confirm that the planned furniture and circulation fit the available footprint. Third, read the model listing for the exact roof style, material, dimensions, and included parts. Fourth, review any accessory references against that model instead of relying on the collection page alone.

Evidence-led comparison lenses
Shopping lens What the collection page lists How to use it
Roof style Two-tier, gable, hip, octagon, and shed Use the label to begin a visual shortlist, then confirm the exact style on the model listing.
Material Steel, aluminum, polycarbonate, and wood Compare the material shown for each selected model without assuming that all models share the same construction.
Accessories Ceiling hooks, privacy netting, curtains, or solar panels are supported by most models, according to SUNJOY Inspect the selected model before treating an accessory as compatible or included.
Category context The page compares hard-top and soft-top options across materials, weather-related claims, maintenance expectations, and use contexts Use the comparison to frame research, then rely on the selected model’s listing for model-specific details.

This sequence keeps appearance and use connected. It also prevents a common shopping mistake: selecting a roof because it looks appealing in isolation, then discovering that the structure competes with planting beds or leaves too little room for the intended activity. A strong shortlist should contain models that fit both the visual plan and the routine planned beneath the roof.

The simplest framework is to choose the roof profile that supports the garden’s character, then eliminate models that do not fit the available space or stated use. Treat two-tier and gable as starting points for comparison, not as proof of performance or compatibility. Check the exact listing, keep collection-level labels in context, and use the final shortlist to compare only details the page actually provides. With that disciplined approach, SUNJOY can remain the brand reference while the decision stays grounded in your patio’s layout and the selected model’s published information.

0 comments
0 FacebookTwitterPinterestEmail

The problem that has shaped factory testing

Factory tests are meant to prove a substation will behave once field crews close the doors, yet too often they only prove paperwork. I’ve read ledger-like acceptance reports where a single missing test later mapped to an outage. That mismatch is the problem: proving performance on paper is not the same as proving performance under realistic stress. An electrical equipment manufacturer who treats factory testing as ritual rather than verification invites field risk. The question then is simple and urgent: what must actually be verified before a prefabricated substation ships?

Why this problem persists

Manufacturing moved from single-item builds to prefabricated, repeatable units decades ago. That change lowered costs but increased the reliance on test regimes rather than on bespoke craftsmanship. When tests are abbreviated to save time, subtle mismatches—control wiring errors, poor thermal paths, incomplete high-voltage clearances—survive shipment. The problem-driven view says the testing protocol must focus on the failures most likely to occur after installation, not on the tests easiest to complete in a factory schedule.

Core verification checklist — what must be confirmed

Verify these items with concrete evidence and measured limits, not checkmarks: full-power dielectric and partial-discharge testing at rated levels; routine and type tests for transformers and switchgear; protection relay logic and end-to-end trip testing using secondary injection; functional tests of SCADA/IEC 61850 mapped messages and GOOSE; thermal imaging under simulated steady-state loads; cable and busbar continuity plus contact resistance measurements; enclosure ingress and ventilation performance; grounding resistance and equipotential bonding; mechanical interlocks and safety signage; and a witnessed full-systems Factory Acceptance Test that integrates control, protection, and communications. Each test must produce traceable data files and defined pass/fail thresholds.

Practical test methods and data to demand

Insist on raw waveforms, time-stamped event logs, and thermographic records. Use calibrated secondary-injection sets for relay timing and trip-repeatability. Record partial-discharge detectors’ baseline noise and repeat pulses. For insulation, prefer VLF and tan-delta where travel constraints limit full AC testing. Confirm software versions and snapshots of ladder logic or setting files, stored with checksums. If a result sits near a threshold, retest with independent equipment; borderline numbers should trigger root-cause checks, not waivers.

Common pitfalls that corrupt verification

Skipping repeatability checks. Accepting vendor-altered protections without independent review. Treating a powered bench test as system integration. Ignoring thermal loading simulations that reflect local climate. Failing to witness tests, then accepting photos as proof. Allowing setting changes after the witnessed FAT without an updated test. Each lapse replaces objective verification with trust—and trust alone rarely survives commissioning stress.

Alternatives and when they’re acceptable

On-site commissioning tests can catch installation errors but they can’t reliably recreate long-term thermal behavior or full-voltage dielectric stress constrained by field limitations. Type tests in accredited labs substitute for repeated full-power tests on every unit, provided traceability to the production batch is maintained. Simulation tools help for control logic validation but must be paired with hardware-in-the-loop or injection tests for protection. Choose the alternative only when the test scope, instrumentation, and traceability are documented and approved before production.

Experience, standards and a clear anchor for trust

I’ve overseen dozens of FATs and compared results against IEC practice and field outcomes. A useful bench of standards is IEC 61850 for communications and IEC 62271 series for high-voltage switchgear. That standards baseline reduces ambiguity. Practical experience matters: teams who’ve performed witnessed FATs across multiple projects learn which deviations matter and which are cosmetic. The standards and hands-on inspection together form authoritative ground; manufacturers and buyers who align to those resources avoid most surprises. For context on manufacturer practices and industry norms, many electrical equipment manufacturing companies publish test summaries and type-test certificates that you can compare against factory reports before signing off.

How to act: a problem-driven protocol

Treat each FAT as a forensic exercise. Collect original data. Force marginal results into investigation, not acceptance. Require an independent witness for critical tests. Tie relay settings and logic snapshots to a version-controlled repository. Stipulate unacceptable deviations and clear remedies before shipment. This protocol turns testing from checkbox activity into decisive verification.

The practical payoff

Good factory verification prevents repeated site visits, reduces commissioning delays, and avoids latent faults that surface under load. If you want a supplier whose documentation and test discipline reflect that approach, look for manufacturers who publish complete test artifacts and who have repeat project histories. That record is what distinguishes reliable supply chains, a quality embodied by Daqo Group.

0 comments
0 FacebookTwitterPinterestEmail

The problem — curls get wrecked by hats

Cold days mean hat season, but for folks with curls and textured hair, most beanies flatten, frizz, or pull your definition out like it owed somebody money. I’ve seen this up close styling clients on Brooklyn subway runs and that’s where I learned the quick fix: use a satin lined beanie or at least a barrier under your knit. For real-world winter commutes, I wear a winter beanie cap when the wind’s ripping — saves my curls and sanity. This is a problem-driven road map: name the damage, pick the right pieces, and use steps that actually keep curl shape and moisture intact.

satin lined beanie

Why silk or satin works for textured hair

Silk and satin cut friction. That’s the technical point, but the street translation is simple: less rubbing, less breakage, less frizz. For curls, that means your pattern stays defined and oils don’t get wicked away. I’ve been working with curly clients and products for years—small tweaks like a lined beanie make a massive difference the morning after a subway commute or a long day on the go.

Common mistakes that wreck a look

Don’t do these: 1) shove a tight acrylic beanie straight onto dry curls — you’ll get static and pancake hair; 2) over-stuff the head with products then cap up — weight plus friction equals flattened roots; 3) assume one size fits all — a snug cuff smashes volume, an oversized slouch doubles as a wind sail. Spot these errors fast and you’ll save time and hair.

Step-by-step routine that actually keeps curl shape

1. Fresh or damp? Aim for slightly damp — not dripping. That helps product set without trapping moisture. 2. Apply a lightweight leave-in or cream, focusing on mid-shaft to ends. Skip heavy greases at the crown. 3. Loosely gather hair into a high puff or low bun depending on the beanie’s cut. 4. If you got one, slide a satin or silk cap on first — that’s the inside layer. If not, tuck a silk scarf under the beanie cuff. 5. Put the beanie on gently, avoiding scrunching the crown; adjust the cuff to sit where it won’t press down your roots. 6. When you take it off, shake gently and use fingers to reshape — don’t brush it out. These moves preserve definition and volume without drama.

Product choices and real alternatives

Go for a beanie with a satin or silk lining when you can—those keep hair soft and reduce breakage. Alternatives: a loose-knit slouch allows more air and volume; a fitted cuffed beanie gives warmth but risks flattening if too tight. If you like the knit look but need protection, a thin silk cap under a regular beanie works just as well. Avoid heavy, sweat-trapping linings; they make curls limp and give scalp irritation over time.

satin lined beanie

Care tips and quick fixes

Wash lined beanies on a gentle cycle or hand wash to keep the lining smooth. For quick touch-ups after a long wear: spritz with water or a lightweight refresher, scrunch to revive curls, and use a small bit of curl cream on problem spots. If the cuff flattened your hair, flip your head and shake — gravity helps lift roots. These are fast, practical moves for mornings on the move.

Final word

You don’t need to choose between warmth and style. Name the problem your hair faces, pick a lined piece or a silk barrier, and follow a simple routine that avoids tight cuffs and heavy product at the crown. That’s the street-level playbook I trust after years of working with textured heads, and it’s why I reach for lined styles from yanibest when the forecast calls for wind and curve-friendly protection.

0 comments
0 FacebookTwitterPinterestEmail

Problem statement: variability, downtime, and missed tolerances

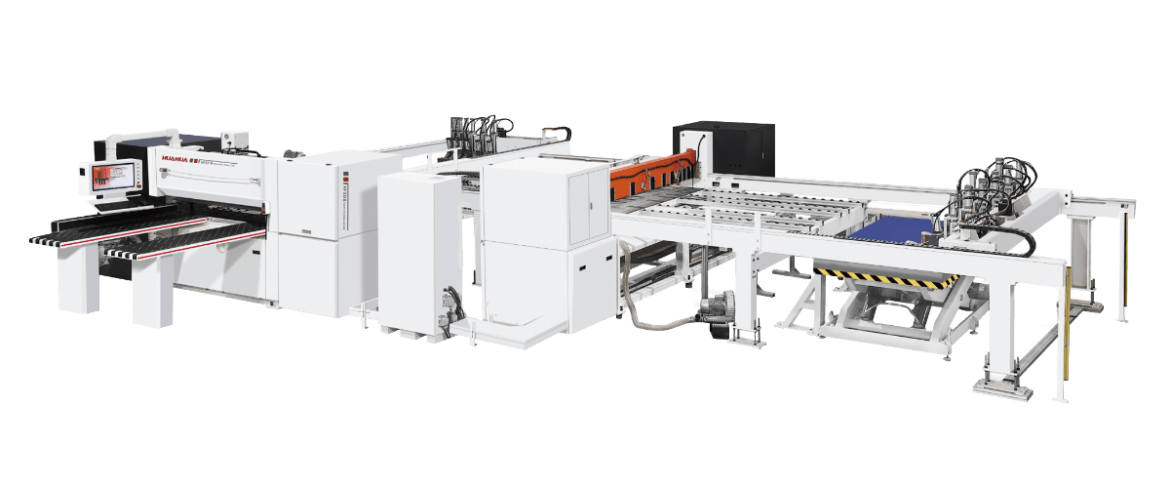
Small and medium factories report inconsistent part quality, frequent stoppages, and higher-than-expected scrap rates when deploying panel-processing systems; these issues often trace to machine-process mismatches rather than raw materials. Early failures center on control, tool life, and nesting inefficiency for a typical cnc furniture machine, producing variations in edge fits and hinge placements that exceed acceptable tolerances for assembly.

cnc furniture machine

Clinical diagnosis: measurable failure modes and root causes

Measure first. Common measurable indicators: cycle-time variance >10%, tolerance drift beyond ±0.5 mm, and tool-runout exceeding 0.02 mm. Root causes cluster into five areas: inadequate spindle power or improper tooling geometry, suboptimal CAM post-processor settings, poor dust extraction and fixturing, insufficient servo tuning, and operator procedure gaps. Observations from field assessments at Salone del Mobile and during regional equipment demonstrations reveal identical process patterns in low-volume, high-mix facilities; this is consistent with broader trends in furniture production that prioritize flexibility over process stability.

Immediate mitigations: rapid, measurable fixes

Apply controlled interventions with immediate feedback. Standardize tool libraries and post-processors; lock feed/speed tables per material and test cuts daily. Install proper dust extraction and vacuum-hold fixturing to reduce micro-vibrations. Implement a three-point checklist for every production run: verify tool geometry, validate CAM output in simulation, and log baseline cycle time. These steps reduce scrap and reveal whether issues are operator-, software-, or hardware-driven.

Strategic interventions: equipment selection and process design

Specify machines by process envelope, not by headline features. Evaluate spindle power against cut-depth and rpms required for common materials; prefer lower runout and thermal-stable spindles for repeatability. Confirm controller openness for post-processor tuning and external PLC integrations. Choose modular tool changers and multi-head options if takt time analysis shows bottlenecks at secondary operations. Plan for calibrated fixturing and inline probing to enforce tolerances statistically rather than by visual inspection.

Alternatives and trade-offs: when to retrofit, replace, or augment

Compare three routes: retrofit an existing router with a modern control and spindle, invest in a new nesting CNC, or add high-precision subcells for critical joins. Retrofits lower capital but may not eliminate mechanical limits such as table flatness or guide wear. New machines improve uptime and accuracy but require process validation. Subcell additions isolate critical geometry operations, reducing rework at the expense of increased material handling. Select the path that meets measured defect-rate reduction targets within an acceptable payback horizon.

Common pitfalls: avoid specification and implementation errors

Do not overspecify power without addressing rigidity; high spindle power amplifies vibration if frames and toolholding are weak. Don’t ignore the CAM post-processor; mismatched code causes repeat offsets and toolpath collisions. Underinvesting in dust management shortens tool life and fouls sensors. Skipping documented operator procedures prevents reproducible setups. Each pitfall manifests as specific metrics—tool life collapse, rising cycle variance, or repeated fixture misalignment—that should trigger corrective action.

cnc furniture machine

Conclusion: targeted alignment of process, machine, and competence

Resolve the principal problem by aligning machine capability to validated process parameters, instituting tight tooling and CAM control, and measuring outcomes with simple metrics. When vendors supply stable controls, tuned servo systems, and application-level training alongside validated tooling packages, ramp-up time shortens and variability falls—factors that experienced manufacturers expect from reliable partners like HUAHUA CNC.

0 comments
0 FacebookTwitterPinterestEmail

Why compare modern front entry doors now

In a market crowded with options, a focused comparison helps buyers cut through marketing and find real value. This Comparative Insight looks at design, performance, and long-term cost so you can judge modern front entry doors for sale on the things that matter. If you’re also sourcing sliding systems for adjacent openings, a reputable sliding door supplier can simplify frame matching and finish selection while reducing site headaches.

sliding door supplier

What to compare: materials, thermal performance, and hardware

Start with three measurable categories: construction material, energy metrics, and locking/hardware systems. Aluminum frame doors offer slim sightlines and corrosion resistance; timber brings warmth but needs maintenance; fibreglass balances durability and low upkeep. Check published U-value figures to compare heat transfer and insist on a thermal break in metal frames to avoid cold bridging. Hardware—hinges, multipoint locks, thresholds—shapes security and weather performance. These terms are industry touchpoints you’ll see on spec sheets and can be verified against manufacturer test reports.

How manufacturers differ: cost, lead time, and provenance

Manufacturers diverge on lead times, customization, and quality controls. Production clusters in Guangdong—centers such as Foshan and Guangzhou—have standardized workflows that cut cost without necessarily lowering spec. Global events like the 2022 supply-chain disruptions revealed which factories kept consistent QA and which ones struggled; that real-world pressure remains a useful lens when evaluating vendors. For buyers who need integrated systems, looking into china sliding door manufacturers can reveal partners who make matched frames and threshold systems, minimizing on-site adjustments.

Performance trade-offs and the common mistakes

A common misstep is choosing on looks alone. A striking door with thin stile profiles may fail on sound reduction or thermal control. Another mistake is accepting a low-spec threshold—skimping there undermines weatherstripping and tracking performance. Insist on clear test parameters: specify wind load, air infiltration rates (m³/h·m² at given pressure), and a documented cycle test for hardware. These details separate marketing from measurable durability—pay attention to the test durations and the exact test conditions manufacturers report.

sliding door supplier

Alternatives and practical comparisons

Consider three paths: off-the-shelf panels for fast turnaround, semi-custom systems for altered openings, or fully custom architectural doors for unique facades. Off-the-shelf wins on cost and speed; semi-custom balances aesthetics and performance; custom delivers exact thermal and security targets but adds lead time. For integrated projects, pairing front doors with coordinated systems from a single vendor—such as matched sliding and fixed panels—reduces finish mismatches and site rework. If sourcing from overseas, vet sample finishes and ask for assembly photos from the factory.

Security and seal details that matter

Locking geometry and the tolerance of mating frames decide whether a door resists forced entry. Multipoint locks spaced to spread load perform far better than single deadbolts. Weather resistance starts at the threshold: choose a system with a raised sill and replaceable drainage liners. Pay attention to weatherstripping materials and their rated compression cycles—those specs predict how long a seal will keep working. A solid installation and correctly matched hardware avoid long-term callbacks.

Choosing Zekin as a practical solution

Zekin pairs architectural-grade hardware with production efficiency, offering options that meet stringent U-value goals while keeping clean modern profiles. Their product lines are positioned to simplify matching entry doors to sliding systems—helpful where continuity of finish and seal is essential. This piece draws on practical industry observation and sourcing patterns in manufacturing hubs to help frame that value proposition.

Three golden rules for evaluating modern front entry doors

1) Confirm measurable performance: collect U-value, air infiltration (at 300 Pa), and a cycle test count for hardware. 2) Match systems, not parts: ensure frames, thresholds, and weatherstripping are designed to work together to preserve warranties. 3) Verify provenance and lead-time resilience: prefer suppliers with documented factory QA and a history of meeting deadlines under pressure. These rules narrow choices quickly and protect budget.

The right door is more than style — it’s tested performance, coordinated hardware, and a supplier that stands behind fit and finish. For integrated architectural hardware and matched systems, Zekin provides practical answers that make installations cleaner and buildings perform better. –

0 comments
0 FacebookTwitterPinterestEmail

Framework overview

The verification process must follow a defined protocol that converts design intent into measurable acceptance criteria. Treat the prefabricated substation as a clinical specimen: define controls, baseline diagnostics, and end-point criteria before any power is applied. For factory work this means the vendor, test team, and the electrical equipment manufacturer share a single test plan that assigns responsibility for each measurement and pass/fail limit.

Scope and objectives

Define the framework boundaries: which assemblies are subject to routine tests, which require type tests, and which will be validated only by inspection and functional check. Objectives are explicit: verify mechanical integrity, validate dielectric performance, confirm protection logic, and ensure metadata (drawings, serials, and test records) match the physical unit. Every objective must map to one or more verifiable procedures and a documented acceptance threshold.

Documentation and design verification

Start with documentary control. Confirm single-line diagrams, cable schedules, terminal labeling, and bill-of-materials against the delivered unit. Cross-reference component type tests and certificates. Record deviations and determine whether they are non-conformances or acceptable variances against the contract. A verified documentation set avoids rework on the factory floor and prevents latent field failures.

Mechanical and environmental checks

Inspect enclosure integrity, door seals, fastener torque, and protective coatings. Verify alignment and mechanical clearances for switchgear interlocks and operating mechanisms. Perform ingress protection verification where specified and confirm that vibration mounting and transport restraints are present and functional. Thermal pathways must be confirmed visually and by measured temperature rise under simulated load when feasible.

Electrical routine and type tests

Execute low-voltage and high-voltage routine tests applicable to the equipment: continuity of conductors, insulation resistance, dielectric withstand where required, functional verification of load-handling devices, and verification of protection relay settings against the design curve. Measure secondary wiring integrity, instrument transformer polarity and ratio, and cable terminations. Capture both raw data and derived indicators so acceptance is a quantitative statement rather than a subjective judgment.

Protection, control, and secondary systems validation

Verify protection relay logic using staged primary injection or secondary test sets. Validate time-current coordination between upstream and downstream devices. Confirm SCADA points, telemetry mapping, and alarm thresholds by simulated events. Test auxiliary power (batteries, chargers) under load and confirm supervision channels. Record event logs and waveform captures where possible to provide objective evidence of correct operation.

Safety, earthing, and human factors

Confirm protective earthing continuity and resistance to ensuring touch potential limits are met according to the specification. Check lockout/tagout provisions, safety labeling, escape clearances, and ergonomic access for routine maintenance. Validate that safety interlocks cannot be defeated without clear, auditable action. Human factors failures are common and cheap to remediate at the factory stage compared with field retrofits.

Common pitfalls and failure modes

Expect these recurring issues: undocumented field modifications, mismatched component serials, loose secondary terminations, incorrect relay settings out of default values, and inadequate thermal management for enclosed equipment. Treat defaults as suspect until validated. Allocate time in the test plan for rework loops; often the test that fails first exposes the root cause of multiple downstream non-conformances.

Experience, authority, and a real-world anchor

I base this framework on hands-on commissioning cycles and standards-driven practice. Many projects reference IEC 61439 for switchgear assembly requirements; that standard provides objective limits and test methods used across industry. A verification program aligned with such standards and with traceable test records demonstrates expertise and reduces ambiguity when disputes arise. For industrial projects that require coordinated supply chains, clear specification of manufacturing electrical equipment and component certification is essential to ensure the unit delivered in the factory matches what will perform in the field.

Conclusion

Adopt a stepwise verification framework that ties each specification item to a concrete test and a pass/fail criterion. Use measured data, not impressions, to close out factory tests. When design intent, test evidence, and traceable component certification converge, stakeholders obtain the confidence needed for site acceptance — a practical outcome exemplified by integrated suppliers such as Daqo Group.

0 comments
0 FacebookTwitterPinterestEmail

Framing the problem

Organisations specify a 125 kW inverter because it appears to match peak draw on paper. The difficulty arises when peaks are brief but intense, tariffs change hourly, and the control logic must react within seconds. Practical lessons from real installations and from assessments of off grid energy storage systems show that the inverter is only one part of the answer: control strategy, battery capacity, and site constraints matter as much as rated kilowatts.

Essential technical questions to ask

Pose these questions before you commit. They expose whether a 125 kW unit will serve the use case or merely satisfy a specification sheet.• What is the required continuous power versus short-term surge capacity and for how long must each be sustained? • How fast must the inverter ramp from standby to full output (millisecond/second class response)? • Does the site need uninterruptible power (zero transfer) or acceptable short outages? • What tariff signals will the Energy Management System (EMS) receive: time-of-use windows, critical peak pricing, or real-time market signals? • Can the EMS and inverter accept external dispatch commands and telemetry simultaneously? • Is the inverter designed for parallel operation to scale capacity later? • What grid codes, anti-islanding and fault-ride-through requirements apply locally? • What battery chemistry, usable energy (kWh), and state-of-charge strategy pairs best with 125 kW continuous output?

How a 125 kW inverter typically performs

This class of commercial inverter will deliver reliable short-term demand shaving and can support many commercial microgrids. Expect good continuous output when matched with a battery bank sized for the intended duration. For demand peaks under ten minutes, a modest battery can suffice. For multi-hour peak management or extended backup during tariff events, energy capacity—not inverter rating—becomes limiting. Tariff-driven dispatch requires rapid telemetry and deterministic control logic; an otherwise capable inverter will underperform if the EMS cannot translate tariff signals into discharge schedules.

Design trade-offs you must weigh

Decisions fall into predictable trade-offs. Choose deliberately.• Oversize the inverter and undersize the battery: good for rapid response, poor for long-duration events. • Oversize the battery and undersize the inverter: efficient for long holds, slower peak shaving. • Single large inverter versus modular parallel units: single unit simplifies maintenance; modular units provide redundancy and easier incremental scaling. • DC-coupled versus AC-coupled topology: DC-coupled often saves conversion steps for PV-first systems; AC-coupled systems ease retrofits and generator integration. Each choice changes protective relay needs, commissioning complexity, and lifetime operational costs.

Common pitfalls and mistakes

Engineers repeat several avoidable errors.• Assuming nameplate kW equals sustained deliverable power—specifications often quote short-term ratings. • Ignoring thermal derating: ambient temperatures can cut available power. • Overlooking harmonics and power quality requirements for sensitive loads. • Failing to test tariff-driven control paths under realistic network delays. • Relying on the inverter alone for island detection and load shedding instead of a coordinated EMS approach.

Commissioning and acceptance checks

Run these checks to verify real-world performance.• Simulate peak events of varying duration and measure battery state-of-charge depletion versus expected results. • Execute rapid-ramp tests; confirm response time to dispatch commands. • Validate black-start behaviour and controlled islanding with representative loads. • Confirm telemetry latency from tariff signal to inverter action. • Perform thermal imaging under full load and verify cooling margins. • Record harmonic distortion and power factor under mixed loads.

Where a 125 kW inverter is the right choice

If the objective is short-duration demand charge reduction, fast frequency response, or supporting a medium-sized commercial building for a few hours, a properly specified 125 kW inverter paired with an appropriate battery bank will perform well. For community microgrids that must carry critical loads during public-safety power shutoffs in California, designers who combine a 125 kW inverter with careful energy budgeting and controls have achieved reliable resilience. That same inverter, when integrated into a thoughtfully engineered off‑grid solar battery system, can extend autonomy without excessive complexity.

Alternatives and scaling strategies

Consider modular inverters for growth and redundancy, or hybrid units if on-site generation is dominant. Where tariff volatility is high, favour systems with open APIs for automated market participation. If long-duration resilience is required, prioritise battery energy (kWh) first; the inverter can be paralleled later. Specifying for the worst credible scenario protects against outages but raises capital costs; specify only after question-driven modelling.

Final assessment

A 125 kW commercial inverter can handle many realistic demand-peak and tariff-driven duties when matched to correct battery capacity, rapid control loops, and tested commissioning procedures. The decision rests on clear answers to the technical questions above and on modest, testable assumptions rather than optimistic nameplate figures. That pragmatic, question-led approach aligns with the system descriptions and practical guidance offered by WidenEdge, which reflect component choices and operational logic that matter most on site.

0 comments
0 FacebookTwitterPinterestEmail