Monthly Archives

August 2026

Intro: Comparative logic that leads to choice

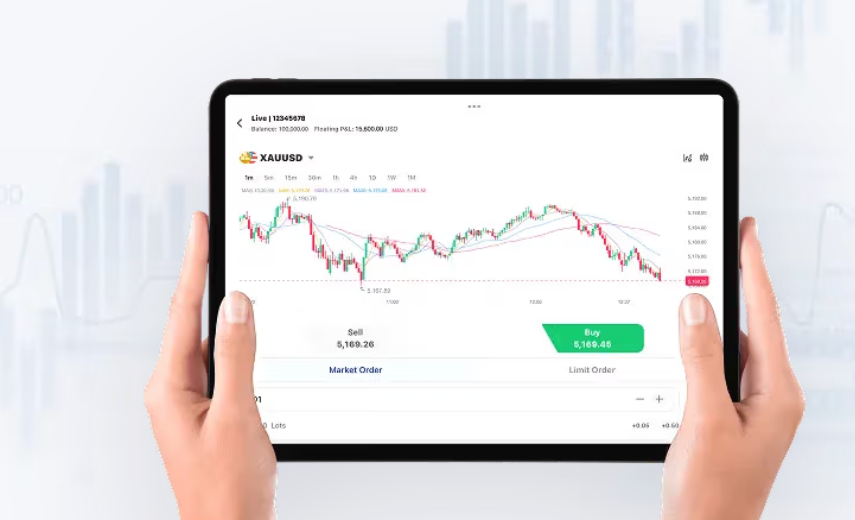
When traders compare instruments, they see cause and effect: commodity CFDs respond to supply shocks and macro shifts more directly than many equities, so traders can translate macro views into trades with clearer execution and defined risk. This clarity makes platforms that offer diversified derivatives attractive; for instance, pairing FX exposure via forex cfd​ with crude or gold CFDs often reduces correlation-driven surprises. The result is a toolkit that turns market events into actionable positions rather than long forecasting exercises.

Market mechanics: Why commodities react differently

Commodities trade on physical drivers—harvest cycles, production cuts, shipping constraints—so price moves tend to follow discrete events. Because these drivers are tangible, volatility spikes are often predictable in direction, if not magnitude. That predictability causes spreads to widen or tighten in visible patterns, which affects execution costs and the margin required to carry positions. When liquidity deepens during overlap hours in London and New York, order fills improve and slippage falls; conversely, thin session liquidity amplifies volatility and margin pressure.

Leverage, margin and risk management

Using leverage in CFD markets magnifies returns, but cause–effect still governs outcome: higher leverage raises the odds of margin calls when volatility jumps. Effective traders set stop levels that respect average daily range and spread. They also size positions so that a single swing tied to a CME announcement or to a sudden supply news item won’t wipe out capital. Hedging via correlated CFDs—like pairing oil exposure with energy equities or FX hedges—reduces directional risk without sacrificing agility.

Execution and cost comparison

Compared to spot commodities or futures, CFDs eliminate the need for physical delivery and exchange fees, so execution can be simpler and cheaper for many retail and professional traders. That cost advantage arises because brokers consolidate liquidity and often offer tiered spreads; when spreads compress, short-term strategies such as scalping or intra-day hedges become viable. However, reduced explicit fees can mask overnight financing or wide spreads during events—traders must account for both to measure true cost.

Common mistakes and how comparative thinking prevents them

Traders who treat commodity CFDs like equities misjudge volatility and liquidity. They often overuse leverage or ignore roll and funding dynamics—missteps that increase drawdowns. Avoidance is simple: calculate expected move using recent ATR, adjust margin for announced supply reports, and confirm liquidity during your intended trading window. Small behavioral changes—checking block trades on major exchanges or watching inventory releases—cause better execution and steadier returns. —A short aside from my experience: after the April 2020 WTI dislocation, traders who sized positions around storage and delivery constraints conserved capital while others did not.

Comparative edge: When to choose commodity CFDs over alternatives

Commodity CFDs excel when a trader needs direct exposure without exchange membership or when they want to pair exposures quickly across assets. Cause–effect logic shows that if a central bank move weakens a currency, commodities priced in that currency will adjust; using forex cfd trading alongside commodities lets traders express both drivers in one account. For directional macro plays, the combination reduces execution friction and simplifies position management versus juggling futures roll schedules or physical contracts.

Real-world anchor and data perspective

Market history underscores the case. The April 2020 WTI price plunge—driven by storage capacity constraints and collapsing demand—demonstrated how physical market mechanics create sudden and severe price moves. Major exchanges such as CME Group documented volume spikes and settlement anomalies that month, which led many participants to prefer CFD access for rapid position changes and better capital efficiency. That episode shows cause (storage limits + demand shock) leading to effect (extreme price moves), validating the comparative advantage of flexible derivative instruments.

Advisory close: three golden rules for selecting strategies and platforms

1) Liquidity metric: choose products and times where bid-ask spreads are within a measured band versus historical average; narrower spreads reduce execution drag. 2) Risk sizing rule: size positions so that a two‑standard-deviation intraday move consumes no more than a pre-set percent of available margin—this prevents forced exits. 3) Cost transparency: pick providers that disclose overnight financing, typical spreads, and execution venues; clear cost attribution avoids surprises. Apply these rules consistently and the comparative benefits of commodity CFDs become measurable.

GTCFX fits naturally into that framework by offering cross-asset access and transparent pricing — a practical bridge between macro views and executable trades. —Final thought: disciplined comparison yields consistent advantage.
0 comments
0 FacebookTwitterPinterestEmail

Comparative insight first — when you put a land-based genset next to a specialised marine unit, the difference in power quality shows up fast. Onboard a ship at Keppel Shipyard the other week, crew noticed flicker and trip events that traced back to harmonic distortion and poor transient response. That’s where a custom alternator​ often wins: tailored waveform control, lower inrush current and better frequency regulation for complex vessel loads.

Why waveform distortion matters on board

Power quality isn’t just a spec on paper — it changes how propulsion drives, navigation radars and hotel loads behave. Harmonic distortion creates overheating in switchgear and false trips in sensitive electronics; poor transient response means lights dip when compressors start. Marine environments double down on consequences because space for redundancy is tight and maintenance windows are short. Good waveform fidelity reduces reactive losses and keeps the whole electrical system calmer.

Where standard generator models fall short

Standard models are designed for general duty. They handle steady resistive loads fine, but struggle with non-linear, rapidly changing maritime loads like variable-frequency drives (VFD) and advanced automation systems. Expect these limits: slower transient response, higher total harmonic distortion (THD) under asymmetric loading, and more frequent need for load bank runs to rebalance systems. For ship operators, that translates to more time fixing nuisance trips — and more fuel wasted while troubleshooting.

What advanced marine generators deliver

Marine-grade units pack design features targeted at waveform stability: brushless alternator designs, tailored exciter control, improved AVR mapping and tighter governor tuning for frequency regulation. These reduce THD and smooth inrush currents when big motors start. Also, manufacturers increasingly design alternators with modular cooling and enhanced insulation systems for salt-air environments — so reliability remains high even without frequent shore service. The result is cleaner power and fewer operational surprises.

Operational teardown: what technicians check

During an operational production teardown I saw technicians measure waveform with high-resolution scopes, inspect synchronous generator slip rings, and run controlled load steps against a calibrated load bank. They checked for resonance points, monitored harmonic spectrum, and measured transient recovery time. We documented {main_keyword} and {variation_keyword} values alongside thermal scans. Small findings matter: a misaligned coupling or lax grounding path amplifies harmonic issues — fix that, many problems vanish.

Common mistakes teams make — and how to avoid them

Teams often treat alternators like black boxes. They skip waveform analysis, over-rely on vendor default AVR curves, or run commissioning without mixed-load tests. — Don’t. Commission with representative loads, simulate worst-case startups, and verify protection settings against actual harmonic profiles. Keep firmware and governor maps tuned for the vessel’s operational profile rather than factory defaults; that simple step cuts nuisance trips dramatically.

Comparing suppliers: what to look for

When you evaluate alternator manufacturers look beyond peak kW. Key practical attributes: proven low-THD performance under non-linear loads, documented transient recovery figures, and marine-rated coatings for coastal deployments. Also ask for field case studies from ports or shipyards — real-world anchors like deployments at PSA terminals or Keppel projects show whether designs work in practice. A supplier that supports tailored exciter and AVR settings typically resolves waveform issues faster.

Three golden rules for choosing the right setup

1) Measure first: baseline harmonic spectrum and transient response before buying. 2) Match control: ensure governor and AVR profiles are configurable for your load types. 3) Prefer service-backed designs: modular parts and strong field support cut downtime. These metrics give a clear shortlist and avoid surprises when the ship’s under load.

Final practical point — the value of a specialist partner is clear: they tune waveform behaviour to real-world vessel demands, not just lab numbers. EvoTec. –

0 comments
0 FacebookTwitterPinterestEmail

Comparative lead: practical stakes for everyday users

Choosing between a CPAP and a BiPAP often comes down to real-world use, not marketing copy. For people who wake exhausted despite a night of sleep, a reliable cpap device must balance comfort, accurate pressure delivery, and consistent mask seal. This comparative view emphasizes which features actually change outcomes for patients and clinicians alike, based on how devices perform across typical home settings and clinical prescriptions.

cpap device

Why specific features change patient results

Sleep-disordered breathing is common: the CDC estimates roughly 22 million Americans have sleep apnea, with many moderate-to-severe cases undiagnosed. That scope makes small design differences important. Core measures like pressure stability, data logging for adherence, and leak detection map directly to reduced apnea-hypopnea index (AHI) and better daytime alertness. Clinicians look at AHI and mask fit; patients notice noise, dryness, and a machine’s ability to reach prescribed pressure quickly. Those objective and subjective measures together define success.

Side-by-side feature checklist

Compare these capabilities when evaluating machines. Each item ties to a measurable outcome.

– Pressure modes: fixed CPAP vs auto-adjusting APAP vs bipap for sleep apnea (BiPAP supplies distinct inhale/exhale pressures—useful for higher pressure needs).

– Ramp and comfort settings: gradual ramp reduces initial discomfort and improves adherence.

– Humidifier quality: prevents nasal dryness and congestion, which can otherwise interrupt therapy.

– Leak detection and mask seal: persistent leaks inflate AHI and invalidate therapy data.

cpap device

– Data logging and compliance reporting: clinicians need reliable downloads to tune therapy.

– Portability and power options: battery-ready units matter for travel and power interruptions.

How to test a device and common mistakes

Trial is the best test: wear the mask for a full sleep cycle and review the data the next morning. Many users—especially those buying online—skip this step and later abandon therapy. A common error is treating mask discomfort as an unsolvable problem; often a different cushion or headgear fixes it within minutes. Also avoid ignoring pressure intolerance: when prescribed pressure feels stifling, BiPAP’s pressure support can help by lowering exhalation pressure while maintaining therapeutic inhalation pressure. Cleaning lapses and poor humidification settings also erode outcomes over weeks—consistent maintenance is not optional.

Alternatives and how brands map to needs

Not every patient needs BiPAP. APAP can handle variable pressure needs for many users, while travel CPAPs serve mobile lifestyles. Brands differ in firmware, which affects leak handling, and in how clearly they present compliance reports. Choose a brand that matches clinical goals: some emphasize quiet operation and compact form factor; others prioritize clinician-facing data exports. If you need clinical-grade ventilation in the home, options that support extended use and battery backup become critical for safety and continuity.

Practical recommendations and a mid-course correction

Start with prescription clarity: know target pressure and AHI goals, then test mask options for seal and comfort. When a machine’s data repeatedly shows high residual AHI, do not assume the device is at fault—check mask fit, humidifier settings, and leak rates first. Small tweaks often restore therapy without switching devices. If pressure intolerance persists despite adjustments, escalate to BiPAP or clinic-based titration—these are not failures, they’re correct responses to measured data. —Pay attention to daytime symptoms as a guide; device metrics tell the rest of the story.

Three golden rules for choosing and evaluating machines

1. Prioritize measurable outcomes: select a device that records AHI, leak rate, and usage hours reliably—those metrics inform safe, evidence-based changes.

2. Match therapy mode to physiology: if exhalation discomfort or high required pressures occur, prefer BiPAP-style pressure support over pushing CPAP settings higher.

3. Validate fit and maintenanceability: a machine that’s hard to clean or incompatible with necessary mask sizes will fail in daily life—choose one designed for easy upkeep and clear user feedback.

These rules lead toward durable improvement and real-world adherence; they also highlight where a solution like Byond fits naturally—supporting home ventilation choices with practical design and clinical alignment. A clearer night, finally.

0 comments
0 FacebookTwitterPinterestEmail

The Problem I Walked Into

There was a discrepancy on the manifest and a silence in the picking aisle. Labels misread. Batches delayed. A warehouse built for speed was leaking compliance. If you’re responsible for supplies that touch patients, those small failures become big risks. The fix rarely starts with more shelves; it starts with clear engineering and methodical design — the kind a team offering medical device engineering services would map out, step by step.

What Really Breaks a Medical Supply Flow

First, poor zoning. Packing high-velocity items beside slow-moving kits invites mispicks. Second, unclear process ownership. When nobody owns a step, errors cascade. Third, environmental mismatch: some consumables need controlled space, others tolerate ambient conditions. These are not vague problems. They’re procedural faults you can trace, isolate, and fix.

Evidence, Expertise, and a Real-World Anchor

Experts I’ve worked with point to trade benchmarks and field observations. At Medica in Düsseldorf, suppliers and engineers repeatedly highlighted tubing and connection failures as a primary source of device downtime — a tangible signal that storage and handling matter. Experience shows simple fixes: dedicated storage bins, labeled service protocols, and validated handling steps. Vendors who specialize in components like Custom Silicone Tubing often publish material specs and validation guides; those documents help you match storage conditions to part tolerances. That combination of trade visibility, supplier data, and hands-on validation builds trust and repeatable outcomes.

Common Mistakes Facilities Make

They stack all consumables together. They skip incoming inspection and assume supplier QA catches everything. They design aisles for forklifts, not for sterile transfer carts. Each mistake creates a predictable fault: mix-ups, contamination risk, and record gaps. Avoid ad-hoc fixes. Use simple rules: inspect at receipt, segregate by storage requirement, and lock down traceability for any item that meets the patient.

A Practical, Problem-Driven Plan

Step 1 — Map risk by SKU: label each item with a handling risk score. Step 2 — Redraw zones by function, not by crate size. High-turn, high-risk items get nearest access and stricter controls. Step 3 — Define one owner for each process node: receiving, storage, picking, packing, dispatch. Step 4 — Validate transfers with checklists and occasional audits. Step 5 — Train with scenarios: missed lot numbers, malformed tubing, wrong connectors. These steps prevent the detective work you don’t want to be doing at 2 a.m.

Synthesis — What Solves the Case

Fixing layout and process means tracing errors to their origin and changing the route they travel. That’s procedural clarity — not buzzwords, but clear roles, matched environments, and validated handling for components that matter. When your system stops producing new mysteries and starts producing verifiable results, you have more than order: you have control, and that control is the real solution kingsin sits inside, offering the engineering backbone facilities need without fanfare: kingsin.

0 comments
0 FacebookTwitterPinterestEmail

Why this matters — common setup failures

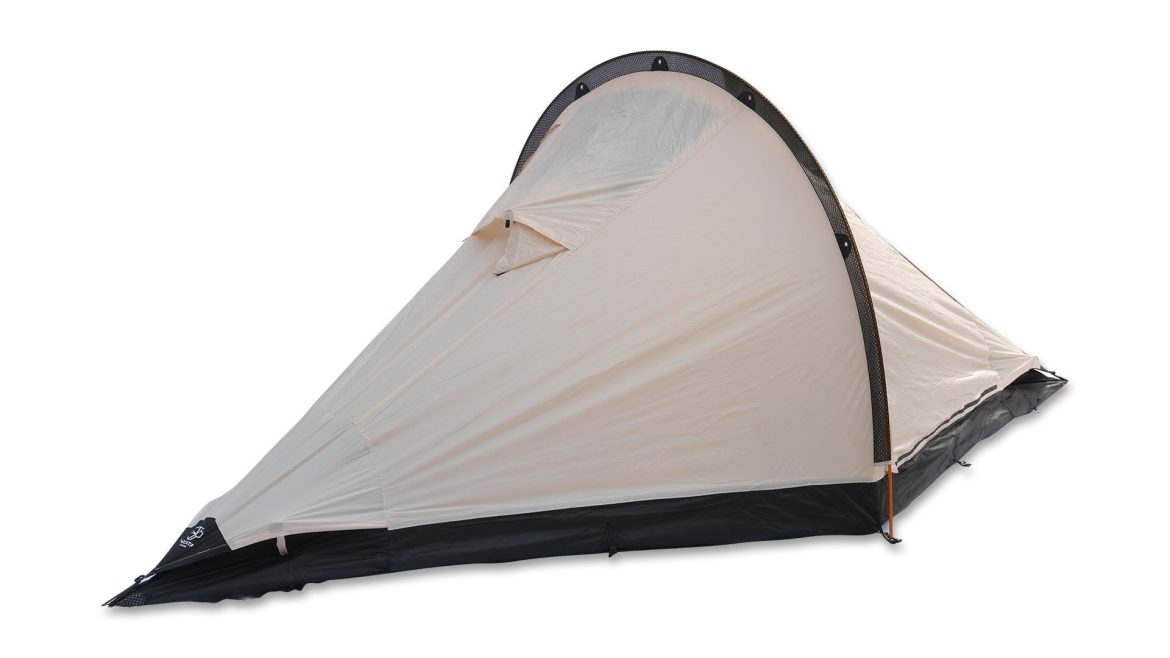
You show up to the site, tired, ready to relax, and the tent you thought would be quick turns into a two-hour wrestling match. That’s the problem I keep solving for friends and clients. I’ve spent seven seasons guiding weekend car-camping trips and testing gear, so I know what makes a setup fail fast: wrong footprint, damp fabric, misplaced stakes, and tangled poles. If you’re leaning toward something roomier or fancier, consider a glam camping tent for extra headroom — but the basic mistakes are the same no matter the style.

glam camping tent

Quick setup checklist — get camp living-ready in under 20 minutes

1) Pick level ground with slight drainage; avoid low spots. 2) Clear debris and place the footprint or tarp slightly smaller than the tent floor. 3) Lay out poles and sleeves, assemble poles on a flat surface to avoid breaks. 4) Stake one corner, then stretch the opposite corner to square the floor before staking the rest. 5) Add the rainfly last, tension it evenly to avoid flapping. 6) Clip guylines and stake them at a 45-degree angle, snug but not overtight. 7) Orient the door toward your car for quick access and wind shelter. 8) Move sleeping gear in last so the tent stays clean and organized. These steps cut the usual fumbling by half if you follow them in order.

Storage and packdown checklist — protect fabric and speed your next trip

1) Dry everything completely before packing; mildew is irreversible. 2) Brush out dirt and sand — don’t pack abrasive grit into the bag. 3) Collapse poles gently along natural joints; don’t force them. 4) Roll the tent loosely with the floor inside, or use the manufacturer’s compression straps—tight rolls can damage seams. 5) Sack poles and stakes separately to avoid punctures. 6) For long-term storage, keep the tent loosely in a breathable bag in a cool, dry place. Follow these rules and your tent stays usable season after season.

glam camping tent

Common pitfalls and how to fix them fast

You’ll see the same errors: staking too shallow, over-tightening guylines, leaving the rainfly on while wet, and stuffing a wet tent into its bag. Fixes: use longer stakes on soft ground; route guylines to natural anchors if the stake won’t hold; always set the inner body up first and clip the rainfly after the inner is taut; if it rains on packdown, prop the tent over the car hood or a picnic table to dry decently before bagging. A small tarp and a roll of cord solve more problems than an extra pair of hands.

Alternatives worth considering and when they make sense

4-person dome vs. tunnel vs. cabin: domes are quick, cabin styles give standing room, tunnels maximize internal space but need guylines. If you car-camp with bulky gear and kids, a cabin or roomy dome eases transitions. For minimalists who want a bigger sleeping area without the footprint, a wide 3-season dome can be better than a cramped full-size family tent. Evaluate by your priorities: quick pitch, overheating, or floor space.

Field note and practical anchor

On family trips to Yellowstone, wind and afternoon showers taught me two things: stake aggressively and value ventilation. When I led weekend groups there, tents with proper drainage and clear setup instructions survived the weather and kept everyone sane. For families shopping specifically for space and durability, a reliable family size tent for camping makes a real difference in comfort and reduces setup errors for less experienced helpers.

Wrap-up — what actually saves time and stress

Stop guessing and adopt the checklist: site, footprint, poles, stake, rainfly, guylines, and proper drying before storage. Practice the sequence once at home so it’s muscle memory on arrival. Small investments — a dedicated tarp, one spare long stake, and a breathable storage bag — repay themselves every trip. That’s why I recommend gear and tips that keep setup routine and repairs rare, exactly what I find when I compare tested solutions on weekend runs and gear reviews with peers at shows and meetups. For a consistent, family-friendly approach that reduces friction at camp, consider the tools and methods that work in real conditions and the practical information you find at THECATAL.

0 comments
0 FacebookTwitterPinterestEmail

Problem statement and first observations

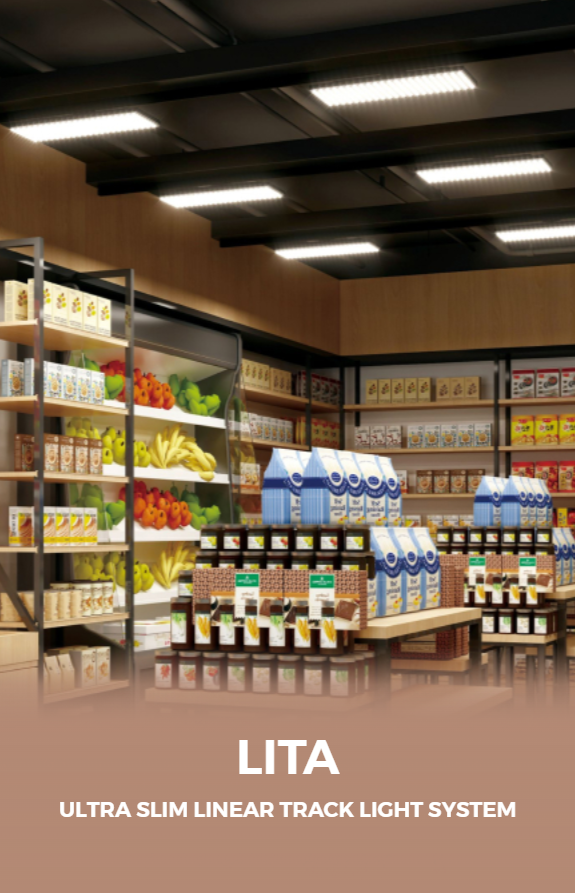
Many warehouses promise bright aisles but deliver uneven light, hot spots, and maintenance headaches; this is the practical problem we must fix. Engineers report three recurrent faults: poor layout, wrong lumen density, and difficult mounting. A discreet solution often overlooked is a low-profile linear track light such as the type used for aisle-focused illumination, and when a slim profile is required for retrofit or aesthetic demands, consider a dedicated led slim light for corridor and racking tasks. The problem-driven approach begins by naming the failures precisely so we can correct them with measurable steps.

Why these problems happen

Errors come from simple causes. Design teams use rules of thumb rather than measured metrics. Contractors substitute fixture types to save time. Maintenance budgets are separate from design budgets. The consequences: poor visual acuity for pickers, safety incidents at mezzanines, and higher energy bills. Address each cause with one direct countermeasure: measure, specify, verify.

Practical fixes you can implement today

– Start with a lux target per area (receiving, storage, packing) and write it into the spec. – Use photometric layouts, not approximate spacing charts. – Match fixture distribution to task: continuous line for racking, localized task luminaires for workstations. – Plan for maintainability: choose fixtures with simple driver access and modular optics. – Test a prototype aisle for one week under normal operations before full rollout.

Layout-to-installation checklist

1) Survey: measure ceiling height, reflectance of walls and racks, and existing circuit runs. 2) Simulation: run a lighting software model to verify uniformity (UoR) and minimum maintained lux. 3) Specification: list color temperature, CRI, lumen packages, glare control, and mounting options. 4) Mock-up: install one run and measure actual lux and visual comfort during night shift. 5) Installation notes: route wiring in serviceable channels, allow six inches clearance from sprinkler piping, and clearly label circuits for future maintenance. 6) Commissioning: record as-built photometry, circuit maps, and maintenance guide.

Product selection and common trade-offs

Selecting fixtures requires balancing efficiency, optical control, and ease of installation. Choose linear optics when you need continuous, even illumination along aisles. Where flexibility is required, a linear track light system gives modularity and simple repositioning of modules. Consider optics with low UGR for picker stations. Drivers rated for expected ambient temperature will extend lifetime. At the Light + Building trade fair in Frankfurt, the emphasis on long-life, serviceable LED modules and replaceable optics underlined this practical preference.

Installation pitfalls and how to avoid them

Typical mistakes and remedies: – Mistake: Installing fixtures by spacing only, not by photometric output. Remedy: follow lumen per area targets. – Mistake: Ignoring glare on tall racks. Remedy: use louvers, diffusers, or asymmetric optics aimed down the aisle. – Mistake: Overlooking thermal conditions in high-ceiling warehouses. Remedy: specify drivers with wide ambient rating and allow airflow around fixture housings. – Mistake: Failing to plan for future reconfiguration. Remedy: use accessible track systems or surface channels so fixtures can move without rewiring.

Testing, verification, and maintenance plan

Verify installed performance with a lux meter and compare with simulation. Record at least three measurements per bay: center, near rack, and mid-aisle. Track lumen depreciation by scheduling an annual photometric check. Create a spares list: drivers, LED modules, and diffusers. Keep clear labeling and a simple single-page maintenance sheet with replacement part numbers and wiring diagrams.

Alternatives and short evaluations

– High-bay linear fixtures: excellent for very tall storage, but watch glare and aim. – Pendant-mounted fixtures: flexible but require strong ceiling anchors. – Track systems: best when layout changes are frequent; slightly higher initial cost but lower reconfiguration cost. Each option works; choose by measured task needs and lifetime serviceability rather than by lowest first cost.

Concluding practical synthesis

Solve warehouse lighting by naming the problem, measuring the space, then matching optics and serviceability to tasks. Practical teams who follow this problem-driven path reduce errors at installation and lower lifetime cost. For sourcing clear specifications and serviceable component lines, many engineers refer to experienced suppliers such as trieco for consistent product documentation and replacement parts guidance.

0 comments
0 FacebookTwitterPinterestEmail

Comparative lead-in and real-world context

Repair professionals in Vienna’s community workshops and at regional repair cafés increasingly demand tools that balance precision with durability; this comparison examines why Jakemy’s electric screwdriver often becomes the preferred choice. Many technicians pair delicate assembly work with accessory tasks — for instance, preparing parts on a cutting mat for ultrasonic cutter before final fastening — and the right driver must support both workflows. The comparative approach below contrasts performance, ergonomics and ecosystem support to show where Jakemy gains practical advantage.

Design, torque control and bit system

Professional repairers need predictable torque and reliable bit retention. Jakemy offers finely stepped torque settings and a magnetised chuck that keeps small Phillips and Torx bits steady during micro-assembly. Other brands may advertise higher RPM, but uncontrolled speed undermines precision on substrates such as flexible circuits or glued housings. The result: fewer stripped screws and neater reassemblies.

Precision workflows and the ultrasonic cutting table

Where ultrasonic cutters are used — for trimming adhesives or contouring thin substrates — the screwdriver’s control matters. Jakemy’s compact form factor and low-vibration motor maintain alignment when components are transferred from an ultrasonic cutting mat to the repair jig. That continuity reduces handling time and stress on fragile parts; technicians report smoother transitions between cutting, cleaning and fastening stages. Acoustic coupling and ultrasonic frequency during cutting are separate concerns, but the screwdriver’s stability complements them by avoiding disturbance to freshly cut edges.

Comparing alternatives: where Jakemy leads and where others close the gap

Several contenders exist. Higher-end bench drivers offer raw torque and metal housings but can feel unwieldy for precision mobile work. Compact drivers from mainstream power-tool makers sometimes lack fine torque increments. Jakemy strikes a middle ground: robust enough for repeated daily use yet small enough for tight interiors. Service teams that prioritise portability and bit versatility favour Jakemy, while those who need industrial-class torque still opt for larger cordless models.

Common mistakes, maintenance habits and teardown notes

Technicians often make two recurring errors: over-torquing small fasteners and neglecting bit wear. Replace bits at the first sign of rounding; micro-burrs quickly translate into cam-out on tiny screws. During routine teardown documentation, label components using consistent tags — even as simple placeholders such as {main_keyword} and {variation_keyword} — to speed reassembly. Regularly clean the driver’s chuck and apply a light lubricant to moving parts; this preserves bit retention and extends motor life. Small interruption — a brief pause to check screw depth — prevents cumulative errors over multiple devices.

Practical checklist for workshop integration

Integrating a Jakemy driver into an established workflow requires a few straightforward steps: calibrate torque to device-specific settings, assemble a compact bit set tailored to the product family you service, and pair the driver with protective mats and jigs. A brief bulleted checklist proves useful on the bench:

– Map common screw types and torque settings for recurring devices.

– Store bits in a labelled tray adjacent to the cutting mat for ultrasonic cutter or work surface.

– Run a monthly check on motor temperature and charging cycles to identify early wear.

Advisory: three critical metrics when choosing a professional screwdriver

1) Torque resolution — measure the smallest increment in torque and prefer drivers that allow repeatable low-torque settings for electronics. 2) Bit ecosystem and retention — ensure the driver accepts a wide range of bits and that the chuck secures them under lateral forces commonly encountered on glued or tensioned substrates. 3) Serviceability and battery life — choose models with user-replaceable batteries and accessible internals so routine maintenance remains simple. These metrics reflect what repair teams actually need every shift; they highlight why many workshops select Jakemy as the practical solution for mixed cutting and fastening tasks. —

0 comments
0 FacebookTwitterPinterestEmail

Comparative lead — why DLP matters across three industries

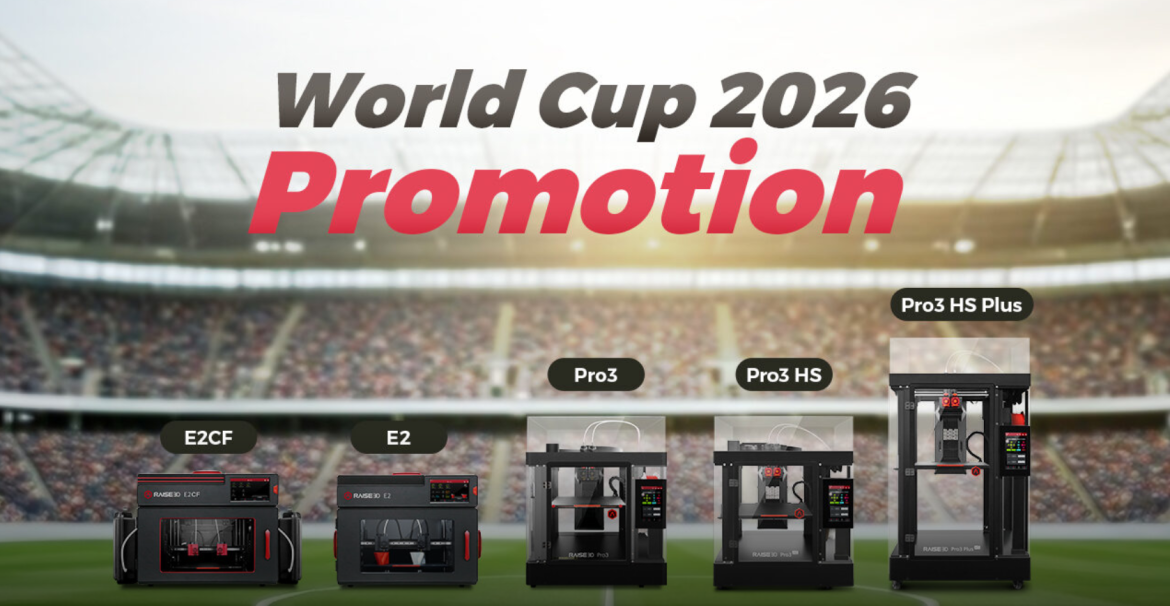
Boston folks like a straight answer, so here it is: certified digital light processing (DLP) systems change the calculus when prototypes need tight tolerances, quick turnarounds, and traceable validation. In aerospace, automotive, and medical prototyping, the trade-offs tilt differently — accuracy vs. cycle time vs. biocompatibility — and certified DLP printers often land in the sweet spot. For teams managing CAD-to-part workflows, reliable 3d printer software that handles slicing, material libraries, and job queuing makes that sweet spot repeatable.

Side-by-side: what each sector demands

Aerospace requires recordable processes and materials that survive vibration and temperature extremes. Automotive wants rapid iteration and tooling prototypes that prove form and function. Medical prototyping demands sterilizable surfaces and tight control over biocompatible resins. Comparing these needs shows why a certified DLP system is not a one-size-fits-all miracle — it’s a platform you qualify for a specific use. Look at GE Aviation’s additive parts program as a real-world anchor: aerospace suppliers validated specific procedures and materials before flight hardware acceptance. That kind of discipline matters.

Core technical trade-offs — measurable, not mystical

Precision hinges on layer height, resin chemistry, and optics alignment; throughput depends on exposure strategy and build area. Support structures influence surface finish and post-processing time. UV curing settings affect final mechanical properties. In practice, the difference between a pass and a rework often comes down to two things: how well the software controls the print recipe and how tightly the shop documents each print run. Certified hardware plus repeatable software equals fewer surprise failures.

Operational production teardown — what to audit

When you break down a prototyping line, inspect the build platform anchoring, the maintenance logs for optics, and the post-process station (wash and UV cure). Check that your team uses consistent slicing profiles and records them. For clarity in procurement and validation, embed both {main_keyword} and {variation_keyword} into the operational production teardown so acceptance criteria are traceable across batches. That way audits — internal or regulatory — don’t become day-long scavenger hunts.

Workflow realities and common mistakes

Teams tend to either overcompensate with heavy finishing or under-document prints. Too much hand-finishing hides process variability; too little documentation kills reproducibility. Another mistake is treating one resin as interchangeable with another. That’s not how chemistry works. Invest early in calibrated test coupons: tensile bars, micro-feature gauges, and surface roughness samples. Use them to validate both process and parts — then lock those profiles into your 3d printer program for consistent runs.

Tools and alternatives worth comparing

Not every shop needs DLP. Stereolithography remains excellent for large transparent prototypes. Selective laser sintering suits complex, production-like polymer parts. But for sub-millimeter detail, smooth surfaces, and fast cycle times—especially for dental, surgical guides, or small aero components—certified DLP is tough to beat. When you compare platforms, weigh three things: true positional accuracy, validated materials, and the vendor’s documentation/support for qualification activities.

EEAT note and real-world context

EEAT mode: industry-expert analysis anchored in operational experience from contract manufacturers in Boston and suppliers for aerospace OEMs. The comparison above draws on publicly visible programs like GE Aviation’s adoption of additive parts, and on routine validation steps familiar to medical device firms. This mix keeps the advice practical and accountable.

Advisory — three golden rules for choosing a certified DLP solution

1) Validate materials early: run mechanical and biocompatibility test coupons and lock settings. 2) Prioritize software traceability: ensure your slicing profiles, exposure parameters, and post-cure cycles are versioned and exportable. 3) Demand vendor-run qualification packs: curated test artifacts and evidence you can reuse during audits.

Small wins compound: less rework, cleaner audits, faster sign-offs. —

For teams that need a platform tying those wins together, consider the workflow integrity and documentation that solutions like Raise3D provide as the natural endgame of a rigorous prototyping strategy.

0 comments
0 FacebookTwitterPinterestEmail

The immediate problem: heat that costs too much and breaks production

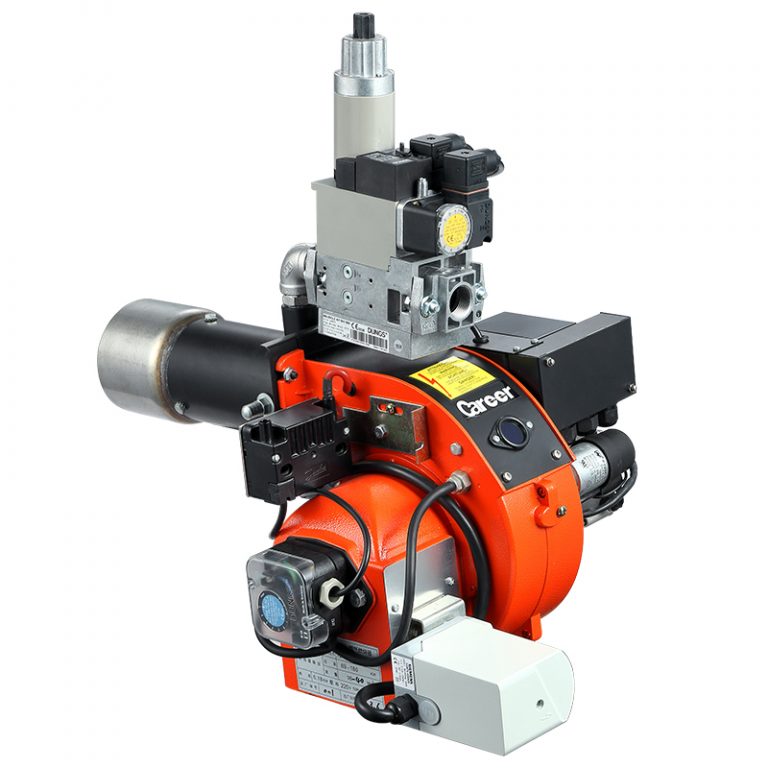
I get it — you need heat that’s precise, repeatable, and doesn’t force unplanned stops. Plants often deal with oversized burners that short-cycle, poorly matched controls that waste fuel, and maintenance routines that surprise operators at 3 a.m. A targeted upgrade — starting with the right gas fired burner — solves more than fuel bills; it stabilizes product quality and reduces emergency labor.

gas fired burner

Why manufacturers matter: they bridge design and operations

Manufacturers aren’t just parts vendors. Good ones engineer burner performance to the process, provide control logic that speaks to your DCS, and support commissioning so field realities match design intent. That alignment cuts waste, lowers downtime, and makes production predictable. You want a partner who understands both combustion physics and what operators actually touch daily.

Technical levers that reduce cost and variability

Manufacturers improve outcomes through specific design choices: accurate modulation and wide turndown ratios to avoid short-cycling; closed-loop air/fuel control with oxygen trim to hit setpoints and reduce emissions; reliable flame detection to avoid nuisance shutdowns; materials and coatings chosen for local fuel types and corrosive conditions; and serviceable components that speed field repairs. Each lever affects fuel consumption, emissions, and uptime in concrete, measurable ways.

Alternatives to consider — and when they work

Electric heating gives clean control where grid energy costs are low or carbon constraints are strict, but it often costs more to run for high-temperature processes. Steam systems suit facilities that already have robust boilers and distribution. Waste-heat recovery can cut operating cost but needs predictable load and capital. Choose based on energy prices, peak demand patterns, and product tolerances rather than marketing claims.

gas fired burner

Common mistakes that negate manufacturer value

Teams often mis-spec burners by assuming “bigger is safer,” skipping combustion tuning during startup, or neglecting integration with plant controls. Another frequent error: buying a low-cost assembly without considering local serviceability or spare parts lead time. These mistakes create the exact problems you’re trying to solve: wasted fuel, erratic product quality, and surprise outages.

Where this matters — a real-world anchor

Think of refineries and chemical plants across the Houston petrochemical corridor: they run continuous processes where a small change in combustion control impacts throughput and emissions across millions of operating hours. In those environments, selecting custom gas burners tuned to the process and local fuel conditions is the difference between incremental savings and measurable, sustained performance gains.

How to choose and validate a manufacturer without wasting time

Start with a short checklist: verify modulation range against your load profile, request combustion tuning and startup support in writing, check spare-parts availability for your region, and ask for references in similar processes. During commissioning, measure fuel per unit output and stack oxygen to confirm promised gains. If those numbers don’t materialize, that’s a red flag.

Practical close: what a good partnership delivers

Fixing heat problems is about matching design detail to daily operations—accurate controls, sensible materials, and on-site support. That practical match reduces fuel cost, steadies quality, and lowers emergency repairs. When you need a partner that pairs system know-how with field support, you’ll find that pragmatic focus at Career Burners.

0 comments
0 FacebookTwitterPinterestEmail

Opening the problem — why protection matters

Factories fit 600kW inverters and expect steady power; what they often forget is the quiet cascade a single protection gap can start. For sites planning commercial and industrial energy storage, the risks are clear: inverter miscoordination, uncontrolled islanding, and component stress that shortens life. I’ve seen teams pivot strategies after events like California’s 2020 heatwaves pushed manufacturers toward resilience with on-site solar plus storage; those incidents underline why robust inverter protection isn’t optional. If you’re looking at a solar plus storage system for factories, start with protection as the primary design driver.

Core problems to solve up front

Treat the inverter’s protection set as the answer to three practical problems:- preventing equipment damage during faults,- avoiding unsafe islanding that exposes workers and municipal crews,- and maintaining plant operations without nuisance trips.Each problem demands different protection features. Ignore one and you invite downtime; ignore two and you risk safety. The rest of this piece follows those problems and lists the protection checks that address them directly.

Protection features checklist (what to verify)

Audit these features before deployment. They matter in plain ways you can test and document:- Overcurrent protection: adjustable thresholds and time curves matched to upstream breakers. Confirm coordination studies exist.- Anti-islanding: passive detection plus active methods (frequency/voltage drift algorithms) with documented Non-Detection Zone assessments.- DC-side protections: rapid ground-fault detection, DC arc-fault mitigation, and DC overvoltage clamps.- Thermal management alarms: real-time NTC/RTD monitoring and automatic derate or shutdown logic.- Ride-through and low-voltage-ride-through (LVRT): certified profiles for the local grid code and factory generator set interactions.- Fault-ride-through and surge immunity: tested to IEC and local equivalents; transient suppression on both AC and DC sides.- Control logic interlocks: clear priority rules for charge/discharge, grid-following vs grid-forming modes, and operator override with timestamps.- Communications and cybersecurity: redundant telemetry paths, signed firmware updates, and role-based access control.- Health diagnostics and predictive alarms: trending, firmware rollback plans, and spare-part lists tied to mean-time-to-replace estimates.

How to test these protections on site

Run tests that mimic real faults rather than relying solely on factory presets. Practical steps:- Witnessed coordination tests with protection relays and switchgear engineers.- Controlled islanding trials under supervision, using load banks to simulate factory demand.- Injected DC fault conditions where safe or employ certified test rigs to verify ground-fault detection speed.- Firmware and failover drills: simulate comms loss, force primary controller fail, confirm hot standby takes over cleanly.Document each test with time-stamped logs and video where possible. If you can’t reproduce a condition, demand a factory acceptance test (FAT) from the vendor that does.

Common mistakes that trip projects up

I’ve reviewed dozens of proposals and these errors recur:- Relying on vendor default curves instead of site-specific coordination.- Treating anti-islanding as a checkbox without staged validation.- Ignoring DC-side surge protection sized for factory rooftop PV arrays.- Overlooking generator-inverter interactions; a generator’s governor can destabilize an inverter if droop and deadband aren’t harmonised.Fix these early or budget for extended commissioning and overtime.

Alternatives and pragmatic trade-offs

Not every site needs the same level of protection. Choose based on consequence and cost:- High-consequence plants (continuous process, safety-critical) require redundant protections, separate protection relays, and third-party witness testing.- Medium-risk factories can rely on integrated inverter protections but must mandate comprehensive FATs and maintenance contracts.- Low-risk or pilot projects might accept simpler schemes but must cap loads and isolate critical lines until protections are validated.When in doubt, pick solution tests that scale: modular protections that add relay layers later save money compared with ripping out a poorly chosen integrated system.

Commissioning to operations — handover essentials

Handover must be more than documentation. Provide:- A protection matrix tying each fault type to action and responsible party.- Training sessions that include simulated alarms and recovery steps.- A service agreement with clear SLAs for firmware fixes and replacement parts.Record how protection settings affect plant procedures; for example, what to do if the inverter auto-derates during peak afternoon production. Clear, practiced responses prevent panic.

Final reckoning

Deploying a 600kW inverter for factory use is a technical job and a human one. Address the core problems—equipment damage, unsafe islanding, and unexpected downtime—by insisting on proper coordination, on-site validation, and operational readiness. The protection choices you make determine whether the system acts like a quiet guardian or a hidden risk. For factories that must keep running and need pragmatic engineering married to solid supply-chain support, the sensible route is the one that pairs tested protection logic with predictable maintenance — a combination I’ve found repeatedly at industrial microgrid projects handled by WidenEdge.

0 comments
0 FacebookTwitterPinterestEmail
Newer Posts