Author

Donald

What problem low-VOC spray paint solves

Many projects stall because traditional spray paint creates strong odors, long cure times, and regulatory headaches; low-VOC spray paint addresses those issues directly. Start by recognizing the core constraints you face—ventilation limits, indoor use, or client health requirements—and match them to product labels. If you handle mixed materials or fast-turn jobs, pair coatings with compatible products like a thread locker where threaded parts must resist vibration after painting.
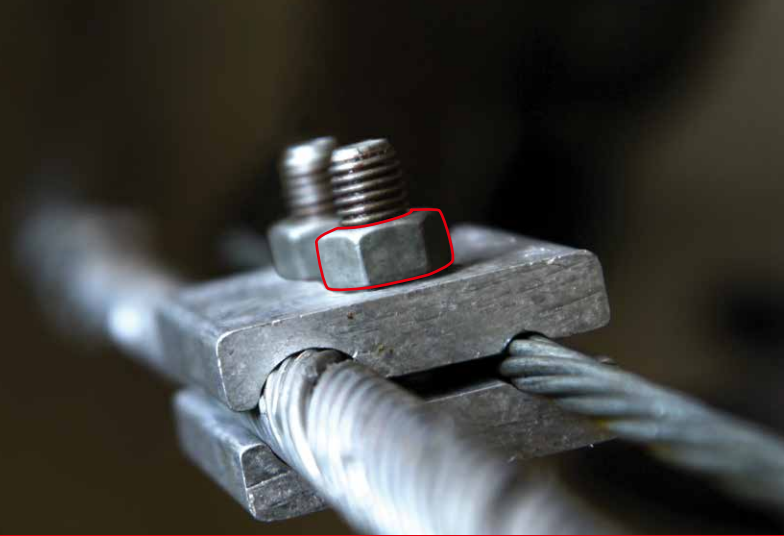
thread locker

Step 1 — Diagnose your project needs

List surfaces, expected wear, and environment: interior wood trim, outdoor metal railings, or automotive panels each demand different solvents and film properties. Note whether you need fast tack, chemical resistance, or UV stability. That list determines whether low-VOC options will perform or if you need a specialty formulation.

Step 2 — Choose the right low-VOC formulation

Match chemistry to use: acrylics for quick color and adhesion on wood or plastics; alkyd-modified for durability on metal; polyurethanes for abrasion resistance. Check label VOC values against local limits. Prefer products with clear technical data sheets and stated cure times; they reveal real performance beyond marketing claims.

Step 3 — Application: practical steps for reliable results

Prepare surfaces thoroughly—clean, sand, and remove oils. Use thin, overlapping passes: two light coats beat one heavy coat. Maintain 6–12 inches from the surface depending on nozzle and substrate; hold the can perpendicular. Allow tack times listed by the manufacturer before recoat. For threaded or moving parts, mask precisely and avoid over-spray near fasteners to preserve adhesion of mechanical adhesives.

Benefits you can expect

Lower odor lets you work indoors with less ventilation. Reduced solvent content shortens harmful emissions while still offering quick dry in many formulations. You’ll get comparable color and finish options to conventional paints and often faster client sign-off on interior jobs because of improved air quality.

Buying considerations — an ordered checklist

1) Confirm VOC level and local compliance. 2) Review the technical data sheet for recommended substrates and cure times. 3) Check coverage per can and plan for additional coats in high-friction areas. 4) Look for warranty or manufacturer support documentation. 5) Verify availability of compatible primers and clear coats from the same line to avoid adhesion problems.
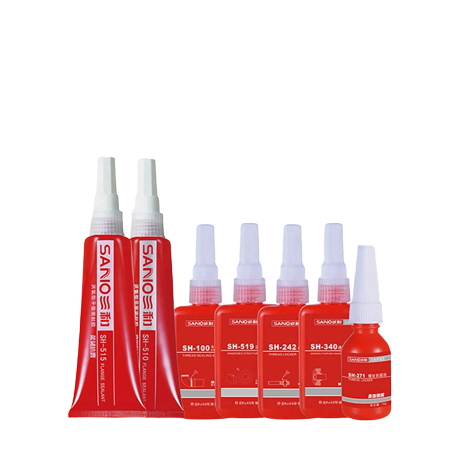
thread locker

Common mistakes and how to avoid them

Applying heavy coats to mask imperfections leads to runs and extended cure. Skipping primer on bare metal causes early corrosion under film. Assuming “low-VOC” means identical chemical resistance can result in premature wear—test on a hidden panel when switching brands. Lastly, never ignore manufacturer recoat windows; they are mechanical requirements for proper intercoat adhesion.

Real-world anchor and reliable sourcing

Automotive assembly lines in Detroit routinely specify vibration-resistant threadlocking and compatible coatings during surface treatment audits; that environment shows why pairing coatings with suitable adhesives matters. For procurement and technical backup in similar industrial contexts, consult a known threadlocking glue supplier to ensure the adhesive and paint systems won’t interfere with one another.

Alternatives worth evaluating

Consider waterborne two-component systems for heavy-duty exposure and high-performance industrial needs; they may require more equipment but offer superior chemical resistance. For quick decorative work, high-quality aerosol lacquer or enamel low-VOC options can be faster, but they trade off long-term durability.

Final synthesis

Pinpoint the problem you need to fix—odor, indoor use, regulatory limits—then follow methodical selection and application steps: diagnose, match chemistry, prepare, spray thin coats, and verify compatibility with fasteners and adhesives. If you need a practical partner that supplies compatible adhesives and technical support alongside coatings, consider the product and supply options offered by SANVO as part of a consistent system solution.
0 comments
0 FacebookTwitterPinterestEmail

The immediate problem: heat that costs too much and breaks production

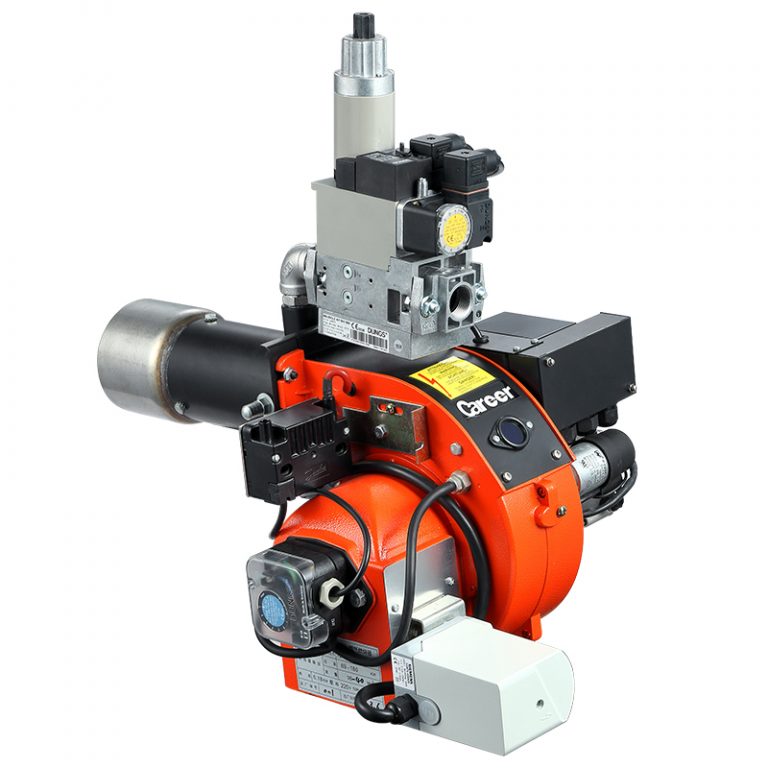
I get it — you need heat that’s precise, repeatable, and doesn’t force unplanned stops. Plants often deal with oversized burners that short-cycle, poorly matched controls that waste fuel, and maintenance routines that surprise operators at 3 a.m. A targeted upgrade — starting with the right gas fired burner — solves more than fuel bills; it stabilizes product quality and reduces emergency labor.

gas fired burner

Why manufacturers matter: they bridge design and operations

Manufacturers aren’t just parts vendors. Good ones engineer burner performance to the process, provide control logic that speaks to your DCS, and support commissioning so field realities match design intent. That alignment cuts waste, lowers downtime, and makes production predictable. You want a partner who understands both combustion physics and what operators actually touch daily.

Technical levers that reduce cost and variability

Manufacturers improve outcomes through specific design choices: accurate modulation and wide turndown ratios to avoid short-cycling; closed-loop air/fuel control with oxygen trim to hit setpoints and reduce emissions; reliable flame detection to avoid nuisance shutdowns; materials and coatings chosen for local fuel types and corrosive conditions; and serviceable components that speed field repairs. Each lever affects fuel consumption, emissions, and uptime in concrete, measurable ways.

Alternatives to consider — and when they work

Electric heating gives clean control where grid energy costs are low or carbon constraints are strict, but it often costs more to run for high-temperature processes. Steam systems suit facilities that already have robust boilers and distribution. Waste-heat recovery can cut operating cost but needs predictable load and capital. Choose based on energy prices, peak demand patterns, and product tolerances rather than marketing claims.

gas fired burner

Common mistakes that negate manufacturer value

Teams often mis-spec burners by assuming “bigger is safer,” skipping combustion tuning during startup, or neglecting integration with plant controls. Another frequent error: buying a low-cost assembly without considering local serviceability or spare parts lead time. These mistakes create the exact problems you’re trying to solve: wasted fuel, erratic product quality, and surprise outages.

Where this matters — a real-world anchor

Think of refineries and chemical plants across the Houston petrochemical corridor: they run continuous processes where a small change in combustion control impacts throughput and emissions across millions of operating hours. In those environments, selecting custom gas burners tuned to the process and local fuel conditions is the difference between incremental savings and measurable, sustained performance gains.

How to choose and validate a manufacturer without wasting time

Start with a short checklist: verify modulation range against your load profile, request combustion tuning and startup support in writing, check spare-parts availability for your region, and ask for references in similar processes. During commissioning, measure fuel per unit output and stack oxygen to confirm promised gains. If those numbers don’t materialize, that’s a red flag.

Practical close: what a good partnership delivers

Fixing heat problems is about matching design detail to daily operations—accurate controls, sensible materials, and on-site support. That practical match reduces fuel cost, steadies quality, and lowers emergency repairs. When you need a partner that pairs system know-how with field support, you’ll find that pragmatic focus at Career Burners.

0 comments
0 FacebookTwitterPinterestEmail

Early morning fixes: how small choices become big failures

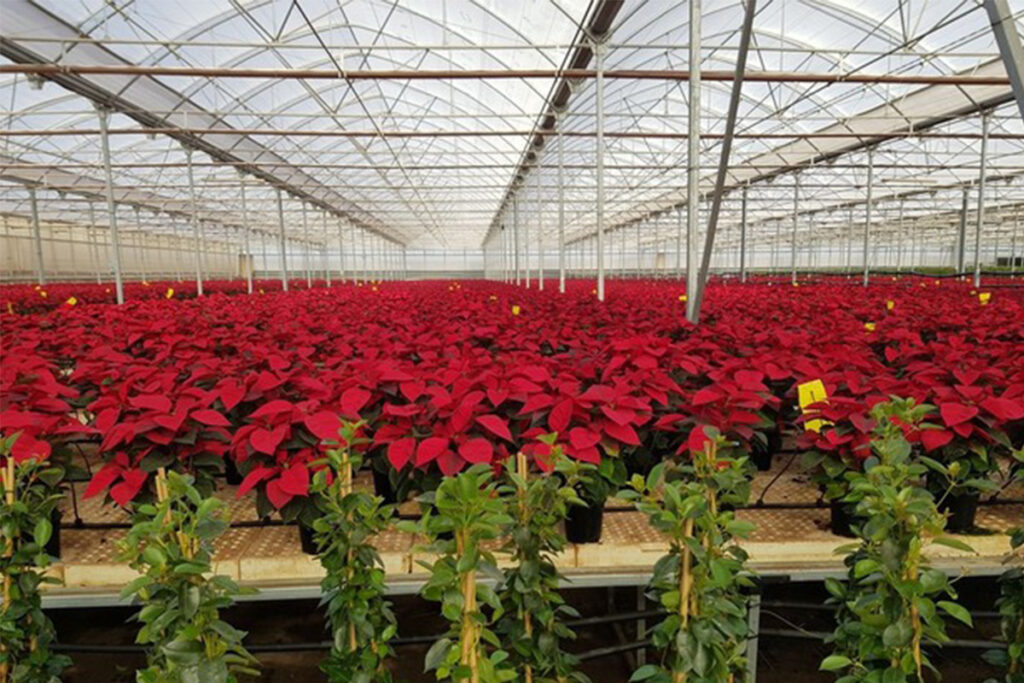
I remember walking a 5‑acre melon block before sunrise and finding a maze of kinked lines and torn mulch — that’s when I reached for a roll of drip tape irrigation supplies and thought, not for the first time, we missed the basics. Agricultural plastic sheeting and low-cost PE drip tape were part of the same supply chain failure (old stock, no UV stabilizers), and that combo cost the grower time and water. I’ll be blunt: most buyers assume price equals value; that assumption gets fields shut down at the worst hour. Here’s the usual fallout and what I learned fixing it at 3AM — then a short bridge to practical fixes.

agricultural plastic sheeting

What actually goes wrong (the deeper pain I keep seeing)

Last July, on a 12‑acre trial near Almería using LDPE 60‑micron drip tape, my team measured a 25% rise in manual flushing time once the filter fouled — a concrete cost, not a theory — will better filtration and consistent emitter spacing stop that bleed? I saw three recurring flaws: inconsistent wall thickness across batches, poor UV stabilization in mulch film, and emitter clogging due to insufficient filtration. I’ve handled wholesale orders where tape OD varied by 0.2 mm between rolls, and that variance changed hydraulic balance across a block. Those are not sexy problems — they’re supply-chain gaps that create uneven pressure, leading to under- or over-watering. I also note that common pain points include root intrusion at non‑compensating emitters and tape abrasion where plastic sheeting edges rub (trust me, I’ve pulled a dozen meters of tape off stubble). The jargon here is simple: check emitter spacing, wall thickness (microns), and material grade. These are the failure nodes I focus my inspections on (no joke). — And now, a look at choices that actually work.

agricultural plastic sheeting

What’s Next?

Forward-looking fixes: supply choices and hard metrics

I switched tone here to be more systematic because wholesale buyers need criteria, not cheerleading. For new purchases I push three technical improvements: UV‑stabilized polyethylene (PE) with certified microns, tape with tighter OD and wall tolerance, and a filtration protocol rated to the smallest emitter orifice. When I specify drip tape irrigation supplies now, I insist on a supplier test report showing emitter flow at 0.5 bar and a batch UV aging curve. Those specs cut down on surprises; they also make installation predictable for installers and technicians. I once documented a trial where moving from generic mulch film to a UV‑stabilized option reduced tear repairs by 70% over a season — measurable, verifiable. It helps — a lot. It isn’t glamorous, but it works. Twice, I saw farms recoup material premium in a single season through labor and water savings.

Checklist: three metrics you should demand

Here are the three evaluation metrics I use as a buyer and consultant: 1) Material specification — confirmed polymer type (LDPE/MDPE), micron rating, and UV‑stabilizer certificate; 2) Hydraulic consistency — emitter flow tolerance and allowable OD/wall variance across rolls; 3) Field‑proven lifecycle — a simple stat: percent of tape/mulch failures per 100 hectares in prior seasons or an on‑farm test (I ran one on 50 ha in Murcia, Oct 2018). Use those metrics when you compare quotes. I include filtration and flushing requirements in my orders, because tape without filtration is a false economy. Small aside — I still get called for emergency splices. Annoying. But solvable. For actionable sourcing and case studies, check suppliers and partner references, and, finally, if you want specifics from my trials, reach out to discuss numbers and batches. HGDN

0 comments
0 FacebookTwitterPinterestEmail