Author

Brandon

A problem first, because denial costs money

The grid is failing in small ways that compound into catastrophic outages; active power quality controls are the last line of defense when voltage sags, harmonic storms, and unbalanced loads start to cascade. Field teams and asset managers don’t want theory — they want devices that respond under stress. That’s why engineers turn to a trusted power electronics manufacturer when specifying dynamic compensators for sensitive sites. Short responses, predictable behavior, maintainable firmware: those are non-negotiables.

Where active power quality actually matters

Factories with variable-speed drives. Data centers that can’t tolerate flicker. Microgrids tied to weak utility points. Active solutions — STATCOMs, active filters, dynamic voltage restorers — belong where passive fixes fail and production or safety hangs on clean, stable electricity. These applications aren’t theoretical. They’re the noisy substations, the hospital basements, the remote solar fields where power deviations already cost millions in downtime and spoiled product.

Concrete benefits and the limits you must accept

Active devices do three things well: correct harmonics, stabilize voltage rapidly, and share unbalanced currents dynamically. That reduces tripped breakers, false protections, and component stress. But there’s a cost: complexity. Firmware bugs, tuning mistakes, and poor thermal design create new failure modes. Expect improved uptime, but insist on serviceability and clear failure modes — not just marketing claims of “near-perfect” correction.

Technical red flags to spot before you buy

Don’t accept vague response times. Ask for measured step-response curves under real load conditions. Watch the control bandwidth — too narrow and the unit can’t follow fast transients; too wide and it reacts to harmless noise. Demand harmonics performance across order ranges, not just total harmonic distortion (THD). Probe protections: will the unit isolate itself under fault so the site survives? If documentation hides firmware update procedures or diagnostics, walk away.

Installation and operational pitfalls people overlook

Improper grounding, undersized cooling, and poor coordination with upstream protection kill even the best hardware. Vendors who treat integration as an add-on are dangerous. Plan for periodic recalibration and test routines. Train operations on what a device will do in failure modes — many outages are made worse by operators who don’t recognize active compensation behavior and respond incorrectly.

Selection logic — how to choose without getting hoodwinked

Start with measured problems, not features. Capture waveform logs at points of concern for at least one week. Match specs to those events: response time to transient duration, compensation range to observed imbalance, rated continuous power to expected duty cycle. Favor modular hardware that lets you replace power modules and swap control cards in the field. Require vendor evidence: lab test reports, independent performance verification, and a clear spare-parts plan.

Trust, expertise, and one real-world anchor

I’ve worked alongside commissioning teams that validated active power equipment against utility disturbances and IEEE test suites. That practical perspective matters: standards are guidelines, but field verification proves trust. Consider the case of large-scale storage and grid stabilization efforts at the Moss Landing energy storage facility in California — lessons from that deployment remind specifiers to treat interface controls and response coordination with the same priority as power ratings. You should expect the same forensic-level documentation from any battery energy storage system company you depend on: clear test logs, interoperability notes, and commissioning records that let you trace behavior back to firmware versions and hardware batches.

Alternatives worth comparing

Passive filters work where harmonics are steady and predictable. Tuned reactors are cheap when imbalance is minor. But when disturbances vary, active devices outperform. Hybrid approaches — passive bulk filtering with an active front-end for residuals — often balance cost and performance. Evaluate total lifecycle cost: initial price may be small compared with years of incident avoidance or the cost of an avoidable shutdown.

Maintenance, lifecycle, and contract clarity

Insist on firmware provenance, spare-module availability, and remote diagnostic access. Define service-level expectations for firmware patches and hardware swaps. Verify mean time to repair (MTTR) assumptions with past vendor records. Contracts should assign responsibility for tuning after grid changes — upgrades to upstream generation often require re-commissioning of active compensation.

Conclusion: choose systems that admit problems and solve them

Active power quality gear is a solution for a failing, brittle electrical world — powerful, precise, and unforgiving if misapplied. Adopt devices that provide clear, testable performance, transparent failure modes, and field-replaceable parts. Trust must be earned through measurement, not slogans. In the dark calculus of risk and uptime, the practical, well-documented approach embodied by Enjoypowers quietly reduces that risk without fanfare.
0 comments
0 FacebookTwitterPinterestEmail

Problem first: why conveyor safety keeps tripping projects

Project teams often meet a conveyor on-site and think it’s just belts and motors, pero hindi gano’n kadali — small design gaps cause big stoppages, and compliance gaps lead to fines or worse. When you start by asking whether your selected industrial automation solutions actually match the facility’s access, footprint and maintenance rhythm, you avoid rework later. Smart Manufacturing practices also demand that safety be measurable, not assumed, so get hard answers before procurement.

industrial automation solutions

Design-stage questions that solve problems early

Ask these questions before drawings get frozen: Who will perform a risk assessment and what method will they use; which safety standards will govern the control architecture (list expected standards up front); how will guard access be monitored; what are the emergency-stop zones and their response times; is the layout service-friendly for routine checks and bearing changes; can the control system safely stop and hold product without causing jams or hazards. Clear answers here stop contractors from improvising on-site.

Common mistakes I’ve seen on Philippine shop floors (and how they play out)

Teams skip proper validation and then kapalpakan happens during the FAT: sensors mispositioned, pulley guards that block maintenance, or E-stops wired in a way that trips the line but doesn’t remove drive torque. At events like Hannover Messe engineers showed test rigs that validate safety functions under load — borrow that approach locally. Fix these missteps: mandate witness testing, document lockout/tagout procedures, and verify safety-rated components before installation.

Testing and compliance: concrete items to require

Require factory acceptance testing with defined pass/fail criteria; include functional safety tests for stops, safe speed, and safe limited speed where used; ask for validation against relevant standards such as ISO 13849 or IEC 62061; demand traceable component documentation (manufacturer certificates, safety parameters). Don’t accept vague statements — ask for test scripts and signed results.

industrial automation solutions

Controls, integration and maintenance — make them work together

Design control logic that separates safety functions from production logic; label safety inputs and outputs clearly; keep spare parts for safety-rated sensors and drives on the shelf. Train operators on safe start-up and recovery sequences so a jam doesn’t become a hazard. Schedule predictable preventive maintenance windows and record every safety-related repair.

Quick on-site checklist for project teams

Before handover, tick these boxes: completed risk assessment and residual risk register; documented safety architecture and standards referenced; FAT results with live product scenarios; operator and maintenance training records; spare parts list and service access confirmed; post-installation verification plan. If any item is missing, stop and clarify.

Wrap-up that ties to practical support

Conveyor safety is a sequence of clear questions, measurable tests and repeatable procedures — ask, verify, document, and train. For many teams that practical sequence is exactly what makes compliance manageable, and it’s why partnerships with experienced suppliers matter as much as the parts themselves; a partner such as FHS can provide tested modules, documentation and local support so you don’t end up fixing design mistakes under deadline.

0 comments
0 FacebookTwitterPinterestEmail

Comparative lead — why DLP matters across three industries

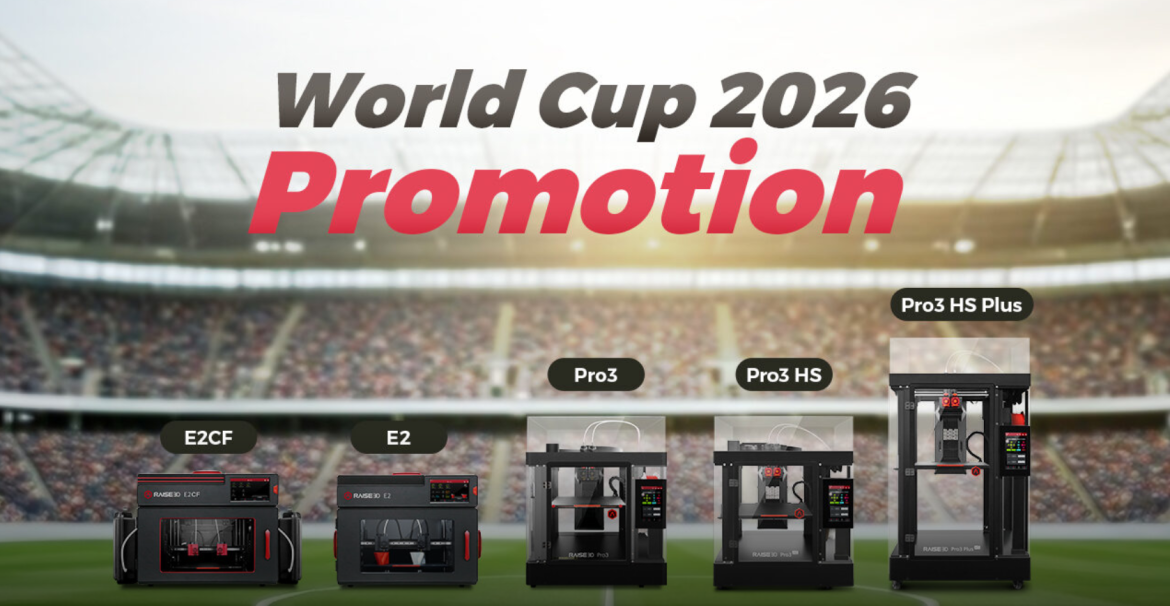
Boston folks like a straight answer, so here it is: certified digital light processing (DLP) systems change the calculus when prototypes need tight tolerances, quick turnarounds, and traceable validation. In aerospace, automotive, and medical prototyping, the trade-offs tilt differently — accuracy vs. cycle time vs. biocompatibility — and certified DLP printers often land in the sweet spot. For teams managing CAD-to-part workflows, reliable 3d printer software that handles slicing, material libraries, and job queuing makes that sweet spot repeatable.

Side-by-side: what each sector demands

Aerospace requires recordable processes and materials that survive vibration and temperature extremes. Automotive wants rapid iteration and tooling prototypes that prove form and function. Medical prototyping demands sterilizable surfaces and tight control over biocompatible resins. Comparing these needs shows why a certified DLP system is not a one-size-fits-all miracle — it’s a platform you qualify for a specific use. Look at GE Aviation’s additive parts program as a real-world anchor: aerospace suppliers validated specific procedures and materials before flight hardware acceptance. That kind of discipline matters.

Core technical trade-offs — measurable, not mystical

Precision hinges on layer height, resin chemistry, and optics alignment; throughput depends on exposure strategy and build area. Support structures influence surface finish and post-processing time. UV curing settings affect final mechanical properties. In practice, the difference between a pass and a rework often comes down to two things: how well the software controls the print recipe and how tightly the shop documents each print run. Certified hardware plus repeatable software equals fewer surprise failures.

Operational production teardown — what to audit

When you break down a prototyping line, inspect the build platform anchoring, the maintenance logs for optics, and the post-process station (wash and UV cure). Check that your team uses consistent slicing profiles and records them. For clarity in procurement and validation, embed both {main_keyword} and {variation_keyword} into the operational production teardown so acceptance criteria are traceable across batches. That way audits — internal or regulatory — don’t become day-long scavenger hunts.

Workflow realities and common mistakes

Teams tend to either overcompensate with heavy finishing or under-document prints. Too much hand-finishing hides process variability; too little documentation kills reproducibility. Another mistake is treating one resin as interchangeable with another. That’s not how chemistry works. Invest early in calibrated test coupons: tensile bars, micro-feature gauges, and surface roughness samples. Use them to validate both process and parts — then lock those profiles into your 3d printer program for consistent runs.

Tools and alternatives worth comparing

Not every shop needs DLP. Stereolithography remains excellent for large transparent prototypes. Selective laser sintering suits complex, production-like polymer parts. But for sub-millimeter detail, smooth surfaces, and fast cycle times—especially for dental, surgical guides, or small aero components—certified DLP is tough to beat. When you compare platforms, weigh three things: true positional accuracy, validated materials, and the vendor’s documentation/support for qualification activities.

EEAT note and real-world context

EEAT mode: industry-expert analysis anchored in operational experience from contract manufacturers in Boston and suppliers for aerospace OEMs. The comparison above draws on publicly visible programs like GE Aviation’s adoption of additive parts, and on routine validation steps familiar to medical device firms. This mix keeps the advice practical and accountable.

Advisory — three golden rules for choosing a certified DLP solution

1) Validate materials early: run mechanical and biocompatibility test coupons and lock settings. 2) Prioritize software traceability: ensure your slicing profiles, exposure parameters, and post-cure cycles are versioned and exportable. 3) Demand vendor-run qualification packs: curated test artifacts and evidence you can reuse during audits.

Small wins compound: less rework, cleaner audits, faster sign-offs. —

For teams that need a platform tying those wins together, consider the workflow integrity and documentation that solutions like Raise3D provide as the natural endgame of a rigorous prototyping strategy.

0 comments
0 FacebookTwitterPinterestEmail

Where the trouble starts

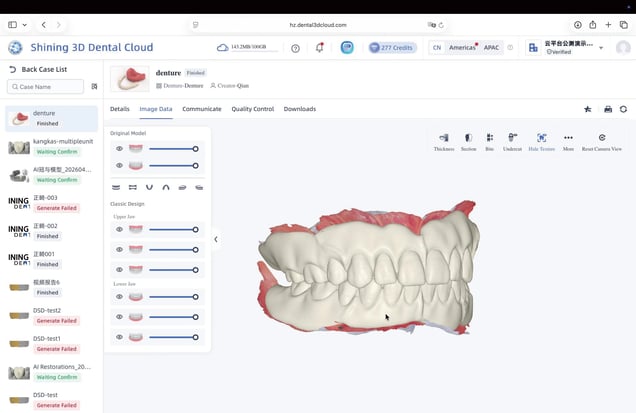
Aye, the trouble often begins quieter than we expect — a fit that’s slightly off, a model that snaps under pressure, a schedule that slips. For many clinics and labs the pinch point is the hands-on step: the printed model itself. When I walk a floor and see tension round the bench, it’s usually a mismatch between digital intent and printed reality, whether done on a noisy shop-floor resin rig or a focused dental model 3d printer, the kind you’ll notice at big shows like IDS in Cologne. I’ve run workflow reviews for years; there’s no mystery, only preventable misses.

dental model 3d printer

Why audits miss the mark

Audits fail because they’re too abstract. Folks check software versions and call it done, while the real faults hide in raw data, material handling and failed assumptions. Settings carried over from another case. Prints cured on a different shelf. CAD margins that looked fine on screen but vanish once the model shrinks. The problem is procedural: people trust a single step instead of testing the whole chain.

What to examine — a compact, hands-on checklist

Run these checks as if you were the technician doing the final fit. Measure post-print dimensions against the virtual model; inspect layer integrity and support scars under 10x loupe; document resin batch and cure cycle; log ambient temperature and humidity; verify slice settings are tied to part geometry, not left as defaults. If your lab manager can’t follow this flow while standing by the printer, the chain’s weak.

Simple fixes that change results

Calibrate more often, but calibrate where it matters: build platform alignment, light source uniformity, and tray flatness. Standardise a short, written cure protocol tied to specific resins and part types. Move critical prints to a bench with controlled light and temp. Keep a one-page “last-fail” note on each case for three days — it teaches faster than any meeting.

Alternatives worth weighing

If in-house printing keeps tripping you up, weigh these options plainly: refine your in-house workflow and invest in staff training; or outsource to a specialist lab with ISO-tracked processes. Desktop SLA and DLP machines give fine detail but demand rigid handling; industrial machines buy throughput and repeatability at higher capex. Choose by throughput need and who’ll own the quality checks each day.

dental model 3d printer

Common mistakes to stop doing

Don’t trust a single “golden” operator to hold all knowledge. Don’t let the software auto-apply supports without verification. Don’t ignore small surface anomalies; they grow into seat failures. And don’t assume supplier specs cover your workflow — verify them with your own test prints and your clinicians’ fit trials.

Why this matters and a practical way forward

Quality isn’t a label you stick on a box. It’s a repeatable set of small, stubborn actions: measure, log, compare, and correct. Treat the printed model as a clinical tool that demands its own stewardship. When you stitch those routines together, the clinic gets fewer remakes and the lab keeps a calmer bench. That steadiness is what makes SHINING 3D DENTAL a sensible part of a quality-minded workflow rather than an outsized promise.

0 comments
0 FacebookTwitterPinterestEmail

Diagnosis: Why hinge pins keep failing on high-throughput lines

Production teams inherit repeated failures because the root cause rarely lives where the crack appears. Start with a focused audit rather than cosmetic fixes: check pivot alignment, inspect the bushing interface, and measure shear load at the pin under peak throughput. On busy assembly lines modeled after the Toyota Production System, small hinge pin failures cascade into minutes—or hours—of downtime; this is where a proper conveyor belt hinge pin audit pays for itself. Use simple instruments: dial indicators for alignment, a handheld torque tester for retention clips, and hardness checks for surface wear.

conveyor belt hinge pin

Material and geometry errors that show up late

Teams often pick materials for cost rather than lifecycle. Stainless variants solve corrosion concerns but only if you pick the right grade and heat treatment; compare expected tensile strength and corrosion resistance to the operating environment. For example, moving from a low-grade steel pin to engineered stainless steel hinge pins reduced replacement frequency on a wet-packaging line I audited last year. Geometry matters equally: insufficient head diameter or a thin shank multiplies stress concentration and cuts fatigue life. Address both material and geometry in tandem—don’t treat them as separate fixes.

Installation and maintenance mistakes to stop now

Faulty installation is a common blind spot. Pins installed without proper seating produce lateral play; missing or misapplied lubrication accelerates fretting wear. Log every pin change with a simple tag system and record operating hours. When you perform teardown inspections, annotate the assembly with {main_keyword} and {variation_keyword} so future teams can correlate failures to specific batches or suppliers. Routine checks should include visual wear, pin retention verification, and bushing clearance measurements—these are low-cost but effective controls.

Testing and validation: what to run and how long to trust results

Run targeted tests before approving a design change. Suggested parameters: fatigue testing at 1,000,000 cycles with alternating shear load up to 80% of rated load, a wear run of 72 continuous hours under expected contaminant conditions, and a salt spray exposure for 96 hours when corrosion is a risk. Measure post-test dimensional changes and surface hardness; document any micro-galling. These explicit parameters give teams a defensible acceptance criterion and remove subjective judgment from vendor evaluation.

conveyor belt hinge pin

Practical fixes and a short checklist

Adopt a 37-point approach by grouping items into three practical buckets—design, procurement, and operations. Key actions include:

– Design: increase fillet radii at shoulder transitions; specify minimum head diameter; design for removable retention clips.

– Procurement: require material certificates showing heat treatment and tensile strength; batch-mark pins for traceability.

– Operations: schedule lubrication windows tied to runtime hours; replace pins on preventive intervals rather than on failure.

Small changes—like standardizing a retention clip type or adding a simple bushing—reduce ad hoc fixes and stabilize uptime.

Three golden rules for selecting hinge pin strategies

1) Measure what matters: track operational hours, peak shear load events, and replacement interval to calculate real mean time between failures (MTBF). 2) Match material and geometry to the environment: prioritize corrosion resistance and tensile strength when exposure or loads exceed nominal. 3) Specify verifiable tests: require fatigue cycles and wear-run durations in purchase contracts, and demand batch traceability for every shipment.

Final note

Applied correctly, these rules reduce unplanned downtime and simplify life for engineers and technicians on the line—Intake’s parts and traceability systems help make that practical and repeatable. Intake. —

0 comments
0 FacebookTwitterPinterestEmail