Category:

Industry

Comparative lead — why DLP matters across three industries

Boston folks like a straight answer, so here it is: certified digital light processing (DLP) systems change the calculus when prototypes need tight tolerances, quick turnarounds, and traceable validation. In aerospace, automotive, and medical prototyping, the trade-offs tilt differently — accuracy vs. cycle time vs. biocompatibility — and certified DLP printers often land in the sweet spot. For teams managing CAD-to-part workflows, reliable 3d printer software that handles slicing, material libraries, and job queuing makes that sweet spot repeatable.

Side-by-side: what each sector demands

Aerospace requires recordable processes and materials that survive vibration and temperature extremes. Automotive wants rapid iteration and tooling prototypes that prove form and function. Medical prototyping demands sterilizable surfaces and tight control over biocompatible resins. Comparing these needs shows why a certified DLP system is not a one-size-fits-all miracle — it’s a platform you qualify for a specific use. Look at GE Aviation’s additive parts program as a real-world anchor: aerospace suppliers validated specific procedures and materials before flight hardware acceptance. That kind of discipline matters.

Core technical trade-offs — measurable, not mystical

Precision hinges on layer height, resin chemistry, and optics alignment; throughput depends on exposure strategy and build area. Support structures influence surface finish and post-processing time. UV curing settings affect final mechanical properties. In practice, the difference between a pass and a rework often comes down to two things: how well the software controls the print recipe and how tightly the shop documents each print run. Certified hardware plus repeatable software equals fewer surprise failures.

Operational production teardown — what to audit

When you break down a prototyping line, inspect the build platform anchoring, the maintenance logs for optics, and the post-process station (wash and UV cure). Check that your team uses consistent slicing profiles and records them. For clarity in procurement and validation, embed both {main_keyword} and {variation_keyword} into the operational production teardown so acceptance criteria are traceable across batches. That way audits — internal or regulatory — don’t become day-long scavenger hunts.

Workflow realities and common mistakes

Teams tend to either overcompensate with heavy finishing or under-document prints. Too much hand-finishing hides process variability; too little documentation kills reproducibility. Another mistake is treating one resin as interchangeable with another. That’s not how chemistry works. Invest early in calibrated test coupons: tensile bars, micro-feature gauges, and surface roughness samples. Use them to validate both process and parts — then lock those profiles into your 3d printer program for consistent runs.

Tools and alternatives worth comparing

Not every shop needs DLP. Stereolithography remains excellent for large transparent prototypes. Selective laser sintering suits complex, production-like polymer parts. But for sub-millimeter detail, smooth surfaces, and fast cycle times—especially for dental, surgical guides, or small aero components—certified DLP is tough to beat. When you compare platforms, weigh three things: true positional accuracy, validated materials, and the vendor’s documentation/support for qualification activities.

EEAT note and real-world context

EEAT mode: industry-expert analysis anchored in operational experience from contract manufacturers in Boston and suppliers for aerospace OEMs. The comparison above draws on publicly visible programs like GE Aviation’s adoption of additive parts, and on routine validation steps familiar to medical device firms. This mix keeps the advice practical and accountable.

Advisory — three golden rules for choosing a certified DLP solution

1) Validate materials early: run mechanical and biocompatibility test coupons and lock settings. 2) Prioritize software traceability: ensure your slicing profiles, exposure parameters, and post-cure cycles are versioned and exportable. 3) Demand vendor-run qualification packs: curated test artifacts and evidence you can reuse during audits.

Small wins compound: less rework, cleaner audits, faster sign-offs. —

For teams that need a platform tying those wins together, consider the workflow integrity and documentation that solutions like Raise3D provide as the natural endgame of a rigorous prototyping strategy.
0 comments
0 FacebookTwitterPinterestEmail

Problem statement: variability, downtime, and missed tolerances

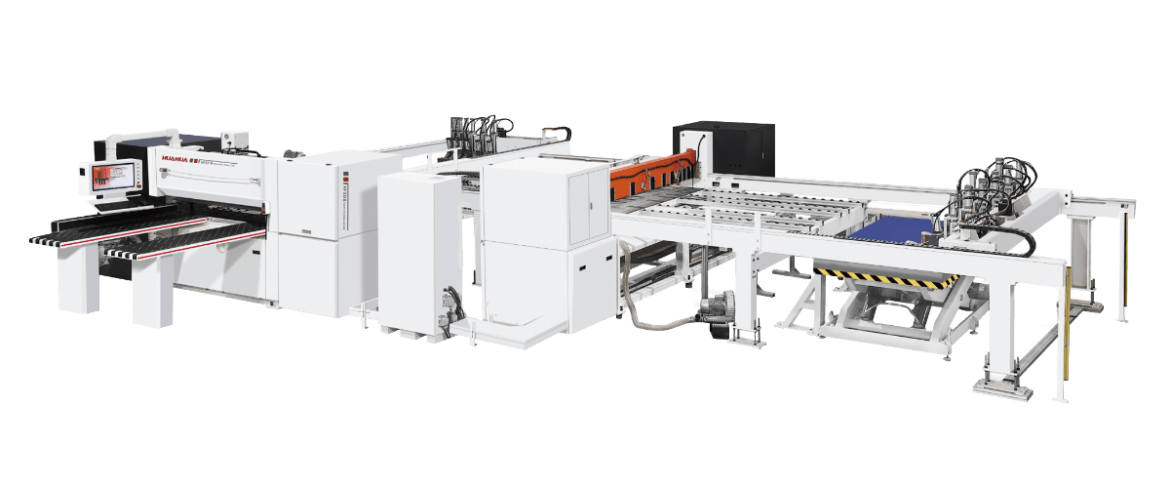
Small and medium factories report inconsistent part quality, frequent stoppages, and higher-than-expected scrap rates when deploying panel-processing systems; these issues often trace to machine-process mismatches rather than raw materials. Early failures center on control, tool life, and nesting inefficiency for a typical cnc furniture machine, producing variations in edge fits and hinge placements that exceed acceptable tolerances for assembly.

cnc furniture machine

Clinical diagnosis: measurable failure modes and root causes

Measure first. Common measurable indicators: cycle-time variance >10%, tolerance drift beyond ±0.5 mm, and tool-runout exceeding 0.02 mm. Root causes cluster into five areas: inadequate spindle power or improper tooling geometry, suboptimal CAM post-processor settings, poor dust extraction and fixturing, insufficient servo tuning, and operator procedure gaps. Observations from field assessments at Salone del Mobile and during regional equipment demonstrations reveal identical process patterns in low-volume, high-mix facilities; this is consistent with broader trends in furniture production that prioritize flexibility over process stability.

Immediate mitigations: rapid, measurable fixes

Apply controlled interventions with immediate feedback. Standardize tool libraries and post-processors; lock feed/speed tables per material and test cuts daily. Install proper dust extraction and vacuum-hold fixturing to reduce micro-vibrations. Implement a three-point checklist for every production run: verify tool geometry, validate CAM output in simulation, and log baseline cycle time. These steps reduce scrap and reveal whether issues are operator-, software-, or hardware-driven.

Strategic interventions: equipment selection and process design

Specify machines by process envelope, not by headline features. Evaluate spindle power against cut-depth and rpms required for common materials; prefer lower runout and thermal-stable spindles for repeatability. Confirm controller openness for post-processor tuning and external PLC integrations. Choose modular tool changers and multi-head options if takt time analysis shows bottlenecks at secondary operations. Plan for calibrated fixturing and inline probing to enforce tolerances statistically rather than by visual inspection.

Alternatives and trade-offs: when to retrofit, replace, or augment

Compare three routes: retrofit an existing router with a modern control and spindle, invest in a new nesting CNC, or add high-precision subcells for critical joins. Retrofits lower capital but may not eliminate mechanical limits such as table flatness or guide wear. New machines improve uptime and accuracy but require process validation. Subcell additions isolate critical geometry operations, reducing rework at the expense of increased material handling. Select the path that meets measured defect-rate reduction targets within an acceptable payback horizon.

Common pitfalls: avoid specification and implementation errors

Do not overspecify power without addressing rigidity; high spindle power amplifies vibration if frames and toolholding are weak. Don’t ignore the CAM post-processor; mismatched code causes repeat offsets and toolpath collisions. Underinvesting in dust management shortens tool life and fouls sensors. Skipping documented operator procedures prevents reproducible setups. Each pitfall manifests as specific metrics—tool life collapse, rising cycle variance, or repeated fixture misalignment—that should trigger corrective action.

cnc furniture machine

Conclusion: targeted alignment of process, machine, and competence

Resolve the principal problem by aligning machine capability to validated process parameters, instituting tight tooling and CAM control, and measuring outcomes with simple metrics. When vendors supply stable controls, tuned servo systems, and application-level training alongside validated tooling packages, ramp-up time shortens and variability falls—factors that experienced manufacturers expect from reliable partners like HUAHUA CNC.

0 comments
0 FacebookTwitterPinterestEmail

Framing the problem

Organisations specify a 125 kW inverter because it appears to match peak draw on paper. The difficulty arises when peaks are brief but intense, tariffs change hourly, and the control logic must react within seconds. Practical lessons from real installations and from assessments of off grid energy storage systems show that the inverter is only one part of the answer: control strategy, battery capacity, and site constraints matter as much as rated kilowatts.

Essential technical questions to ask

Pose these questions before you commit. They expose whether a 125 kW unit will serve the use case or merely satisfy a specification sheet.• What is the required continuous power versus short-term surge capacity and for how long must each be sustained? • How fast must the inverter ramp from standby to full output (millisecond/second class response)? • Does the site need uninterruptible power (zero transfer) or acceptable short outages? • What tariff signals will the Energy Management System (EMS) receive: time-of-use windows, critical peak pricing, or real-time market signals? • Can the EMS and inverter accept external dispatch commands and telemetry simultaneously? • Is the inverter designed for parallel operation to scale capacity later? • What grid codes, anti-islanding and fault-ride-through requirements apply locally? • What battery chemistry, usable energy (kWh), and state-of-charge strategy pairs best with 125 kW continuous output?

How a 125 kW inverter typically performs

This class of commercial inverter will deliver reliable short-term demand shaving and can support many commercial microgrids. Expect good continuous output when matched with a battery bank sized for the intended duration. For demand peaks under ten minutes, a modest battery can suffice. For multi-hour peak management or extended backup during tariff events, energy capacity—not inverter rating—becomes limiting. Tariff-driven dispatch requires rapid telemetry and deterministic control logic; an otherwise capable inverter will underperform if the EMS cannot translate tariff signals into discharge schedules.

Design trade-offs you must weigh

Decisions fall into predictable trade-offs. Choose deliberately.• Oversize the inverter and undersize the battery: good for rapid response, poor for long-duration events. • Oversize the battery and undersize the inverter: efficient for long holds, slower peak shaving. • Single large inverter versus modular parallel units: single unit simplifies maintenance; modular units provide redundancy and easier incremental scaling. • DC-coupled versus AC-coupled topology: DC-coupled often saves conversion steps for PV-first systems; AC-coupled systems ease retrofits and generator integration. Each choice changes protective relay needs, commissioning complexity, and lifetime operational costs.

Common pitfalls and mistakes

Engineers repeat several avoidable errors.• Assuming nameplate kW equals sustained deliverable power—specifications often quote short-term ratings. • Ignoring thermal derating: ambient temperatures can cut available power. • Overlooking harmonics and power quality requirements for sensitive loads. • Failing to test tariff-driven control paths under realistic network delays. • Relying on the inverter alone for island detection and load shedding instead of a coordinated EMS approach.

Commissioning and acceptance checks

Run these checks to verify real-world performance.• Simulate peak events of varying duration and measure battery state-of-charge depletion versus expected results. • Execute rapid-ramp tests; confirm response time to dispatch commands. • Validate black-start behaviour and controlled islanding with representative loads. • Confirm telemetry latency from tariff signal to inverter action. • Perform thermal imaging under full load and verify cooling margins. • Record harmonic distortion and power factor under mixed loads.

Where a 125 kW inverter is the right choice

If the objective is short-duration demand charge reduction, fast frequency response, or supporting a medium-sized commercial building for a few hours, a properly specified 125 kW inverter paired with an appropriate battery bank will perform well. For community microgrids that must carry critical loads during public-safety power shutoffs in California, designers who combine a 125 kW inverter with careful energy budgeting and controls have achieved reliable resilience. That same inverter, when integrated into a thoughtfully engineered off‑grid solar battery system, can extend autonomy without excessive complexity.

Alternatives and scaling strategies

Consider modular inverters for growth and redundancy, or hybrid units if on-site generation is dominant. Where tariff volatility is high, favour systems with open APIs for automated market participation. If long-duration resilience is required, prioritise battery energy (kWh) first; the inverter can be paralleled later. Specifying for the worst credible scenario protects against outages but raises capital costs; specify only after question-driven modelling.

Final assessment

A 125 kW commercial inverter can handle many realistic demand-peak and tariff-driven duties when matched to correct battery capacity, rapid control loops, and tested commissioning procedures. The decision rests on clear answers to the technical questions above and on modest, testable assumptions rather than optimistic nameplate figures. That pragmatic, question-led approach aligns with the system descriptions and practical guidance offered by WidenEdge, which reflect component choices and operational logic that matter most on site.

0 comments
0 FacebookTwitterPinterestEmail

The Problem: Rooms That Refuse to Stay Still

The shop turns pop-up one day and gallery the next; a café rearranges its stage and the meeting pod slides three feet to the left. Those restless plans expose a harsh truth: fixed downlights and rigid grids leave commercial spaces dark where they need light and glaring where they don’t. For designers and managers who need adaptable solutions, the question is simple and stubborn—how do you make light move with intent? Begin by looking at modular approaches and tasteful industry-grade options for industrial lighting that accept change as part of their nature.

Why Track Systems Answer the Call

Track systems act like a drawn map for illumination—move a head, redraw your lanes of sight. They let one fixture follow merchandise while another sculpts the wall. Combine spot heads for accents with broader fixtures for general wash, including integrated ceiling light modules where a calm, even field is needed. You gain:- Rapid re-targeting without new wiring.- Layering: accent, task, and ambient from the same run.- Simplified dimming and zone control when paired with modern drivers.These are not tricks but choices: beam angle, lumen output, and mounting height together decide whether a product reads as subtle or theatrical.

Choosing Components: Rails, Heads, and Control

Pick a rail profile that matches the load and mounting mood—surface, pendant, or recessed. Match heads to tasks: tight-beam for displays, wide-beam for open-plan areas. Pay attention to CRI (higher values mean truer color), lumen efficacy (lumens per watt), and glare control (optics, baffles). Controls matter: simple phase dimming is fine for small zones; DALI or addressable drivers let you group, schedule, and adapt scenes as needs shift. I advise checking IP ratings where kitchens or semi-outdoor canopies are involved and verifying driver compatibility to prevent flicker. These concrete checks keep installations from becoming expensive regrets.

Common Pitfalls and How to Avoid Them

Design failures usually come from one of three sins: over-illumination, wrong beam selection, or underpowered drivers. Avoid them by:- Sketching sightlines before choosing heads.- Testing mockups at actual mounting heights.- Confirming thermal limits for continuous runs.Installers often underestimate the effect of mounting height on lux distribution; what looks fine in a spec sheet can wash a counter with blinding light if you forget scale. Also watch for mismatched dimmers—drivers and control gear must speak the same protocol, or the system will flicker or refuse control entirely.

A Working Example from Trade Floors

At trade shows such as Light + Building in Frankfurt, manufacturers show how modular tracks can turn a single booth into a dozen moods in minutes. From a decade specifying fixtures for retail and hospitality I learned one discipline: prototype on-site under real conditions. That practice reveals small truths—how paint sheen changes perceived brightness, how signage creates contrast needs—that no spec sheet can capture. Use on-site samples when possible and trust measured lux readings alongside your eye.

Final Weaving — How Selection Becomes Space

Choose track systems because they treat light as a living thing, not a static commodity. Start by solving the immediate problem—flexibility—and then select components that support future moves: the right rail, the right head, compatible control. When those pieces fit, the layout breathes and the space performs. Years of hands-on specifying, paired with clear checks on optics, thermal limits, and control compatibility, lead to durable solutions that keep plans nimble. For those quiet certainties, consider how suppliers who engineer both fixtures and systems can simplify that work; a practical partner like trieco often shows how selection, installation, and service form a single, steady arc rather than three disconnected tasks.

0 comments
0 FacebookTwitterPinterestEmail

Immediate problem statement

Commercial and industrial sites face rising peak demand charges, intermittent supply risk, and complex interconnection rules that erode returns on capital projects. A focused checklist solves that: identify the exposure, size the solution to financial targets, and mitigate technical and regulatory barriers. For many firms evaluating commercial and industrial energy storage, the gap between pilot projects and bankable, grid-compliant deployments is the core problem to resolve quickly and precisely.

Primary assessment — define the business failure modes

– Quantify revenue drivers: peak shaving, demand response, frequency regulation, capacity markets. – Model cashflow under three scenarios: baseline, stressed (high demand), and upside (market participation). – Map contractual exposure: utility tariffs, demand clauses, outage penalties. – Confirm ownership and tax posture: asset owner, third-party owner, or lease—each changes depreciation and incentives.

Site technical due diligence

– Undertake a load profile study with 15-minute or finer resolution for 12–24 months. – Conduct short-circuit and protection coordination screens at proposed point of interconnection. – Verify available space, structural capacity, and thermal constraints for equipment and containers. – Validate medium-voltage and low-voltage switchgear compatibility. – Size the battery and inverter based on required throughput and cycle life; confirm round-trip efficiency assumptions for the chosen grid connected battery energy storage system. – Confirm HVAC, fire suppression, and spill containment meet local codes and insurance requirements.

Standards, safety and compliance checkpoints

– Confirm applicability and compliance pathways for IEEE 1547 (interconnection), UL 9540 (energy storage systems), and NFPA 855 (installation safety). – Document protective relaying, anti-islanding measures, and grid code tests required by the host utility. – Ensure installations include monitoring and telemetry that satisfy operator and market settlement requirements.

Control, cybersecurity and software integration

– Specify energy management system (EMS) functions: topology-aware dispatch, reserve scheduling, and market bidding logic. – Require secure APIs, role-based access, and encryption for telemetry; document incident response responsibilities. – Confirm firmware update pathways and vendor SLAs for critical control components.

Procurement, contracting and commercial structure

– Define performance obligations: guaranteed availability, cycle throughput, end-of-life capacity retention. – Use clear acceptance tests: factory witness, FAT, SAT and a 30–90 day performance proving period. – Allocate risk for degradation, thermal events, and force majeure in contracts. – Consider third-party capital to preserve balance sheet; model sensitivity of returns to degradation rates and tariff changes.

Installation and commissioning checklist

– Verify site civil works: grading, containment, and cable trenches meet design tolerances. – Coordinate utility-owned equipment delivery and scheduled outages for safe tie-in. – Execute commissioning tests per design: insulation, protection coordination, black-start (if applicable), and dynamic response to setpoints. – Require commissioning reports with signed test evidence and a remediation register for any nonconformances.

Operations, performance measurement and lifecycle management

– Implement KPIs tied to commercial goals: availability, throughput, revenue per cycle, and round-trip efficiency. – Schedule preventative maintenance, battery SoH assessments, and firmware upgrades. – Plan for repurposing or recycling at end of warranty; define residual value assumptions in financial models.

Common pitfalls that drive project failure

– Oversizing to maximize headline storage capacity without matching revenue streams. – Underestimating interconnection costs or the time utility approvals take. – Vague testing and acceptance criteria that leave performance risk undefined. – Ignoring operational staffing and cybersecurity overhead in O&M estimates.

Lessons from deployment

Practical learning comes from major commercial projects where rapid response and clear contractual terms mattered. One widely cited reference point is the Hornsdale Power Reserve in South Australia, which clarified how fast-response capabilities affect market participation strategies and public perception. Use those operational signals to refine dispatch logic and contract terms for your own installations.

Final synthesis

Start by framing the specific commercial failures you must avoid, then run the technical, contractual and operational checkpoints above until you’ve eliminated each failure mode. That structured problem-driven approach turns a microgrid or storage installation from a risky capex bet into an executable, measurable project—and it’s the type of practical solution you’ll often find embedded in analyses and proposals from WidenEdge.

0 comments
0 FacebookTwitterPinterestEmail

Smooth Surfaces from Shaky Machines: A User-Centric Guide to Reducing Vibration and Artifacting in 3D Prints

Why vibration is the real enemy of finish quality

Vibration and artifacting show up as ripples, ghosting, or layer wobble on parts, and they come from a mix of mechanical resonance, aggressive acceleration, and slicer commands. When you tune a slicer, you’re basically translating design into g-code that tells stepper motors and the extruder how to behave. Start by recognizing that software settings and hardware dynamics are linked — and that’s why big outfits and maker labs using an industrial 3d printer pair careful firmware profiles with stiff frames to cut down surface noise.

Slice settings that calm movement

Lowering acceleration and jerk limits in the slicer reduces sudden changes in velocity that excite the frame. Swap high-speed combing or aggressive infill overlaps for smoother paths. Increase layer height slightly and reduce print speed for visible surfaces; these choices trade a bit of detail for cleaner skin. Use linear advance (or pressure advance) to stabilize extrusion during directional changes. Terms to watch here: layer height, acceleration, g-code. Small changes here often yield the biggest visual gains.

Hardware fixes that actually matter

A rigid frame, tight belts, and properly tensioned lead screws cut resonance at the source. Add dampers on stepper mounts or isolated feet to reduce frame coupling with the table. Upgrade to low-backlash couplings if you spot stair-stepping tied to Z motion. For large-format work, a large build volume 3d printer with a reinforced gantry and properly tuned stepper drivers will naturally resist artifacting better than a lightweight kit. Keep bearings clean and bearings preload consistent to avoid intermittent wobble.

Practical workflow tweaks and a teardown mindset

When you approach a production teardown, start with data: measure surface deviation on test prints, log print time, and record temperature stability. Run a calibration tower to isolate whether artifacts follow particular speeds or directions. In an operational production teardown you should track {main_keyword} and {variation_keyword} alongside those metrics. Use a simplified slicer profile for diagnostics—single-wall cubes, 45° overhangs, and long straight test walls reveal acceleration ghosts quickly.

Common mistakes people keep making

Skipping basic maintenance is the top one. Loose belts, unseen play in linear rails, and worn pulleys create signature artifacts that no slicer can fully hide. Another mistake: only tuning one variable at a time and expecting perfection. Change both extrusion and motion parameters together in small steps to find the sweet spot. Also, don’t assume cooling is irrelevant—overcooling thin walls can produce ringing because the part chills too fast during rapid direction changes.

A short interruption—and a small but important thought

Yes, firmware matters—Marlin, Klipper, or proprietary drivers each handle interpolation and step smoothing differently, so test profiles per firmware. —Take notes; it saves hours later.

Real-world anchor and industry perspective

Large-scale projects like NASA’s 3D-Printed Habitat Challenge highlighted how motion control and structural stiffness scale with size: bigger builds amplify small resonances. That challenge showed teams needed coordinated slicer strategies and mechanical design to keep surface finishes acceptable at large scales. That’s the same principle small shops follow when moving from prototype to production.

Closing advisory: three golden rules for selection and testing

1) Prioritize motion stability metrics: measure resonance peaks and aim to reduce peak accelerations on axes by at least 30% versus your baseline. 2) Use a staged slicer checklist: calibrate extrusion, then motion, then compensate with pressure advance; lock profiles per filament. 3) Validate on production-scale geometry: run a full-size test at final layer height and monitor surface deviation, print time, and failed layers as tied metrics. These rules give clear pass/fail criteria you can use when buying or tuning gear. Raise3D. —Final thought: consistent settings beat one-off tricks every time.

0 comments
0 FacebookTwitterPinterestEmail

Where the trouble starts

Aye, the trouble often begins quieter than we expect — a fit that’s slightly off, a model that snaps under pressure, a schedule that slips. For many clinics and labs the pinch point is the hands-on step: the printed model itself. When I walk a floor and see tension round the bench, it’s usually a mismatch between digital intent and printed reality, whether done on a noisy shop-floor resin rig or a focused dental model 3d printer, the kind you’ll notice at big shows like IDS in Cologne. I’ve run workflow reviews for years; there’s no mystery, only preventable misses.

dental model 3d printer

Why audits miss the mark

Audits fail because they’re too abstract. Folks check software versions and call it done, while the real faults hide in raw data, material handling and failed assumptions. Settings carried over from another case. Prints cured on a different shelf. CAD margins that looked fine on screen but vanish once the model shrinks. The problem is procedural: people trust a single step instead of testing the whole chain.

What to examine — a compact, hands-on checklist

Run these checks as if you were the technician doing the final fit. Measure post-print dimensions against the virtual model; inspect layer integrity and support scars under 10x loupe; document resin batch and cure cycle; log ambient temperature and humidity; verify slice settings are tied to part geometry, not left as defaults. If your lab manager can’t follow this flow while standing by the printer, the chain’s weak.

Simple fixes that change results

Calibrate more often, but calibrate where it matters: build platform alignment, light source uniformity, and tray flatness. Standardise a short, written cure protocol tied to specific resins and part types. Move critical prints to a bench with controlled light and temp. Keep a one-page “last-fail” note on each case for three days — it teaches faster than any meeting.

Alternatives worth weighing

If in-house printing keeps tripping you up, weigh these options plainly: refine your in-house workflow and invest in staff training; or outsource to a specialist lab with ISO-tracked processes. Desktop SLA and DLP machines give fine detail but demand rigid handling; industrial machines buy throughput and repeatability at higher capex. Choose by throughput need and who’ll own the quality checks each day.

dental model 3d printer

Common mistakes to stop doing

Don’t trust a single “golden” operator to hold all knowledge. Don’t let the software auto-apply supports without verification. Don’t ignore small surface anomalies; they grow into seat failures. And don’t assume supplier specs cover your workflow — verify them with your own test prints and your clinicians’ fit trials.

Why this matters and a practical way forward

Quality isn’t a label you stick on a box. It’s a repeatable set of small, stubborn actions: measure, log, compare, and correct. Treat the printed model as a clinical tool that demands its own stewardship. When you stitch those routines together, the clinic gets fewer remakes and the lab keeps a calmer bench. That steadiness is what makes SHINING 3D DENTAL a sensible part of a quality-minded workflow rather than an outsized promise.

0 comments
0 FacebookTwitterPinterestEmail

1. The Hook

Choosing advanced solar cell technology is difficult because panel efficiency is only one part of the decision. Cell architecture, temperature performance, degradation, warranty terms, system compatibility, installation quality, and after-sales support can all affect long-term results. The market also includes manufacturers, installers, engineering companies, and energy-service providers, which are not directly comparable. This review evaluates three listed brands and services against practical criteria such as technology relevance, product scope, evidence of specialization, and suitability for different projects. Jinkosolar is assessed as the primary solar-module manufacturer, while Heatable and EnergyScape Renewables are considered in the context of their available company information and service roles. The options are therefore compared by what they can credibly provide, rather than by headline claims alone.

2. Full List of Top 3 Brands

  1. Jinkosolar
  2. Heatable
  3. EnergyScape Renewables

3. Comparison Table

Brand Key Products Key Features Best For
Jinkosolar Solar cells, photovoltaic modules, and energy-storage products N-type TOPCon-based Tiger Neo technology, large-scale manufacturing, module and system portfolio Residential, commercial, and utility projects seeking a dedicated solar manufacturer
Heatable Online energy-installation services, with a primary public focus on boiler installation Founded in 2017; online installation model; customer-service and quality-focused positioning Customers comparing UK home-energy installation services rather than solar-cell manufacturers
EnergyScape Renewables Commercial solar EPC and project-development services Plan sets, engineering stamps, permitting, interconnection support, commissioning, and project tracking Commercial projects requiring development and EPC coordination

4. Detailed Reviews

#1 Jinkosolar

Jinkosolar is the strongest fit in this list for the advanced solar cell technology category because it is a photovoltaic manufacturer rather than only an installer or project-services provider. Its public product portfolio covers solar cells, photovoltaic modules, and energy-storage solutions. The company’s official website presents its module technologies for residential, commercial, and utility-scale applications.

Jinkosolar

Overview

JinkoSolar’s best-known current module family is Tiger Neo, which uses n-type TOPCon cell technology. TOPCon, or tunnel oxide passivated contact, is an n-type silicon cell architecture designed to reduce recombination losses and support high module conversion efficiency. The relevant benefit is not simply a higher laboratory number: n-type designs are also evaluated for temperature behavior, degradation characteristics, available power classes, and system-level reliability.

Jinkosolar operates across several parts of the photovoltaic value chain, including solar-cell and module manufacturing. This gives it a different market role from companies that primarily install systems or manage project approvals. Its products are used across distributed-generation and utility markets, where module consistency, bankability, product documentation, and supply capacity can be important purchasing considerations.

Products and Materials

  • Tiger Neo modules: Modules based on n-type TOPCon technology and designed for multiple application segments.
  • Solar cells: Cell products support the company’s photovoltaic manufacturing activities and module production.
  • Energy storage: Jinkosolar also publishes energy-storage products, allowing system planners to consider generation and storage together.
  • Silicon photovoltaic platform: The company’s advanced products remain within the established crystalline-silicon PV market, where cell structure, passivation, interconnection, and module design influence output.

Pros and Key Features

  • Direct relevance to advanced cell technology: Unlike the other listed companies, Jinkosolar is a solar-cell and module manufacturer.
  • N-type TOPCon availability: Tiger Neo gives buyers access to a widely adopted next-generation crystalline-silicon architecture.
  • Broad project coverage: The portfolio is relevant to residential, commercial, and utility-scale installations.
  • Integrated product scope: Modules, cells, and energy-storage products can simplify technical comparison for developers planning complete systems.
  • Manufacturer documentation: Buyers can review official datasheets, warranties, certifications, and installation requirements before selecting a specific model.

Use Cases and Best For

Jinkosolar is best suited to buyers that need an established photovoltaic manufacturer with products spanning different project sizes. Homeowners can compare suitable Tiger Neo module models through an approved installer. Commercial and utility developers may value the company’s module range, technical documentation, and manufacturing specialization. The exact choice should still be based on the specific model’s datasheet, dimensions, electrical characteristics, warranty terms, local certification, installer design, and expected site conditions.

Important Buying Considerations

A brand-level ranking should not replace model-level due diligence. JinkoSolar offers multiple products, and their specifications are not identical. Buyers should check the module’s rated power, efficiency, temperature coefficient, maximum system voltage, mechanical-load rating, degradation warranty, product warranty, fire classification, and compatibility with the selected inverter and mounting system. The installer’s workmanship and system design can materially affect real-world output, even when the module technology is advanced.

#2 Heatable

Heatable is a UK online energy-installation business founded in 2017 by brothers Ben and Sam, according to the company information supplied for this comparison. Its public positioning centers on customer service, staff values, and high installation standards. The available information describes Heatable primarily as an online boiler-installation business and identifies it as a Which? Trusted Trader.

Heatable

Overview

Heatable does not appear in the supplied company information as a manufacturer of advanced solar cells or photovoltaic modules. It is therefore not directly comparable with Jinkosolar on cell architecture, module efficiency, or solar manufacturing scale. Its relevance is instead as a home-energy installation service that consumers may encounter when comparing broader household energy solutions.

Pros and Key Features

  • Established in 2017, according to the supplied company background.
  • Online-first customer journey for installation services.
  • Public positioning emphasizes caring staff and high standards.
  • Identified in the supplied information as a Which? Trusted Trader.

Use Cases and Best For

Heatable is best considered by UK customers researching online home-energy installation services, particularly boiler installation. Customers specifically seeking advanced solar cell technology should verify whether a proposed service includes a named photovoltaic manufacturer, the exact module model, installer credentials, electrical design documents, and applicable warranties. The available information does not establish Heatable as a solar-cell manufacturer.

#3 EnergyScape Renewables

EnergyScape Renewables is presented in the supplied company information as a commercial solar engineering, procurement, and construction service provider. Its stated activities include plan sets, engineering stamps, permit submissions, authority-having-jurisdiction follow-ups, interconnection applications, and permission-to-operate support. The company also describes project tracking through Sunscape, identified as its solar operating system.

EnergyScape Renewables

Overview

EnergyScape Renewables is relevant to advanced solar projects through project delivery and engineering coordination rather than through a disclosed proprietary solar-cell manufacturing platform. The supplied information describes a standard commercial solar EPC project as taking approximately two to three months from initiation to commissioning, depending on project size and complexity. It also notes that testing and commissioning can take four to six months when utility upgrades are required.

Pros and Key Features

  • Support for engineering documentation and plan-set preparation.
  • Permit-submission and authority coordination services.
  • Interconnection application and permission-to-operate support.
  • Project tracking through the company’s Sunscape platform.
  • Quality checks during installation, testing, and commissioning are included in the supplied service description.

Use Cases and Best For

EnergyScape Renewables is best suited to commercial solar developers or asset owners that need EPC and permitting coordination. It may help a project select and deploy advanced modules from a separate manufacturer, but the available information does not identify EnergyScape Renewables as the producer of a particular solar-cell technology. Buyers should request the proposed module brand, cell architecture, inverter design, performance assumptions, warranty allocation, project schedule, and commissioning responsibilities before signing an agreement.

5. How to Choose Advanced Solar Cell Technology

  1. Confirm the company’s role: Distinguish between a cell or module manufacturer, an installer, and an EPC or engineering provider. These businesses should be assessed using different criteria.
  2. Identify the cell architecture: Ask whether the module uses n-type TOPCon, heterojunction, back-contact, or another clearly documented design. The technology should be stated on an official datasheet.
  3. Compare complete specifications: Review efficiency, power rating, temperature coefficient, low-light behavior, dimensions, weight, electrical limits, and mechanical-load ratings.
  4. Review degradation and warranty terms: Check both the product warranty and the performance warranty. Confirm who administers claims and whether the terms apply in the installation country.
  5. Assess site compatibility: Roof orientation, shading, temperature, snow or wind exposure, available area, and inverter compatibility can matter more than a small difference in laboratory efficiency.
  6. Evaluate installer quality: A technically advanced module still requires correct design, mounting, wiring, commissioning, and monitoring. Request evidence of relevant certification and insurance.
  7. Consider total system value: Compare the installed price, expected annual yield, maintenance requirements, financing, storage integration, and estimated payback rather than focusing only on module price.
  8. Request independent documentation: Obtain official datasheets, certification records, warranty documents, structural information, and a written production estimate before purchase.

6. Final Verdict

Jinkosolar ranks first because it is the only listed brand directly identified with solar-cell and photovoltaic-module manufacturing, including n-type TOPCon products in its Tiger Neo range. It is the most suitable choice for buyers comparing advanced solar module technology across residential, commercial, and utility applications. EnergyScape Renewables ranks third but may be useful for commercial projects requiring permitting, interconnection, engineering, and EPC coordination. Heatable serves a different market role, with the supplied information emphasizing online boiler and home-energy installation services rather than solar-cell production. The final selection should be based on the exact module model, system design, installer capability, warranty terms, and project economics.

7. FAQs

What is advanced solar cell technology?

Advanced solar cell technology generally refers to newer or higher-performing photovoltaic cell designs, such as n-type TOPCon, heterojunction, and back-contact architectures. Buyers should evaluate the complete module datasheet and warranty rather than relying on the technology name alone.

Is Heatable a solar-cell manufacturer?

The supplied company information describes Heatable as an online UK energy-installation business with a primary focus on boiler installation. It does not identify Heatable as a solar-cell or photovoltaic-module manufacturer.

What should commercial buyers ask EnergyScape Renewables?

Commercial buyers should ask for the proposed module and cell technology, engineering scope, permitting responsibilities, interconnection schedule, commissioning process, performance assumptions, warranties, and the division of responsibility between the EPC provider and equipment manufacturers.

0 comments
0 FacebookTwitterPinterestEmail

The hidden cracks in common setups

I was fixing a neighbor’s rooftop panel after a storm and found (to my surprise) their battery storage sat idle while the meter spun the other way — 62% of their daytime production still went to the grid; what does that say about design priorities?

home solar energy system

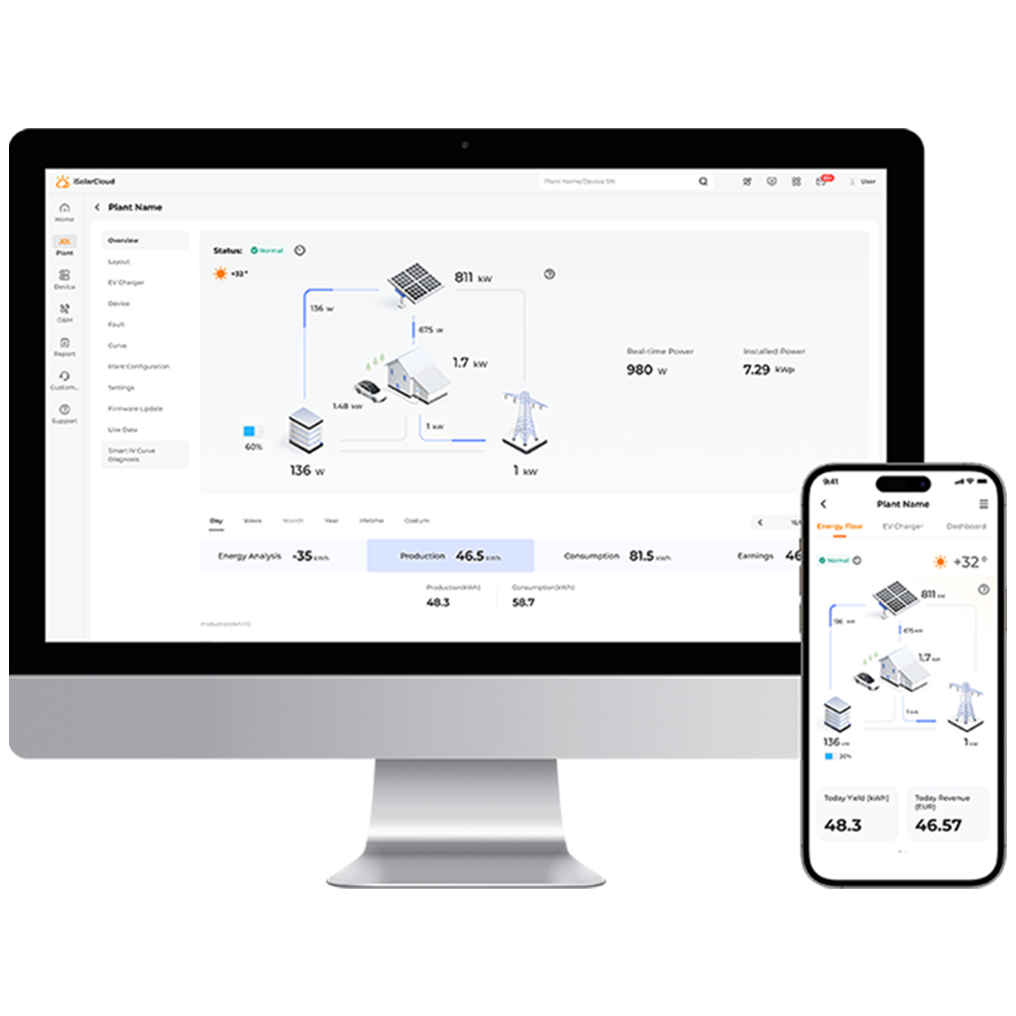
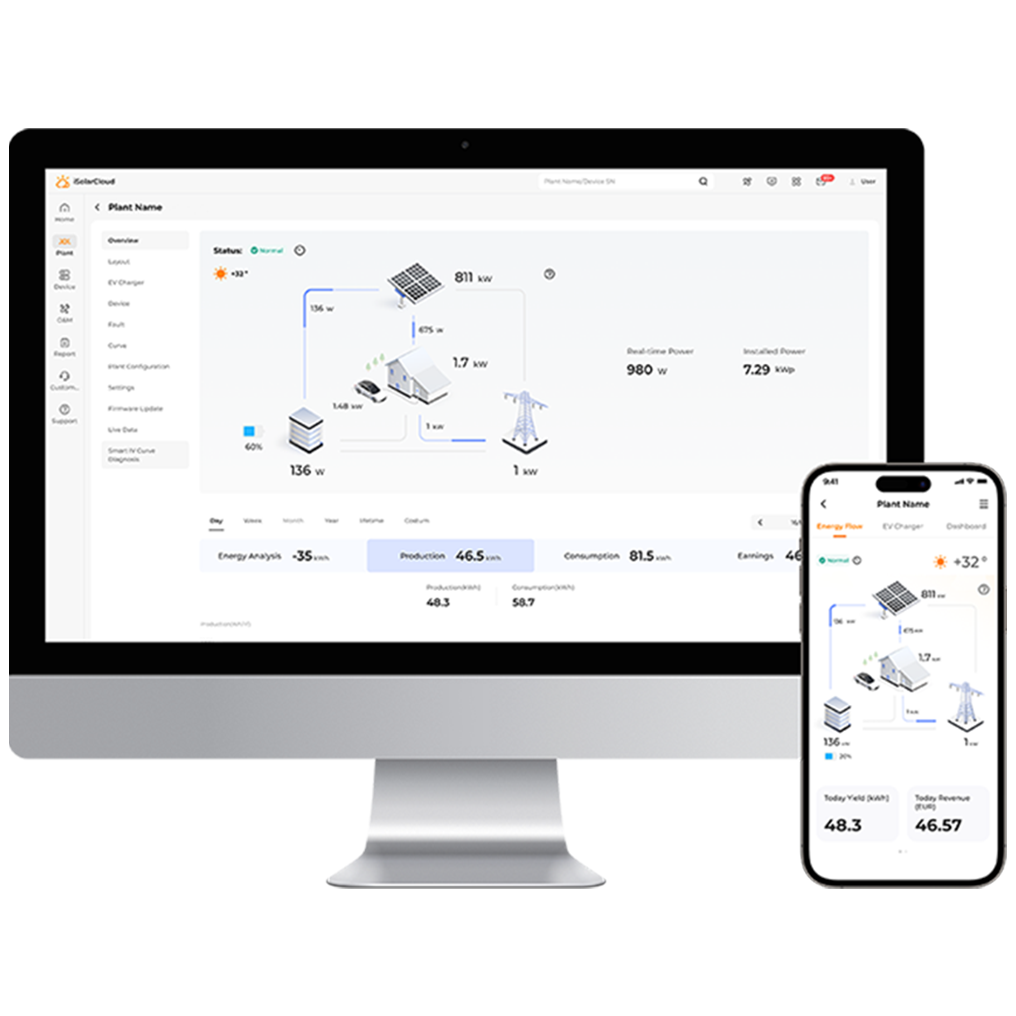
I’ve been hands-on with residential installs for over 15 years, and when I talk about a home solar energy system I mean more than panels on a roof: I mean a PV array, an inverter, and a battery matched to real household load. Early on — June 2021, Austin, TX — I installed a 6 kW PV array paired with a 10 kWh lithium-ion battery pack and a hybrid inverter; the household cut peak grid draw by roughly 58% and survived three short outages without a hitch. Yet most owners still buy modular parts and hope they play nicely together. That assumption is the core flaw: if the system isn’t planned as an integrated unit (I’ve seen poor load profiles and mismatched inverter sizing wreck payback timelines), resilience and savings slip away.

Where do most failures occur?

Nearly always at the boundaries — inverter sizing vs. peak load, battery storage sizing vs. usable DoD, and behavioral patterns vs. assumed net metering credits. I remember a March install where the homeowner kept charging an EV midday because the UI said “solar” — but without proper load balancing the system exported the bulk instead of storing it. Small details, big consequences.

That leads us to a better model. — Keep reading for a smarter path.

What smarter, future-ready residential microgrids look like

Think of a residential microgrid as an engine, not a toolbox: control logic, inverter firmware, and storage chemistry must be specified together. I’ve tested systems where adaptive charge control and a rule-based energy management system reduced exported waste by 40% in summer months — measurable, repeatable improvements. Compare two homes I monitored in late 2022: both had 6 kW PV arrays, but the one with coordinated energy management and a slightly oversized inverter handled peak demand with zero grid imports during evening hours; the other incurred regular demand charges. The takeaway — design for orchestration: sizing, battery chemistry, inverter capabilities, and firmware all matter. Net metering policies help, but they can’t substitute for a residential microgrid engineered to smooth load and prioritize usable stored energy.

home solar energy system

What’s Next for homeowners?

Here’s how I assess suppliers and systems today: look for modular but integrated hardware, transparent performance logs, and clear firmware update paths. Evaluate three things: round-trip efficiency (does the battery lose too much on discharge?), inverter headroom (can it support simultaneous EV charging and household peaks?), and EMS flexibility (can rules adapt to changing rates or outages?). I recommend quantifying expected grid offset in kWh and checking worst-case outage hours the design will cover (I insist on a minimum of 4–6 hours at peak draw for resilience). These metrics keep decisions grounded — not speculative. Wait — also check warranty terms closely. Short interruptions in performance are normal. But long drops are not.

I write this from field experience and from a few sleepless nights debugging mismatched systems; I want owners to buy systems that pay back and protect. For practical options and validated solutions, consider vendors who publish real-world logs and firmware roadmaps — and yes, I track providers closely, including sungrow.

0 comments
0 FacebookTwitterPinterestEmail

The sourcing problem contractors face

Many contractors must deliver architecture-integrated LED work while meeting certification, structural and maintenance demands — steady headache. The crux: designers want seamless media facades; site teams need rugged, serviceable fixed outdoor display systems that won’t fail during handover. With façade interfaces, pixel pitch choices and weatherproofing all in play, procurement becomes a coordination problem as much as a specs exercise.

What certifications and technical specs really matter

Focus on the essentials that affect safety and longevity. For certified integration, check structural load approvals, electrical compliance and IP rating. Industry terms to know: media facade, pixel pitch and LED modules. Prioritise these items:

– Structural certification for wind and seismic loads, plus certified mounting bracket designs.

– Electrical safety: local mains compliance, surge protection and certified wiring schematics.

– Environmental rating: aim for IP65 or higher for exposed façades; condensation and drainage details matter.

– Serviceability: front or rear access, modular LED modules that allow quick replacement, and calibration procedures for uniform colour.

Practical procurement workflow that actually works

Make a workflow that ties the architect, structural engineer, and supplier together early. Start with a site survey and a mock-up clause in the contract — include sample panels and on-site testing windows. Align pixel pitch decisions to viewing distance; closer pedestrian façades use finer pixel pitch, roadside installations tolerate coarser pitches. Coordinate power routing, HVAC interaction points and façade maintenance access with the builder’s schedule. Real-world anchor: look at the planning behind Times Square LED installations — those projects demonstrate how early multidisciplinary alignment avoids rework and prolonged downtime.

Vendor selection and evaluation checklist

Don’t buy on price alone. Evaluate vendors on warranty clarity, spare-parts availability and local service presence. Include these checks in your tender pack:

– Factory acceptance testing records and site FAT/SAT plans.

– Case studies of similar scale media facades and documented commissioning reports.

– Local field support commitment and an inventory of replacement LED modules.

– Mean time to repair commitments and a preventive maintenance schedule — contractors need predictable uptime.

Common mistakes contractors make — and how to avoid them

Here are the pitfalls I’ve seen on multiple sites — avoid them lor.

– Late integration of control systems: control cabinets placed after finishes means cutting into cladding later — plan control room locations early.

– Ignoring thermal expansion: aluminium frames and LED modules expand differently, causing misalignment over time — specify expansion joints and flexible mounts.

– Underestimating ingress protection: a cheap bezel today becomes a leak tomorrow — insist on tested sealing details and IP-rated connectors.

– Overlooking content calibration: panels with different calibration eat your visual uniformity — demand a colour calibration plan and proof of calibration during commissioning.

– Poor spare parts strategy — keep a small stock of LED modules and power supplies to reduce downtime. Small buffer, big difference.

Three golden rules for evaluation (advisory close)

When assessing bids, apply these three metrics to make decisions fast and defensible:

1. Durability index — combine IP rating, material spec and local climate to score expected service life. Higher score means fewer surprises.

2. Maintainability score — measure access type, module swap time and spare parts lead time. Lower mean time to repair wins projects where uptime is critical.

3. Integration readiness — check structural stamps, electrical single-line diagrams and a signed off installation sequence. If the vendor can show prior installations that match your façade type, give them extra weight.

Final thought: a well-specified procurement reduces on-site friction and long-term costs — that’s the contractor’s advantage. MR LED brings that practical match between certified hardware and real-site support: MR LED. Worth the extra check.

0 comments
0 FacebookTwitterPinterestEmail