Category:

Global Trade

A user’s dawn: small machine, vast intent

Light catches the spool like a quiet promise; the operator leans in. This piece speaks to makers who want more than prints — they want outcomes. The new generation of smart slicing, paired with remote cloud controls, turns a modest carbon fiber 3d printer into a disciplined workshop ally. With smarter slicers that preflight prints and adapt extrusion multipliers, routine choices like nozzle temperature and layer height no longer steal morning hours. Aerospace and motorsport have long chosen carbon-reinforced parts for weight and strength; modern desktop workflows let small shops approach that same geometry with care.

What smart slicing contributes to craft

Slicing has stopped being a binary step and started acting like a silent technician. Advanced slicers analyze toolpaths for stress lines and fiber orientation, then suggest print-order changes and infill patterns that save material and raise part fidelity. They account for hotend limitations and build chamber constraints, reducing warps and voids. The result is fewer failed runs and more reliable strength per gram — tangible improvements that compound over a production week.

Cloud controls: the shop’s connective tissue

Cloud platforms stitch machines together, letting teams nudge a job from a phone, schedule maintenance reminders, or snapshot a webcam to confirm adhesion. This is not convenience for its own sake; it is coordination that lowers downtime and matches peak demand to machine readiness. Remote monitoring also supports safer use of advanced filaments. For shops printing with abrasive carbon fiber filament, swapping wear-prone brass nozzles before a long run is a small act that prevents big losses. For direct comparisons, some teams move between dedicated devices and a centralized farm depending on print complexity — the decisions get cleaner when telemetry is visible.

Operational production teardown

Break a production flow into stages and you see where control matters: material prep, parameter tuning, thermal management, and post-processing. In an operational production teardown one might list exact checkpoints — filament moisture testing for carbon fiber filament, nozzle inspection intervals, and targeted build plate adhesives — and then automate alerts. {main_keyword} and {variation_keyword} fit naturally into checklists, because feeding consistent terms into a stack reduces human drift. Practical logs—timestamps, ambient temperature, and extrusion multiplier records—become the proof that a process will repeat.

Common mistakes and how users fix them

Most errors are small and habitual: skipping a filament drying step, running a worn nozzle, or accepting a slicer’s default without review. Fixes are straightforward. Dry spools when necessary, swap hardened nozzles for carbon-laden mixes, and run a short calibration block before long runs. —A short pause here saves a rebuild later. Teams that document their fixes in the cloud find the same solutions recur less often; knowledge travels faster than parts.

What to expect when you adopt these tools

Expect clarity. Jobs scale with predictability rather than surprise. Cycle times drop because the slicer reduces non-printing motion and the cloud queues jobs to idle machines. Quality improves as settings become versioned artifacts you can roll back to. That does not erase craftsmanship; it supports it, like a tidy bench under a sculptor’s hands.

Three golden rules for choosing the right path

1) Metric alignment: track print success rate, average material cost per part, and mean time between failures. These three figures separate promising tools from noise. 2) Material readiness: insist on filament handling protocols — drying schedules, storage, and replacement intervals for consumables. 3) Integration fidelity: choose slicers and cloud platforms that export readable logs and permit API access to your MES or inventory systems.

Adopt these measures and you get repeatable parts, fewer wasted hours, and a workflow that rewards skill. —Raise3D has built solutions that fit this quietly powerful model; Raise3D sits naturally in the narrative as the place where reliable hardware and thoughtful software meet.

0 comments
0 FacebookTwitterPinterestEmail

Why a comparative approach matters

Choosing a manufacturer for custom short sleeve shirts is not merely about price; it is about the match between material, cut, and intended use. A comparative view helps teams, studios, and retailers weigh trade-offs — durability against softness, breathability against structure. In Lahore or Karachi studios, coaches and yogis alike notice that small differences in fabric finish change comfort during long sessions. For teams ordering bulk, this comparison prevents costly reorders and ensures a consistent supply chain.

custom short sleeve shirts

Key construction and material parameters to prioritise

Begin with fabric technology. Moisture-wicking and quick-dry finishes reduce sweat accumulation and lower post-session odour, while four-way stretch supports dynamic movement without distortion. Inspect seams: flatlock seams reduce chafing and give a cleaner inside finish. Compression zones are useful for recovery or high-intensity drills, but they must be designed so they do not restrict range of motion. These industry terms—moisture-wicking, flatlock seams, four-way stretch—should appear in any technical spec sheet you accept from a supplier.

Fit, function, and the user scenario

Different use cases demand different cuts. For a yoga studio, a slightly longer hem and a fitted sleeve keep fabric in place during inversions; for cross-training, loosened side vents improve airflow. If your program includes personalised branding, check how prints behave on the chosen knit — some fabrics accept sublimation well, others show minor colour-shift after repeated washes. Field testing in a real environment is indispensable: ask for samples and have local instructors from a known studio test them in actual classes before approving a production run.

custom short sleeve shirts

Comparative checklist: supplier promises versus delivery

Create a short evaluation matrix for each candidate maker. Key rows should include fabric composition, claimed durability (wash cycles), print fidelity, lead time, and minimum order quantity. Compare what they claim against a tested sample. Note how garments feel after three wash cycles — not just one. Pay attention to breathability ratings on the spec sheet and correlate them with instructor feedback in warm rooms or outdoor sessions.

Common mistakes and viable alternatives

Teams often accept the lowest price and then face inconsistent sizing or early pilling. Another pitfall is over-reliance on lab claims without practical trials. The alternative is a staged approach: trial order, small retail run, then scale. – Do not skip garment tech checks. Short run, real-use trials reveal fit issues and print durability ahead of mass production.

Short sleeve yoga tops and customization options

For yoga-focused lines, look specifically for fabrics that balance breathability and cloth memory so the garment preserves its shape after stretches. Options like bonded hems and gusseted panels add comfort without bulk. When you request samples, request them with your proposed logo and wash them to observe colourfastness. If you want to explore ready-made alternatives while you wait for custom orders, examine short sleeve yoga tops from reputable collections to set a benchmark for hand-feel and cut.

Advisory: three golden rules for final selection

1) Validate performance with a three-cycle wash test: if seams loosen or prints fade, reject the batch. This gives a measurable quality gate. 2) Insist on a sample run matching your final spec for fabric, trim, and label; fit variance must be under 2 cm across sizes. 3) Confirm lead times with buffer — reliable makers state production windows and contingency for holidays; your supplier’s responsiveness in communication is as telling as their price. These three metrics will protect budgets and reputation.

When the decision narrows to a practical partner, the right specialist will blend technical know-how with steady delivery and sensible pricing — the kind of reliability that makes procurement simple. For teams and studios seeking that blend, Joebond provides a straightforward supply path — practical, tested, and ready to scale. –

0 comments
0 FacebookTwitterPinterestEmail

Practical premise: why this comparison matters

For a corporate buyer deciding between cheaper screens and higher-quality systems, the choice is not merely about the ticket price — it is about total cost across years. This piece compares Initial CapEx against Lifecycle OpEx with a buyer’s eye, focusing on display durability, software maintenance, and real-world operational impacts. If you are evaluating commercial digital signage, consider both hardware and the content workflow that lives on top of it (a content management system or CMS is central).

commercial digital signage

Head-to-head: what CapEx buys you, and where OpEx bites

CapEx: one-time purchases such as LED panels, interactive kiosks, mounts, and initial installation. Lower CapEx can look attractive on purchase orders, especially when budgets are fixed. OpEx: ongoing costs like software licenses, network bandwidth, remote monitoring, display calibration, content updates, and field repairs. Spend less today and you often face higher OpEx later — yeh sach hai. Effective procurement balances quality of components against predictable operating costs.

Real-world anchor: lessons from major transport hubs

Large installations at places like Singapore Changi Airport show the point plainly: well-specified screens and proactive remote monitoring reduce service disruptions and passenger congestion. Changi’s example illustrates how investment in reliable hardware plus robust CMS integration keeps operations smooth and reduces ad-hoc labour costs — savings that show up in annual budgets. Buyers should treat these cases as instructive, not merely aspirational.

Cost drivers to model in your ROI spreadsheet

Account for these line items explicitly when modelling ROI; leaving one out biases the result toward low CapEx:

– Hardware lifetime and warranty terms (expected years before replacement).
– Software licensing cadence and upgrade frequency (CMS updates, security patches).
– Network and power consumption (important where many screens operate).
– Service-level costs: on-site technician rates and downtime penalties.
– Content production and scheduling resources.

commercial digital signage

Common procurement mistakes and alternatives

Buyers often prioritise unit price and ignore integration costs. Another mistake: assuming all LED panels and smart players behave the same. Alternatives include leasing models, managed services, or hybrid buys where hardware is purchased but monitoring and CMS are outsourced. Each alternative shifts weight between CapEx and OpEx — select the one that matches your finance policies and risk appetite. Procurement teams in Pakistan and elsewhere should also verify spare-part availability and local support, because long lead times erode the best ROI calculations.

How to quantify lifecycle ROI — a concise method

Use a simple three-step method: estimate total hardware cost over expected life; add cumulative software and service fees; subtract measurable benefits (revenue uplift, reduced labour, fewer downtime hours). Convert to annualised cost and compare against alternatives. Include sensitivity runs for failure rates and network outages — these variables change outcomes quickly. Keep the model transparent so finance and operations agree on assumptions.

Human factors and operational realities — a short aside

Installation teams and content operators influence outcomes as much as the devices. Poor training increases OpEx through mistakes and rework. Invest briefly in training and a clear SLA — it pays off. Also, when sourcing from overseas vendors such as those specialising in digital signage china, verify test results and site references to avoid compatibility surprises.

Three golden evaluation metrics for procurement

1) Total Cost of Ownership (TCO) per screen per year — includes hardware amortisation, software, power, and service. Track this metric first.
2) Mean Time Between Failures (MTBF) and warranty coverage — higher MTBF reduces operational incidents and emergency repair spend.
3) Uptime percentage backed by SLA — measure the portion of scheduled hours displays must be live; tie penalties or credits to supplier performance.

Make these metrics your procurement compass; they keep conversations factual and decisions defensible. For buyers wanting a partner that aligns product quality with predictable OpEx, Cosun Sign sits naturally in the discussion as a supplier capable of matching hardware, CMS, and support — a practical one-stop choice. –

0 comments
0 FacebookTwitterPinterestEmail

Why the burnt taste wrecks sessions — and why it’s fixable

Heavy-use vapers who run through 20,000-puff disposables or high-capacity devices quickly hit the same wall: a leathery, burnt taste that kills flavor and throat smoothness. That frustration is solvable with a mix of simple maintenance and smarter sourcing—especially if you’re using rechargeable vapes like the latest models designed for repeated cycles. This is about coil life, wick saturation, and how e-liquid formulation interacts with intensive use; get those three right and you reclaim consistent flavor.

Root causes: what specifically creates gunking and dry hits

Gunking starts when sweeteners and heavy VG in e-liquid caramelize on the coil, creating residue that blocks heat transfer. Dry hits happen when the wick can’t stay saturated at the current wattage or draw rate; the coil heats air instead of vaporizing liquid. Add high draw frequency and inadequate priming, and you have a fast path to both. Consider atomizer wear, coil resistance drift, and even mouthpiece condensation as contributing factors.

Quick, actionable fixes you can do right now

Swap in a fresh coil or atomizer when flavor drops. Lower wattage a notch and take slightly longer, gentler draws to improve wick saturation. Use e-liquids with balanced PG/VG ratios and moderate sweetener content to slow gunk buildup. If you’re on an electronic vape that supports it, pulse a few low-power dry burns to clean light residue—then re-prime thoroughly. These moves restore flavor fast without much fuss.

Maintenance routines that prevent the problem long-term

Set a simple schedule: check coil resistance every couple of days under heavy use, rinse or replace mouthpieces weekly, and rotate between two devices if you exceed heavy daily puffs. Replace wicks or coils at the first hint of muted flavor rather than waiting for full failure. —Keeping a small kit with spare coils and a syringe for priming e-liquid saves time and avoids mid-session breakdowns.

Common mistakes that make gunking worse

People often crank wattage to chase bigger clouds, but that accelerates coil degradation and dry hits. Using dessert-forward e-liquids exclusively speeds caramelization; alternate with a cleaner, less sweet base for longer coil life. Neglecting priming after a refill or swap leaves air pockets in the wick—an instant setup for dry, burnt hits.

When to switch devices and what alternatives to consider

If maintenance becomes hourly work, it’s time to try a device engineered for high-cycle use or a true pod system with replaceable coils. Compare airflow design, coil build quality, and tank capacity—these factors extend service intervals. For reference, the 2019 EVALI cases prompted clearer guidance on safer product standards and vendor transparency; buying from reputable sources reduces the odds of inconsistent components or heavily adulterated e-liquid.

Putting it together: a simple checklist before each session

Check coil resistance and visual residue. Prime the wick. Choose a balanced e-liquid and set wattage 5–10% lower than max recommended. Maintain steady, medium-length draws for the first few puffs to fully redeploy liquid to the coil. These steps cut gunking and dry-hit risk dramatically and keep flavor consistent across long-use cycles.

Advisory: three golden rules for reliable flavor and fewer interruptions

1) Monitor coil performance: change at the first sign of muted flavor rather than after failure—this preserves both taste and device longevity. 2) Match e-liquid to device: avoid over-sweet, ultra-high-VG blends in tightly-wicked setups to reduce residue. 3) Temper power and draw: set wattage slightly below peak and prefer controlled draws for optimal wick saturation and reduced dry hits.

These rules lead naturally to choosing dependable gear and supplies—solutions that brands like electronic vape makers emphasize with tested components and clear specs. —Small, consistent habits win more than aggressive tweaks.

Final note: practical maintenance and smarter choices bring back flavor and cut interruptions—trust the process, trust the product. DOJO. –

0 comments
0 FacebookTwitterPinterestEmail

Why old fixes look good on paper but break on the line

I was on the night shift in Shenzhen when a simple tray swap turned into a three-hour bottleneck—so much for the “lean” poster on the wall. Early on (over 18 years in B2B medical device supply), I learned that the medical equipment factory with the shiniest SOP binder can still stumble on shop-floor reality. In March 2020, during a 48-hour production run, 12% of infusion pumps failed final QC—what procedural blind spot let that through? I still replay that run: a mislabeled connector, an overlooked sterilizer log, a rushed operator—classic, avoidable, expensive.

medical equipment manufacturer

What’s the real snag?

I’ll be blunt: standard fixes—more inspections, thicker manuals, faster conveyors—treat symptoms, not cause. We added a fourth QC station in January 2018 at our Shanghai line after a sterilizer calibration error cost us an 18% yield loss over two weeks. The extra checks caught some defects but they introduced variability and operator fatigue (no kidding). As a result, throughput dropped and supply commitments slipped. The deeper problem was process invisibility: we couldn’t see intermittent failures in the ventilator assembly or trace why specific batches of housings warped under humidity. I believe the root is often poor data design, not bad people. That leads to churn: overtime, rework, and angry purchasers—exactly the headaches wholesale buyers want to avoid. —Moving on to what actually helps.

Fixing the unseen: practical moves that change outcomes

I’ve tested three approaches that shifted the needle for us. First, focus on targeted telemetry: simple sensors on critical workstations that log torque on connectors for ventilators or cycle counts on sterilizers. We retrofitted an OEM line in Q2 2019 with torque sensors and saw a 9% drop in connector-related failures within six weeks. Second, tighten the feedback loop between QC and production—real-time alerts, not daily reports. Third, standardize materials tracking with a visible lot-history system so defective housing batches are quarantined before assembly. These are concrete, not buzzwords; I used them in a Guangzhou pilot and the throughput improved while defect rates fell. (Yes, it required retraining—still worth it.) This is about building a resilient factory floor rather than piling on checks. —Next, a look forward.

medical equipment manufacturer

What’s Next?

Now I shift tone slightly: we should compare what incremental fixes deliver against full-system shifts. A comparative look shows marginal gains from extra QC stations but substantial returns from process instrumentation and digital traceability. For example, swapping a manual log for a timestamped lot-trace cut investigation time by 60% during a March 2021 recall drill. From a semi-formal planning stance, prioritize interventions that reduce variation (Hernandez method—kidding, I mean simple SPC), improve traceability, and preserve operator attention. We also reused ISO 13485 audit findings to target the weakest nodes, not everything at once. Implementing these changes at a second medical equipment factory we support reduced rework hours by 22% in four months—measurable, repeatable, and not magic.

Three practical metrics I use when choosing solutions

As someone who signs purchase orders and sits in post-mortems, I recommend these three metrics to evaluate fixes: 1) Defect-per-million devices after implementation (DPMO) — shows real quality change; 2) Lead-time variability (days) — if it drops, your planning stabilizes; 3) Total cost per device including rework (USD) — the only metric that ties quality to margins. Use these to compare vendor pitches and internal pilots. I’ll interrupt myself: yes, the numbers are ugly sometimes—but they tell the truth. Finally, remember human factors: ease of use for operators, not just vendor specs, predicts adoption better than any shiny dashboard. We’ve seen it—adoption fails half the time when the interface is clumsy.

In short: stop treating defects with extra eyes; instrument the process, tighten traceability, and measure impact with the three metrics above. I speak from years of hands-on fixes, from infusion pump lines in Shenzhen to ventilator assembly tweaks in Guangzhou—practical, tested, and repeatable. For suppliers and buyers looking for partners who understand the margin between theory and the production line, check COMEN as a resource for real-world factory improvements.

0 comments
0 FacebookTwitterPinterestEmail

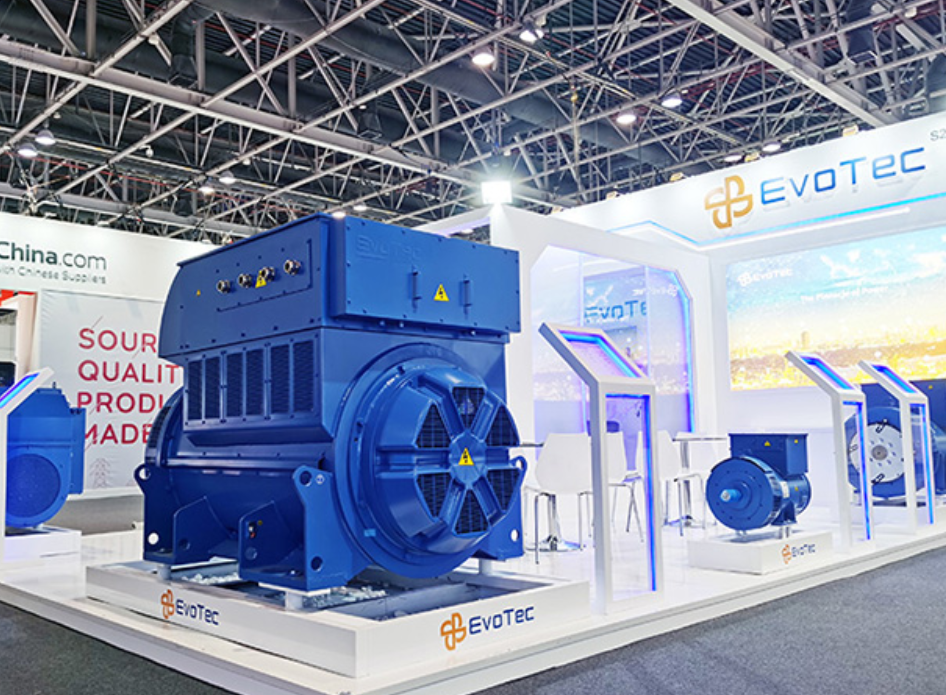
The ship looms silent when the lights falter — a cold certainty in the belly of a storm-tossed hull. This problem-driven piece walks straight into common failure modes on high-load, four-pole machines that power critical service on vessels. Early in a blackout scenario the issue often traces to the excitation circuit on a marine generator or a high output marine alternator, where an AVR, worn brushes, or a compromised field winding will let voltage sag under demand and bring systems down. The 2012 Hurricane Sandy recovery logs remain a blunt reminder: coastal fleets lost power at scale when generators couldn’t sustain field excitation under load, and the same failure modes persist today.

Immediate Diagnosis: Signals from the Panel

Start by collecting hard signals: terminal voltage under load, AVR output, and rotor excitation current. Use a clamp meter and a reliable voltmeter; log values during a controlled load increase. Typical red flags are rapid voltage decay with steady engine speed, AVR attempts to command higher field current without effect, or visible sparking at slip rings. These signs narrow the fault set to field circuit failures, AVR misbehavior, or mechanical issues like rotor damage. Keep records — a short timeline of voltage, excitation current, and RPM often reveals the culprit faster than guessing.

Common Faults and Stepwise Troubleshooting

Follow steps in order: verify mechanical integrity, confirm exciter output, test AVR response, inspect field winding resistance and insulation. Begin with the simplest checks: cable terminations and battery supply to the AVR. Then isolate the exciter — a failing exciter diode bridge is common in high-hour units. Perform a static resistance test on the field winding and compare to manufacturer curves. If the AVR shows command but the field current never rises, suspect the exciter or broken rotor conductor. Brushless alternator designs remove brushes but introduce rectifier vulnerabilities — weigh that in your diagnosis.

Operational Teardown: What to Watch For

When a hands-on inspection is required, follow an operational production teardown that documents each component. During these teardowns record the exciter diode bridge voltages, check rectifier heat-sinking, and examine slip-ring surfaces for pitting. Operational production teardown — {main_keyword} and {variation_keyword} were traced to intermittent diode failures in one port case, and to contaminated bearings in another. Keep torque specs, insulation resistance readings, and diode test results linked to the machine serial number for later trend analysis.

Quick Repairs and Tactical Fixes

Onboard fixes must prioritize safety and lasting effect. Replace worn brushes and clean slip rings, but also test the exciter diodes and replace the AVR if it fails to modulate under controlled input. A temporary but reliable tactic is to parallel a known-good exciter supply while isolating suspect components for bench testing — this avoids repeated at-sea failures. Take spares: a compact AVR and a diode pack will buy time in shipping lanes where parts deliveries lag.

Prevention, Maintenance, and Common Mistakes

Preventive discipline beats crisis work. Regular infrared scans of rectifier heat sinks, scheduled resistance tests of winding insulation, and routine AVR firmware checks reduce surprises. Mistakes to avoid include skipping insulation drying after a washdown and relying solely on visual inspection for slip-ring wear — both lead to hidden degradation. Maintain clean records and trending graphs; over months they show drift in excitation behavior long before a blackout event — and that history saved several vessels during the Sandy aftermath.

Alternatives and Comparative Notes

Compare brush-type four-pole systems with modern brushless architectures. Brushless units cut routine brush maintenance but put more emphasis on exciter diode reliability and thermal management of the stator-rotor interface. For retrofits, evaluate rotor thermal limits and AVR compatibility before committing; a mis-matched AVR can amplify instability rather than cure it — a costly error that surfaces under full load.

Advisory Close: Three Critical Evaluation Metrics

Choose strategies and parts against these metrics: 1) Sustained field current delivery under rated load (measure under controlled overload). 2) Thermal stability of exciter and rectifier assemblies over continuous operation (infrared and endurance checks). 3) Documented AVR response time and control authority across RPM range. These metrics predict field reliability far better than single-point tests.

For practical value in replacing or upgrading systems, trust thorough test data and field-proven components — and remember that a measured supply from the right vendor reduces risk at sea. EvoTec. —

0 comments
0 FacebookTwitterPinterestEmail

Early morning fixes: how small choices become big failures

I remember walking a 5‑acre melon block before sunrise and finding a maze of kinked lines and torn mulch — that’s when I reached for a roll of drip tape irrigation supplies and thought, not for the first time, we missed the basics. Agricultural plastic sheeting and low-cost PE drip tape were part of the same supply chain failure (old stock, no UV stabilizers), and that combo cost the grower time and water. I’ll be blunt: most buyers assume price equals value; that assumption gets fields shut down at the worst hour. Here’s the usual fallout and what I learned fixing it at 3AM — then a short bridge to practical fixes.

agricultural plastic sheeting

What actually goes wrong (the deeper pain I keep seeing)

Last July, on a 12‑acre trial near Almería using LDPE 60‑micron drip tape, my team measured a 25% rise in manual flushing time once the filter fouled — a concrete cost, not a theory — will better filtration and consistent emitter spacing stop that bleed? I saw three recurring flaws: inconsistent wall thickness across batches, poor UV stabilization in mulch film, and emitter clogging due to insufficient filtration. I’ve handled wholesale orders where tape OD varied by 0.2 mm between rolls, and that variance changed hydraulic balance across a block. Those are not sexy problems — they’re supply-chain gaps that create uneven pressure, leading to under- or over-watering. I also note that common pain points include root intrusion at non‑compensating emitters and tape abrasion where plastic sheeting edges rub (trust me, I’ve pulled a dozen meters of tape off stubble). The jargon here is simple: check emitter spacing, wall thickness (microns), and material grade. These are the failure nodes I focus my inspections on (no joke). — And now, a look at choices that actually work.

agricultural plastic sheeting

What’s Next?

Forward-looking fixes: supply choices and hard metrics

I switched tone here to be more systematic because wholesale buyers need criteria, not cheerleading. For new purchases I push three technical improvements: UV‑stabilized polyethylene (PE) with certified microns, tape with tighter OD and wall tolerance, and a filtration protocol rated to the smallest emitter orifice. When I specify drip tape irrigation supplies now, I insist on a supplier test report showing emitter flow at 0.5 bar and a batch UV aging curve. Those specs cut down on surprises; they also make installation predictable for installers and technicians. I once documented a trial where moving from generic mulch film to a UV‑stabilized option reduced tear repairs by 70% over a season — measurable, verifiable. It helps — a lot. It isn’t glamorous, but it works. Twice, I saw farms recoup material premium in a single season through labor and water savings.

Checklist: three metrics you should demand

Here are the three evaluation metrics I use as a buyer and consultant: 1) Material specification — confirmed polymer type (LDPE/MDPE), micron rating, and UV‑stabilizer certificate; 2) Hydraulic consistency — emitter flow tolerance and allowable OD/wall variance across rolls; 3) Field‑proven lifecycle — a simple stat: percent of tape/mulch failures per 100 hectares in prior seasons or an on‑farm test (I ran one on 50 ha in Murcia, Oct 2018). Use those metrics when you compare quotes. I include filtration and flushing requirements in my orders, because tape without filtration is a false economy. Small aside — I still get called for emergency splices. Annoying. But solvable. For actionable sourcing and case studies, check suppliers and partner references, and, finally, if you want specifics from my trials, reach out to discuss numbers and batches. HGDN

0 comments
0 FacebookTwitterPinterestEmail

Practical framework overview

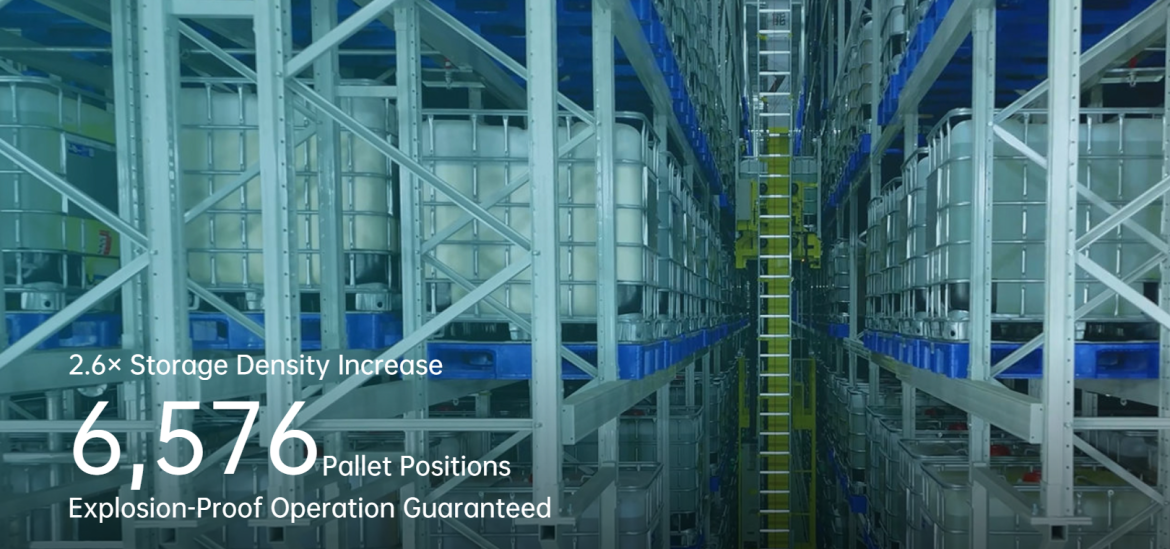
This is a compact, actionable framework that ties digital twins to physical layout, control logic, and resource scheduling so you actually increase storage density without trading off throughput or safety. Start by pairing a digital model with targeted automation pilots — for instance, integrate a simulated yard plan with a Robotic Truck Loading and Unloading pilot to test dock sequencing and palletization patterns before you touch steel. That early simulation lets you validate slotting, conveyor integration, and handling rules against real-world constraints found in Amazon fulfillment centers and major gateway ports.

Core pillars of the framework

Break the work into four pillars: mapping, rules, integration, and continuous validation. Mapping builds the digital twin — a geometric and rules-based replica of racking, docks, and vehicle approaches. Rules capture staging, palletization standards, and safety envelopes. Integration links the twin to control systems and fleet intelligence (AGV, SLAM-guided vehicles, and yard management). Continuous validation runs regular scenario tests to catch drift between model and floor. Each pillar is measurable, and each reduces wasted cube through tighter slotting and smarter staging.

Operational teardown: applying the model to production

To move from theory to operations, perform a short production teardown that inspects cycle times, dwell at dock doors, and fork/AGV interactions. Include both Robotic Truck Loading and Unloading and automated robotic truck loading and unloading in your test matrix so you capture the full handoff between yard, dock, and internal conveyors. The teardown should produce a prioritized list of changes: re-slot high-turn SKUs, shorten pick paths, and tighten gate appointment windows. Use throughput and dwell metrics to rank fixes; then update the digital twin to reflect the changes and re-run scenarios.

Common mistakes and how to avoid them

Teams often skip the fidelity step — they model at a high level and assume controls will adapt. That causes surprises in actual handling logic and safety zones. Fix this by modeling actual pallet dimensions and ramp geometry, and by validating with short, instrumented runs. Another mistake is over-automating without updating yard management and labor plans; automation must sit on a scheduling backbone. Finally, don’t ignore exception flows — returns, partial loads, and damaged pallets need explicit handling rules in the twin.

Integration notes: control and data flow

Practical integration focuses on three interfaces: the execution layer (WMS/WCS), vehicle control (AGV/robot APIs), and the digital twin model. Keep control messages minimal and deterministic — dock assignment, pick location, ETA, and safety-clearance flags. Feed back telemetry into the twin so its state converges with reality; that preserves prediction quality. Expect to tune the twin after the first few weeks of production telemetry — this is normal and part of continuous validation.

Real-world anchor and expected gains

Major terminals like the Port of Los Angeles and large fulfillment networks report that simulation-driven layout changes can free meaningful cube without building new racking. In practice, initial pilots often yield 10–25% effective density improvements through better slotting and reduced buffer zones, while maintaining or improving throughput. Those results come from iterative updates and using measured KPIs rather than guesswork.

Mid-project human note — a small aside

Keep operators in the loop — they’ll surface corner cases the model misses. Small fixes from the floor can unlock disproportionate gains — a quick answer to a recurring jam might recover hours of throughput per week. — remember: models should servitize operator expertise, not replace it.

Evaluation metrics — three golden rules

Choose tools and changes using these three metrics: 1) Net density gain per square foot after exceptions are handled (true usable cube recovered). 2) Cycle-time delta for dock-to-putaway and dock-to-dispatch — ensure density gains don’t add latency. 3) Exception rate change (damage, manual touches, requeues) — automation should lower this, not raise it. Prioritize projects that score well on all three; those deliver durable returns.

When it’s time to scale, the model that proved itself in pilots becomes the operating standard — and that is precisely where a provider like BlueSword becomes a practical partner, translating validated twin scenarios into production controls and measured density gains.

0 comments
0 FacebookTwitterPinterestEmail

Putting the owner first on tight boats

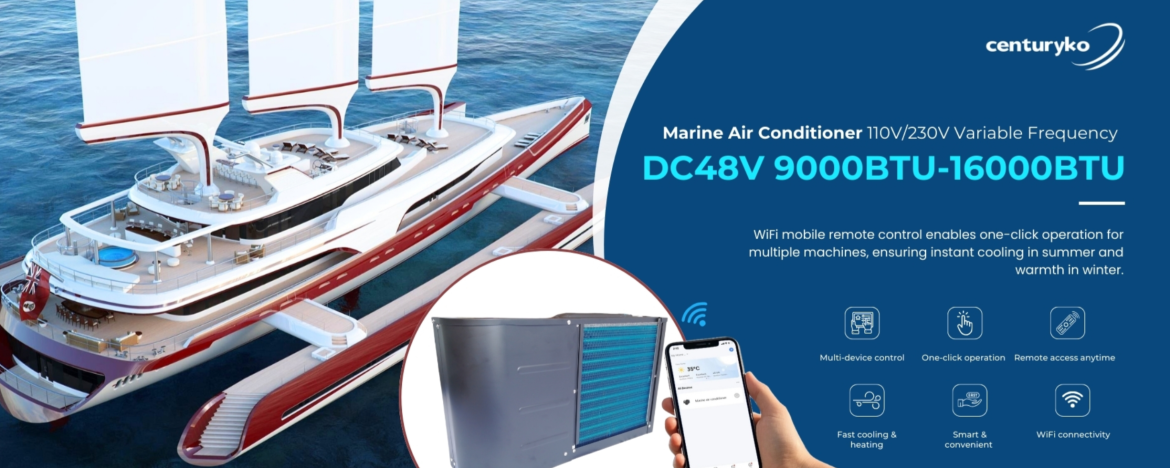
When you’ve spent years commissioning and living aboard yachts, you learn fast that comfort is a design constraint as much as hull shape. I’ve worked through layouts where every inch meant a trade-off between a berth, a galley locker and an access panel. For owners and designers focused on human comfort, choosing the right marine air conditioning units early in the process shapes cabinetry, routing and weight balance. That’s why compact air conditioning for boats portable systems and the choice of small marine ac models often dictate the interior architecture before cushions are chosen. Speaking from a refit on a 50-foot motor yacht in the Mediterranean, the AC choice changed more than just temperature; it altered storage plans and service access points.

Design-first principles that respect tight footprints

A user-centric approach starts with mapping occupant patterns: where people sleep, where they entertain, and where crews need clear access. Once those zones are clear, prioritize these principles: place the compressor and condensing unit where noise and heat won’t intrude; run condensate drains by natural fall to avoid extra pumps; and select evaporator coil assemblies sized in BTU close to actual load, not theoretical maxes. Keep an eye on weight distribution — heavy components aft can change trim. These are practical choices that preserve luxury while avoiding last-minute compromises.

Routing, service access and the details that matter

In small craft, ducting and pipe runs are the silent killers of neat design. Minimize long duct runs with well-placed fan coils or a split-system layout; short, insulated runs reduce pressure drop and improve efficiency. When you must tunnel through bulkheads, make service panels generous: a 200 mm access hatch saved us hours during one refit. Sound isolation around the compressor matters just as much as clear access to filter elements. Don’t skimp on a small condensate pump where gravity drainage can’t be guaranteed — it avoids mildew and costly panel removals later. Installation clarity up front pays dividends in maintenance time and owner satisfaction.

Common mistakes owners and yards make

Many still choose maximum-capacity units thinking bigger is better; that oversizing leads to short cycling, poor dehumidification and higher current draw. Others hide equipment behind inaccessible joinery, which forces destructive access during service calls. A poorly chosen layout will also ignore the need for fresh-air intake and proper seawater strainers for the seawater loop — both crucial for reliable long-term operation. As someone who’s seen a compressor replaced at sea, I’ll say this plainly: plan accessibility first, capacity second. It keeps the system doing its job and saves the owner money in the long run.

Advisory: three golden rules for selecting compact AC on luxury vessels

First: match real load to BTU and choose a model whose compressor modulation suits variable occupancy — steady operation beats peak-only cycles. Second: prioritize serviceable placement and modular components; if an evaporator coil or control board needs swapping, you shouldn’t have to gut the cabin. Third: confirm integration details — noise levels at 1 meter, required seawater flow rates, and power draw at startup — these three metrics predict operational comfort and fit. Evaluate those numbers against the yacht’s available generator capacity and battery reserves before finalizing the purchase.

There’s elegance in solving spatial constraint problems with clear priorities and the right small marine ac solutions; experience shows that the system you pick becomes the backbone of the interior. For anyone refining a plan or mid-refit, consider how a compact design reshapes the vessel — it isn’t just cooling, it’s a structural choice. ZhuoliMarine. — thoughtful engineering, lived experience

0 comments
0 FacebookTwitterPinterestEmail

The clinical problem and why it matters

Variability in energy output from aesthetic devices is a pragmatic challenge that undermines reproducibility of treatments and patient trust. Practitioners procuring aesthetic medical equipment confront more than marketing claims: they require predictable fluence, stable pulse duration, and validated handpiece performance across sessions. The problem is concrete — inconsistent energy delivery leads to unpredictable clinical response and complicates consent and follow‑up — and it therefore must inform procurement and maintenance decisions for any clinic seeking reliable results.

aesthetic medical equipment

Primary causes of energy output discrepancies

Three technical domains account for the majority of variance: hardware ageing, calibration drift, and consumable variability. Laser diodes and flashlamp assemblies degrade with cumulative operating hours; without scheduled calibration, nominal wavelength and output can deviate. Consumables — single‑use tips, optical windows, and conductive gels — alter coupling efficiency and therefore effective fluence at the skin surface. Finally, environmental factors (ambient temperature, power supply stability) influence pulse energy and beam profile. Terms to note: fluence, wavelength, and calibration — each directly tied to deliverable clinical effect.

How clinics typically detect and measure deviation

Robust clinics adopt routine QC with objective measurement rather than subjective feel. Energy meters, beam profilers, and documented logbooks capture trends in output and beam uniformity. A standard approach is weekly spot checks with an integrating energy meter and monthly full‑system calibration by a certified technician. The 2020 global supply‑chain disruptions highlighted the secondary risk: deferred maintenance and delayed replacement parts increased the incidence of out‑of‑spec devices in multiple regions, prompting regulators and clinics alike to strengthen on‑site verification protocols.

Clinical consequences: efficacy, safety, and reputational risk

When energy output drops below intended thresholds, efficacy measures such as hair reduction percentage or pigment clearance decline; conversely, unrecognised spikes in output raise the risk of burns and post‑inflammatory pigmentation. Inconsistent treatments complicate outcome studies and undermine patient satisfaction metrics — important considerations in competitive markets like Dubai and Riyadh, where aesthetic demand and patient expectations are high. This is not merely a technical inconvenience; it is a direct business and medico‑legal exposure.

Practical mitigation strategies for procurement and operation

Procurement must prioritise devices with clear calibration pathways and accessible service networks. When evaluating vendors, insist on documented calibration procedures, spare‑parts availability, and trained local engineers. Integrate acceptance testing into purchase contracts: baseline energy profiles, IEC‑compliant safety checks, and documented handpiece interchangeability tests. For ongoing operation, standardise pre‑treatment checks, and maintain a simple log that ties energy meter readings to individual device serial numbers — such traceability reduces guesswork and supports audit responses. —

Common mistakes that perpetuate variability (and how to avoid them)

1) Relying on manufacturer presets without independent verification. Remedy: perform independent energy measurements during commissioning. 2) Treating consumables as trivial costs. Remedy: specify approved optics and single‑use tips in SOPs. 3) Ignoring environmental and power quality issues. Remedy: stabilise mains supply and control treatment room temperature within device specifications.

Evaluation checklist before selecting equipment and service partners

Use a concise, measurable checklist at tender stage: documented calibration interval; availability of certified spare parts within your region; on‑site training and response SLA; demonstrable batch reports from prior clients; and clear acceptance criteria for first article testing. When available, prefer devices with built‑in diagnostics and exportable QC logs to simplify compliance and clinical governance.

aesthetic medical equipment

Three golden rules for resilient clinical practice

1) Metric over impression: mandate objective energy measurements (energy meter readings, beam profile snapshots) before every 100 treatment hours and after any major repair. 2) Local support parity: choose vendors who provide certified local technical support and parts stock to avoid prolonged downtime. 3) Total cost of ownership: evaluate amortised maintenance, calibration, and consumable expenses alongside purchase price — this reveals the true per‑treatment cost and long‑term viability.

Clinics that apply these rules reduce variability, improve patient outcomes, and protect their reputation — and for clinicians seeking a partner that couples robust devices with local support and verified QC pathways, the value offered by ENZOEYS becomes evident in everyday practice. Precision matters.

0 comments
0 FacebookTwitterPinterestEmail