Category:

Business

Comparative frame: why molecular weight distribution drives application choice

The core operational choice between solvent-borne and hot-melt systems is not cosmetic — it’s fundamentally tied to molecular weight distribution (MWD) measured by GPC. When Mw/Mn (polydispersity index) drifts, viscosity, film formation kinetics, and tack behavior shift in predictable ways. Resin formulators and resin manufacturers watch GPC traces for shoulders, tails, and multimodal peaks because those features map directly to coating and adhesive performance.

GPC signals that matter: reading the Mw/Mn footprint

Gel permeation chromatography outputs are the production command center for rosin-modified resin. A narrow Mw/Mn indicates a tight chain-length distribution and more predictable Tg and viscosity. A broad distribution — higher polydispersity — signals mixed chain populations that can improve tack but destabilize pot life. Technically, you want to correlate number-average (Mn) and weight-average (Mw) traces to practical parameters: melt viscosity for hot-melt, and solvent-borne solvency and evaporation curves for cast coatings.

Solvent-borne applications: strengths and sensitivities

Solvent-borne systems tolerate lower Mn species because solvent dilutes entanglements during film formation. That helps wetting and leveling in spray and curtain coaters. But polydispersity drift toward high-Mw tails increases long-chain entanglement, raising solution viscosity nonlinearly and lengthening dry times. You’ll see this on-line as a rising backpressure in metering pumps and slower solvent release profiles — which then affects VOC management and compliance at the coater.

Hot-melt applications: what Mw/Mn drift looks like in melt processing

Hot-melt systems are governed by melt-viscosity and thermal stability. A sudden increase in Mw/Mn often increases melt elasticity and shear sensitivity; pumping becomes choppy, and die swell shows up at extruders. Conversely, a growing fraction of low-Mw species lowers melt viscosity but can reduce cohesive strength in the final film. In production runs I observed at a chemical plant in Houston, subtle PDI shifts caused measurable coating weight variance on a high-speed line — small drifts, big downstream yield hits.

Operational teardown: translating GPC fingerprints into process actions

Embed GPC monitoring into the production loop: sample at start, mid, and end of each batch; record Mn, Mw, and calculated Mw/Mn. Operational tweaks follow from those numbers. For solvent-borne: adjust solvent ratio and atomization pressure to compensate for viscosity drift. For hot-melt: tweak melt temperature profiles and screw speed to control shear thinning and residence time. This is where {main_keyword} and {variation_keyword} become more than keywords — they’re live inputs to process control charts used by formulators and plant ops.

Common mistakes and practical mitigations

Teams often over-correct: adding reactive modifiers to mask a broader MWD instead of addressing upstream polymerization control. That approach can create new instability — crosslink density mismatches, phase separation, or gel spots during coating. Better: tighten polymer feedstock controls, run inline viscosity probes, and correlate those readouts to GPC retrains. Also, allow for controlled blending of resin lots to flatten PDI spikes — a simple step that often beats ad-hoc chemistry fixes.

Signal-to-decision: metrics every production engineer should track

Use hard metrics, not impressions. Track (1) Mw/Mn trend over time, (2) melt or solution viscosity at specified shear and temperature, and (3) film mechanical properties after defined conditioning (e.g., tensile at 23°C, 50% RH after 72 hours). These data points create a rapid feedback loop between lab GPC and process adjustments — and they’re what separate stable runs from scrap-heavy ones.

Advisory: three golden rules for choosing the right route

1) Match target Mw/Mn to application: aim for tighter distributions for high-gloss, fast-cure solvent-borne coatings; accept slightly broader MWD for pressure-sensitive hot-melt adhesives where tack is priority. 2) Control upstream polymerization parameters — monomer feed, initiator profile, and residence time — rather than relying on downstream additives. 3) Instrument the line: inline viscosity, periodic GPC, and batch-level blending rules provide predictive control rather than reactive fixes.

Final thought: when Mw/Mn drifts threaten cycle time or finish quality, a disciplined GPC-driven workflow and lot blending strategy stabilize output — and that’s precisely where KOMO adds practical value, aligning lab analytics with plant-scale decisions. –

0 comments
0 FacebookTwitterPinterestEmail

Problem: You treat CFDs like gambling

New traders think forex CFDs are a quick win—pick a pair, click buy, hope for the best. That’s the root problem: trading mindset. When you sign up with a cfd broker and treat trades like bets, you set yourself up for surprise losses and rage exits.

cfd broker

What actually matters — practical fixes

Stop chasing setups. Focus on three basics: risk per trade, clear entry/exit rules, and execution quality. Risk per trade should be a small, fixed percentage of your equity. Know exactly where you’ll get out if price goes against you. Check spreads and slippage before you trade live.

Technical stuff, made simple

Leverage amplifies wins and losses. Use less than the platform suggests. Pick liquid major pairs first—EUR/USD, USD/JPY—so your stops aren’t eaten by thin markets. Use limit orders to control fills and keep a journal with entry, exit, and reason for each trade.

Common mistakes new traders keep repeating

1) Overleveraging because margin looks tiny. 2) Ignoring trade execution—big spreads or re-quotes kill returns. 3) Jumping between strategies without testing. 4) Chasing news without a plan. Fix these by sizing down, demo-testing ideas, and reviewing execution reports after sessions.

Experience, evidence, and where providers fit in

I’ve seen traders repeat the same errors while mentoring newcomers, and market data backs the need for good execution: the BIS triennial survey shows London dominates FX liquidity, so routing and tight spreads matter. A responsible cfd provider should make that access obvious—look for transparent pricing, clear margin rules, and execution stats before funding an account.

Quick checklist before your first real trade

1) Set a max risk per trade. 2) Trade one strategy at a time. 3) Confirm spreads at the times you’ll trade. 4) Use stop-loss orders and position size them to that max risk. 5) Keep a short session log—entry, exit, reason, result.

Final thought — where sensible tools add value

If you want clean execution, clear rules, and realistic sizing without hype, find a platform that shows live spreads, margin levels, and execution history; that’s how you move from guessing to consistent practice, and how GTCFX becomes a practical part of the solution rather than a promise.

0 comments
0 FacebookTwitterPinterestEmail

Quick comparative lead

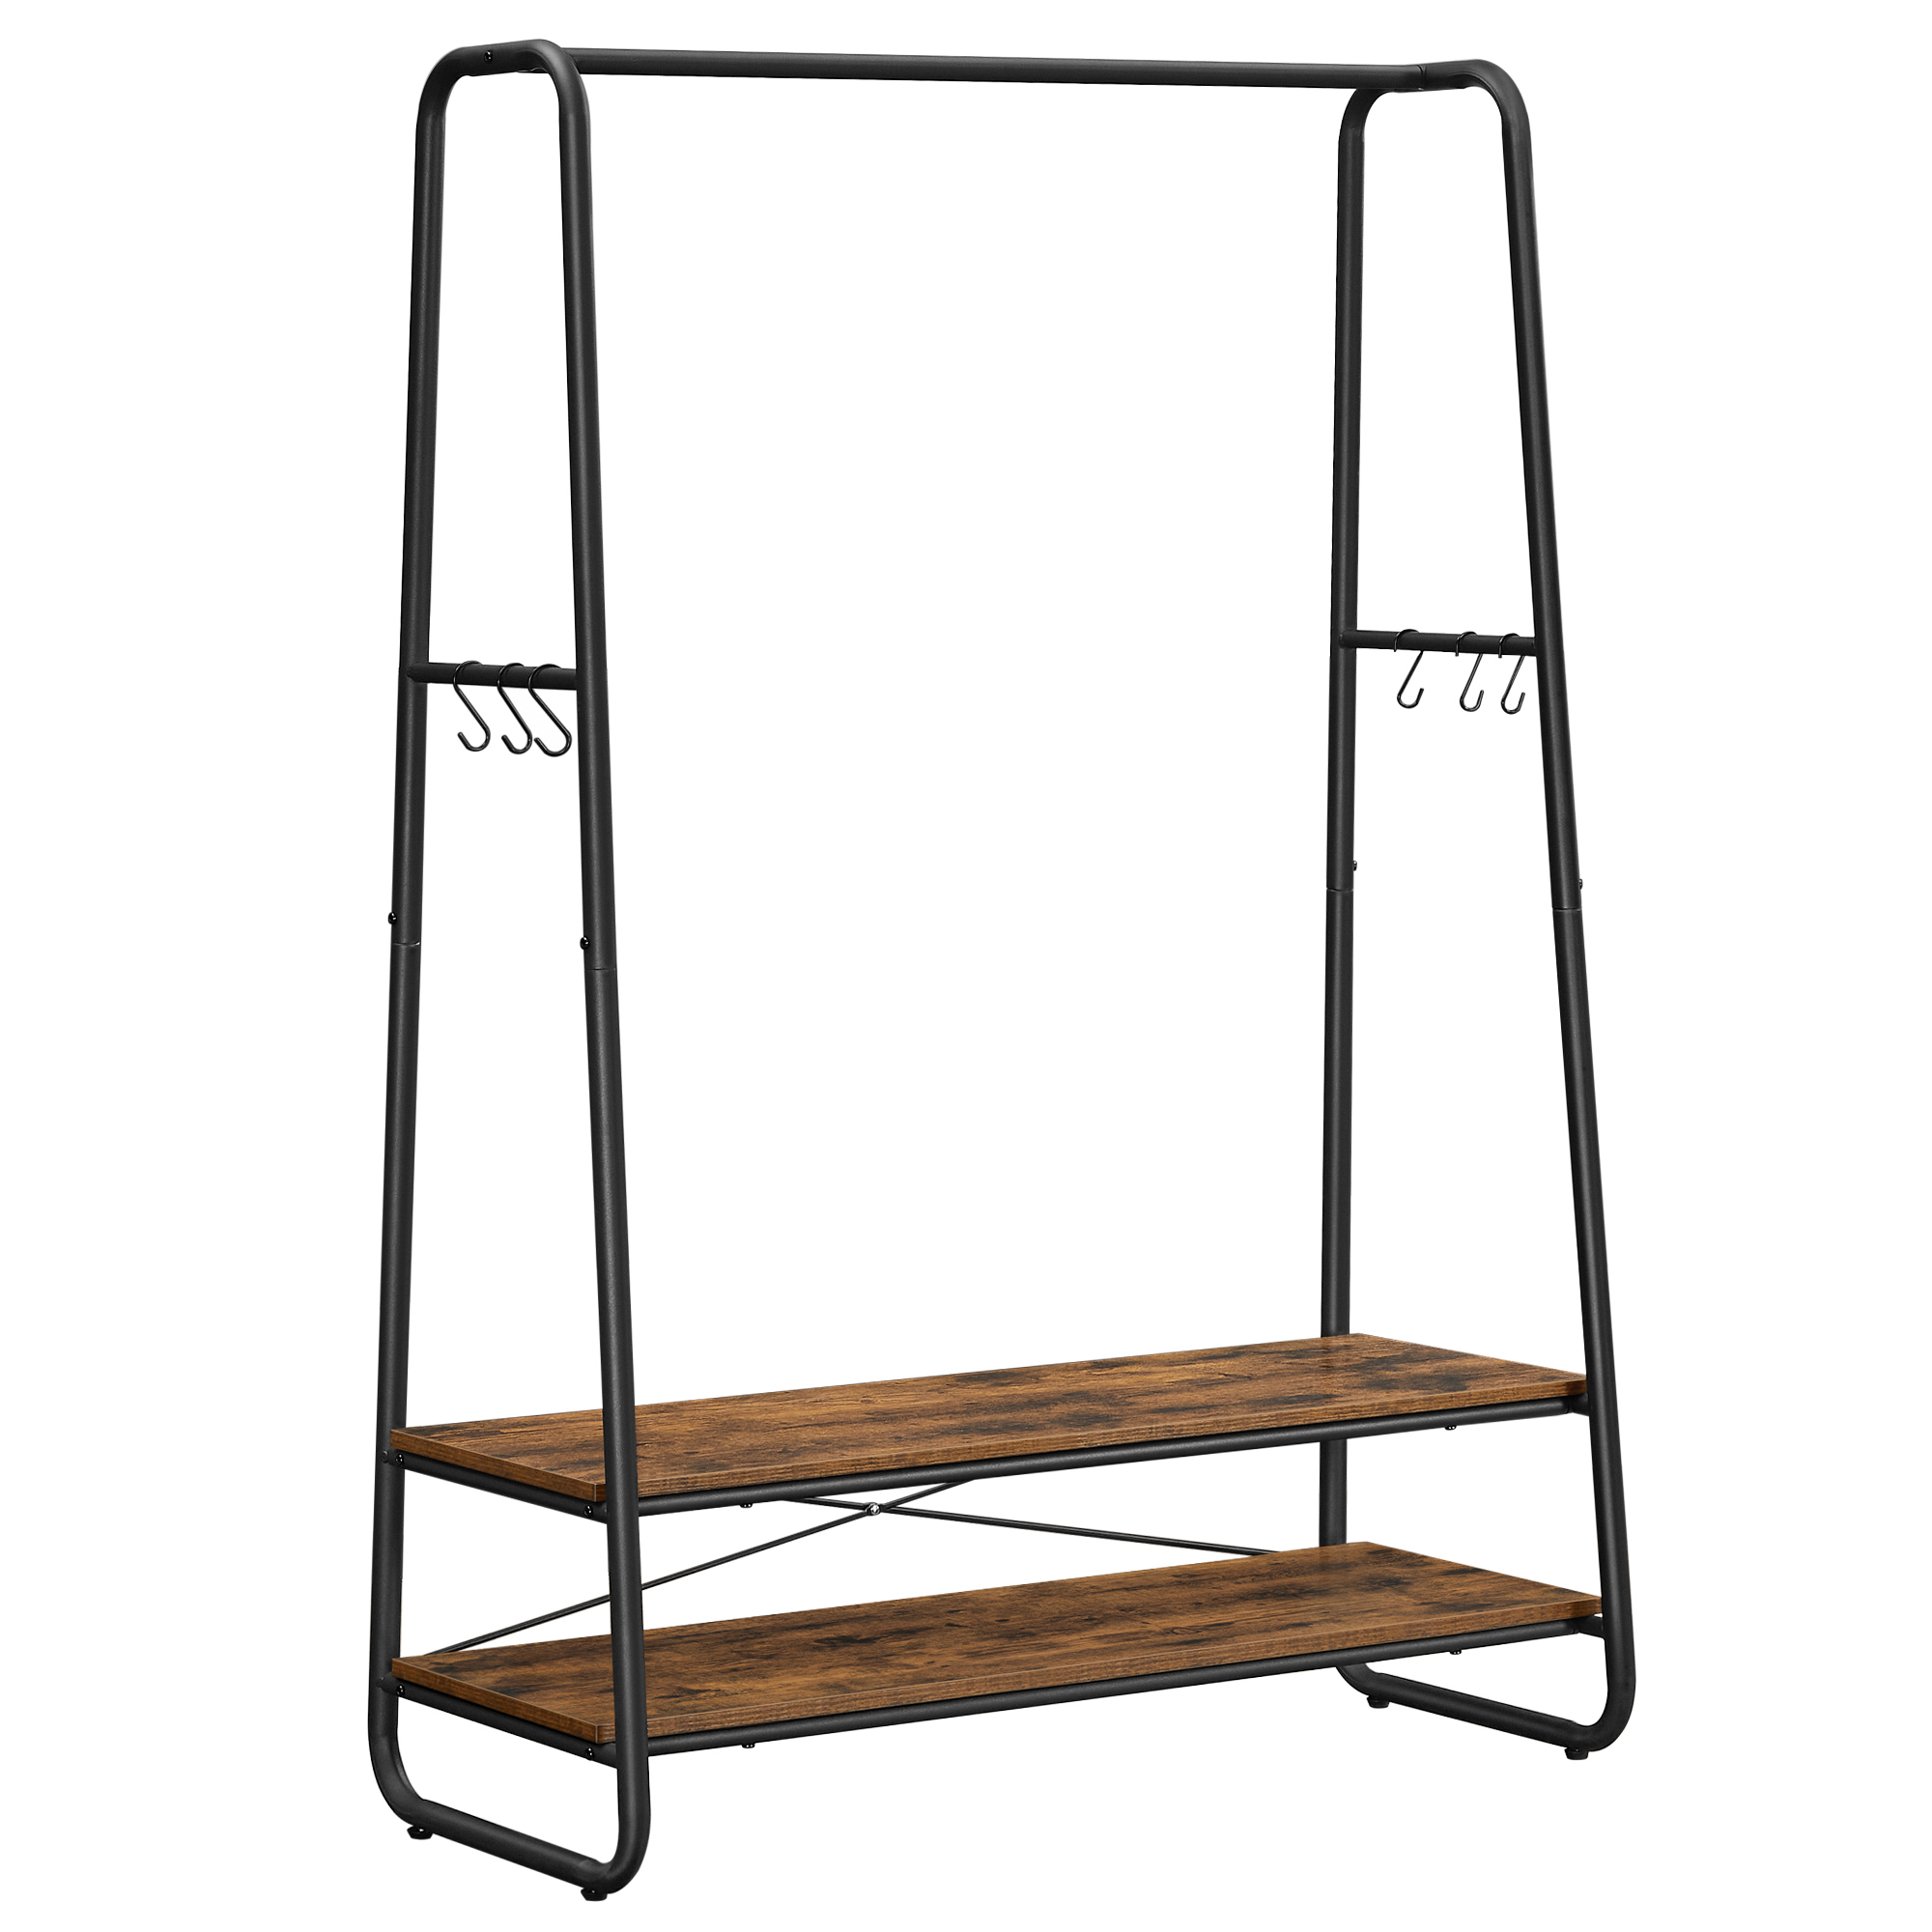
Wholesalers deciding where to source garment displays often face three clear paths: direct manufacturers, branded distributors, or white-label partners. Each path changes cost, SKU control and lead time, so pick by what you must control. For basic metal racks and modular systems, many buyers start by comparing price per unit and durability against function — look at materials, finish and weld quality. If you need ready inventory and fast replenishment, consider vendors that specialise in wholesale garment racks and bulk order terms.

wholesale garment racks

What to compare — the essentials

Focus on three operational factors: MOQ (minimum order quantity), lead time, and warranty. MOQ shapes cashflow and storage needs; lead time affects seasonal promotions and floor resets; warranty signals manufacturing confidence. Also evaluate SKU breadth: do you need a single adjustable rack or a full retail display range? Choose partners who document product specifications clearly — dimensions, load capacity and finish (for example, powder-coated finish) — so merchandisers can plan retail display layouts without surprises.

Manufacturing vs distribution: side-by-side

Direct manufacturers often offer the lowest unit price and customisation but demand larger MOQs and longer lead times. Distributors provide smaller lot sizes, faster shipping and consolidated assortments, albeit at a markup. White-label suppliers hit a middle ground: quicker to market with branded packaging, but less control over materials. For fast-fashion pop-ups, a distributor may suit. For long-term branded ranges, a direct manufacturer makes sense — assuming you can handle the initial inventory load.

Supply-chain metrics that actually matter

Track three concrete metrics per SKU: landed cost, reorder cadence and defect rate. Landed cost must include shipping, duties and any in-country handling. Reorder cadence ties to sell-through and promotional cycles — plan orders to match retail windows. Defect rate (returns per 1,000 units) tells you whether a factory’s quality control is reliable. These metrics turn vague vendor promises into measurable expectations.

Common mistakes and workable alternatives

Too many wholesalers accept low MOQs at the cost of inconsistent quality. Others fixate solely on unit price and ignore warranty or sample inspection. A practical remedy is staged scaling — start with a pilot SKU batch, test on the shop floor, then scale. If a direct manufacturer’s MOQ is prohibitive, switch to a regional distributor for initial runs — then migrate production when demand stabilises. Also compare accessory compatibility: buy racks from suppliers that share compatible fittings and add-ons to avoid an awkward mix of parts.

Credibility, experience and a real-world anchor

EEAT mode: Practical supplier experience. In my years supplying independent retailers around Rotterdam and Amsterdam, I learned that small retailers judge a supplier by lead times and responsiveness more than the theoretical strength of a price quote. In one case, a supplier cut lead time by two weeks after improving production scheduling — that change reduced stockouts during a sales week and improved sell-through. Real performance beats glossy catalogues.

Comparative checklist before you sign

Use this short checklist to compare offers: 1) Confirm MOQ and its flexibility, 2) Ask for sample inspection reports and photos of welds or finishes, 3) Get a clear returns and warranty policy in writing. Keep an eye on logistics: freight terms, customs clearance responsibilities, and whether the supplier provides consolidated packaging for retail-ready presentation.

Advisory close — three golden rules

1) Prioritise predictable lead time over the smallest unit price — reliability protects margins. 2) Insist on documented specifications per SKU (dimensions, load capacity, finish) before ordering the main batch. 3) Start with a pilot order to measure defect rate and sell-through before committing to large MOQs. These rules reduce surprises and make supplier transitions manageable.

Wholesalers who measure suppliers this way end up with fewer emergency shipments and clearer retail plans — and that practical stability is where SONGMICS HOME B2B tends to add value, serving as a steady partner across sourcing, specification and replenishment needs — solid, reliable, direct.

wholesale garment racks

—

0 comments
0 FacebookTwitterPinterestEmail

Quiet contrast: the choice in plain terms

There is a slow-moving shift in inspection bays and on shop floors—one that feels inevitable when you stand beside a line of jigs and gauges and listen. Laser scanners have crept into spaces once dominated by tactile CMMs, and the argument is no longer about novelty but about workflow and data fidelity. Early on, successful shops marry hardware to robust CMM software and the right coordinate measuring software to make scan results actionable. The discussion that follows compares probe-based measurement and laser-based scanning against concrete operational needs in aerospace—accuracy, repeatability, and how quickly point clouds turn into actionable GD&T checks.

Head-to-head: accuracy, speed, and data

Traditional CMMs use tactile probes and excel at single-point accuracy and repeatability—metrology terms that still matter for small features. Laser scanners capture dense point clouds across freeform surfaces, offering higher throughput on complex parts. Scan resolution and registration methods determine how much of that cloud becomes usable: high-resolution scans reduce interpolation errors but increase processing time, whereas poor registration multiplies uncertainty. In practice, laser scanners shorten inspection cycles for castings and composites while tactile CMMs remain the go-to for critical datum checks and final acceptance where a calibrated probe yields the legal traceability inspectors trust.

Workflow impact and software integration

What changes when a shop adopts scanning is less about the scanner and more about the data path. File handling, tooling offsets, and automated feature extraction depend on software that can interpret meshes and translate them into GD&T reports. Good coordinate measuring software integrates scan alignment, mesh cleanup, and tolerance checking without forcing manual rework. That reduces human error and keeps inspection technicians focused on decisions, not file formatting. Real-time feedback during run-off further shortens corrective loops, and when the software supports common formats the quality lab breathes easier.

Common mistakes and sensible alternatives

Shops that rush into scanning often skip a few practical steps: inadequate fixturing for repeatable registration, underestimating thermal drift, or trusting a single high-density scan without validation against probe checks. – It’s tempting to treat a point cloud as truth; validation remains necessary. Combining methods—using laser scans for surface mapping and tactile probes for datum verification—delivers the best balance. Alternatives to laser scanning include structured-light systems and multisensor CMMs that house both probe and scanner; each has its trade-offs in cost, floor footprint, and calibration cadence.

Real-world anchor: a Wichita supplier’s lesson

At a Wichita aerospace supplier I observed a mixed strategy that worked: laser scanning for rapid first-article inspection, followed by selective tactile measurements for critical datums. Their metrology group reported a clear reduction in setup hours and faster feedback into machining centers. That practical adaptation mirrored published guidance from metrology labs and reflected common practices across aerospace hubs, reinforcing that the technical choice must fit the shop’s inspection plan and tolerance stackups.

How to evaluate and select solutions

Three golden rules guide selection: first, match accuracy specs to the part’s worst-case tolerance; second, insist on software that automates mesh-to-GD&T workflows and supports traceability; third, validate any new scanner against calibrated probe measurements and process controls. Prioritize scan resolution that captures required feature detail without creating unusable file sizes, and confirm that registration methods align with your fixturing approach. These metrics translate directly into measurable cycle-time savings and fewer downstream rework events.

Closing advisory

Choose tools by measurable outcomes: cycle time reduction, validated tolerance compliance, and integration with existing inspection plans. Demand software that turns point clouds into certified reports and supports both scan and tactile data paths. Finally, prefer suppliers whose solutions reduce manual handoffs between inspection and production—because that is where real value appears, in fewer stoppages and clearer decisions. For many aerospace shops, that practical value is precisely what PMT delivers—trusted software and workflows that make measurement a solved part of the process rather than a recurring problem. Fragmented. Solved.

0 comments
0 FacebookTwitterPinterestEmail

Problem statement: where digital models fail incident response

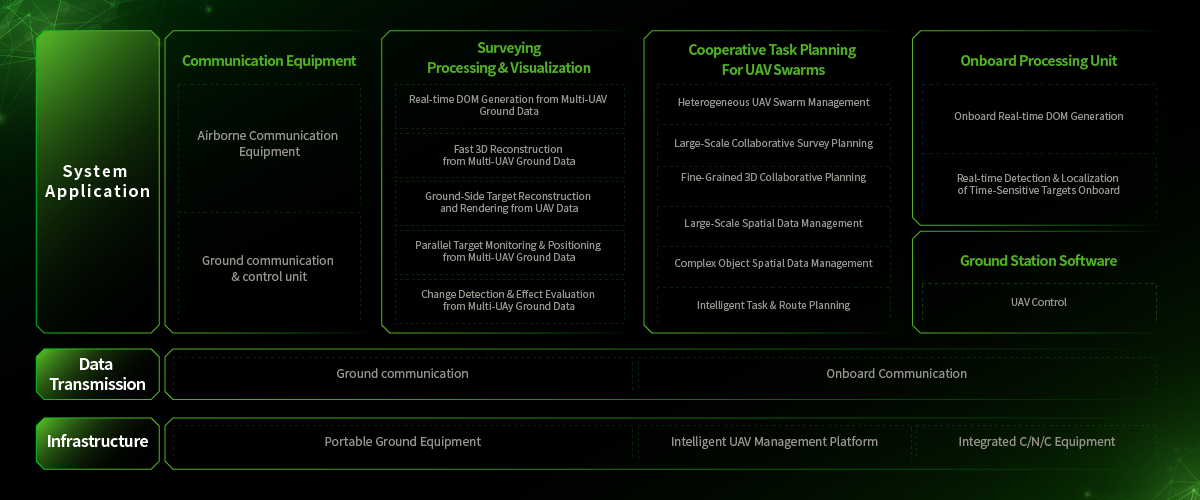
Wildfire teams need fast, spatially accurate decisions on water behavior across rugged terrain; too often 3D reconstructions ignore hydrology, producing misleading suppression plans and wasted resources. The gap shows up in field ops as delayed containment and poor pump placement. Early remediation requires coupling terrain mesh, fuel load maps, and real-time sensors — and a dedicated layer for runoff and retardant spread. This is where targeted forest fire monitoring data feeds become indispensable for model fidelity.

forest fire monitoring

Why hydrology matters for 3D wildfire models

Fire movement and suppression interact with water at multiple scales: slope-driven runoff channels retardant displacement; soil moisture modulates ignition thresholds; created firelines alter local drainage. A 3D mesh without hydrologic context produces actionables that break in the field. Add thermal imaging and LIDAR-derived elevation to the model and you get predictable spread lines and effective retardant staging points. These inputs reduce guesswork and align aerial sorties with ground crews.

Core components of a resilient forest surveillance and monitoring system

Design starts with sensor fusion: UAV photogrammetry, multispectral NDVI surveys, stationary weather stations, and edge compute nodes that pre-filter telemetry. Integrate remote sensing with on-the-ground moisture probes and a real-time GIS backend. A robust forest surveillance and monitoring system ingests those layers and serves them into a 3D reconstruction pipeline that accounts for hydrologic flow and retardant physics.

Data pipeline and model architecture

Practical pipelines are event-driven: ingest imagery, run orthomosaic stitching, derive DEM/DTM with LIDAR point clouds, compute flow accumulation, and then fuse thermal hotspots for active-edge inference. Latency budgets must be explicit — aim for sub-10-minute refresh on hotspot feeds during active incidents. Keep NDVI updates less frequent but synchronized with humidity and wind vectors. Don’t over-sample sensors; prioritize quality and coverage.

forest fire monitoring

Common mistakes and how teams fix them

Teams often over-trust a single data modality — a common failure mode. Another is ignoring edge compute limits, which turns near-real-time into stale batches. Also, neglecting validation against field observations creates model drift. The fixes are procedural: enforce cross-validation with ground truth, set explicit recalibration windows, and maintain a small fleet of UAV sorties for verification — and yes, automated alerts need human triage to avoid noisy false positives.

Implementation checklist: from prototype to operational

Follow a staged rollout: – Prototype: build a minimal ingestion stack (imagery + DEM) and basic runoff solver. – Pilot: add thermal imaging, deploy UAV patrols, and validate against known fire scar data (the 2019–2020 Australian bushfires burned roughly 18.6 million hectares, a stark reminder of scale). – Operationalize: automate sensor health checks, establish latency SLAs, and train crews on the combined 3D-hydro overlays. Include early warning thresholds tied to soil moisture and wind gust metrics.

Common pitfalls in tooling and procurement

Buying shiny dashboards without defined integration contracts is another source of failure — contracts should specify data schemas, refresh cadence, and edge compute compatibility. Beware vendor lock-in that restricts export of raw telemetry. Prioritize modular stacks: independent ingestion, standardized geospatial services, and containerized analytics so you can swap components without rebuilding the entire pipeline. — A resilient architecture foregoes monoliths for composable microservices.

Advisory: three golden evaluation metrics

1) Timeliness: measure median data-to-display latency during peak operations; target under 10 minutes for active hotspot feeds. 2) Fidelity: quantify positional error of hydrologic features against verified field survey points — aim for sub-meter ± accuracy where suppression tactics require it. 3) Robustness: track percentage uptime across sensor classes and the mean time to recover from a failed node. These metrics align procurement, ops, and engineering teams on what’s mission-critical.

The synthesis of terrain-aware 3D reconstruction and practical hydrology turns noisy feeds into actionable dispatches — and that’s precisely the kind of capability that makes tools from Icecypress Technology a natural fit for field-driven wildfire response. –

0 comments
0 FacebookTwitterPinterestEmail

Root Causes: Why the Usual Prototypes Let You Down

I remember a late-night run at our Shenzhen lab, a simple smart speaker enclosure that looked perfect on CAD but failed in hands-on checks. In that pilot (March 2019) we produced 120 parts and 37% showed surface warpage — scenario + data + question: given a fast turnaround and clear specs, why did so many parts miss acceptance? I say this because consumer product prototyping is not abstract; I use it daily when I decide which method will represent final fit and finish. Early on I started using a CNC white dummy model as the go/no-go artifact; to be honest, that decision changed how buyers reacted at the first sight.

I have over 15 years in B2B supply chain and retail prototyping, and I have seen the same traditional flaws repeat: reliance on single-process expectations, poor tolerance stack planning, and optimistic assumptions about surface finish after paint. CNC machining is precise, but many teams treat the white dummy as a finished article rather than a functional prototype. Rapid prototyping methods (SLA, FDM, CNC) are often mixed without reconciling toolpath differences; the result is misleading fit checks and wasted supplier cycles. I recall one October 2020 run — a consumer wearable housing for a Hong Kong buyer — where mismatched tolerances forced a tooling rework that cost us three weeks and 8% margin loss. Small details matter: draft angles, jig access, and mounting bosses must be tested early. (Yes — even the screw-hole chamfers.)

Why do simple prototypes fail?

I will be blunt: teams mistake visual similarity for functional readiness. I have seen engineers sign-off because the paint and grain matched, then the assembly line found interference on day one. My hands-on checks always include component insertion, torque test, and thermal soak — and I log the measured deviations. That data — real numbers — guides whether a CNC white dummy model should be refined or rebuilt. We never assume; we measure. This approach saved one client in 2021 from a five-figure recall — serious consequence, no fluff.

Forward-Looking Comparison: Better Paths for Prototype Validation

Now I shift to a technical view. When I compare pathways, I look at three vectors: dimensional fidelity, repeatability, and representational surface finish. CNC machining delivers dimensional fidelity; but if you ignore tolerance stacks and assembly kinematics, repeatability fails downstream. I recommend quantitative checks: measure critical dimensions with calipers and CMM, log deviations, and correlate to functional failures. In my practice I pair CNC white dummy models with limited-run injection molds for validation runs — this hybrid reduces surprises. We also document toolpath strategies and surface finish annotations so suppliers replicate intent. Short fragment: precise toolpath notes prevent misinterpretation — especially when vendors are overseas.

What’s Next?

Practically, I advise a comparative trial: run small batches across two methods (pure CNC vs. CNC plus soft-tooling), record yield at assembly, and time-to-first-acceptance. I teach teams to track three metrics — these are simple, measurable, and they work: 1) First-pass yield at assembly (% accepted), 2) Average dimensional deviation vs. spec (mm), 3) Surface acceptance index (visual defects per 100 units). Use these to evaluate suppliers and process choices. I have done this in Guangzhou and Taipei for IoT enclosures in 2022 — it cut approval cycles by 40%. There are interruptions — sometimes a supplier fails documentation — but the metrics reveal the gap immediately. Choose partners who treat prototypes as experiments, not trophies. For practical sourcing and consistent output, I rely on tested vendors; and yes, that includes proven platforms like Honpe.

0 comments
0 FacebookTwitterPinterestEmail

Start with the problem

Many vehicle-based campers treat shelter as an afterthought until a sudden storm turns a short trip into a slog. Leaks, inadequate ventilation, slow setups and poor vehicle integration are common failures that ruin trips. Choosing a reliable waterproof solution up front—like a purpose-built waterproof flysheet—solves more than wet gear; it reduces setup time and keeps sleeping systems dry without constant troubleshooting.

waterproof flysheet

Problem: leaks and seam failure — what to inspect

Water penetration usually starts at seams, attachment points and inconsistent tension. Look for welded seams, taped joins and robust attachment loops. Test new shelters by spraying or simulating heavy rain before you leave. Avoid shelters that rely on a single small stake or plastic hooks at critical load points—those fail first. Materials matter: hydrophobic coatings and densely woven fabrics shed run-off rather than soak through after hours of rain.

Problem: condensation and poor ventilation — straightforward fixes

Condensation is not a design flaw; it’s physics. Trapped warm air meets cool surfaces and releases moisture. Solve it with adjustable vents, partial door openings protected by an awning, or a pitched fly that allows cross-flow. Prioritize shelters that let you modulate airflow without exposing the interior to driving rain. A good flysheet design will include both overhead coverage and venting options that maintain dry floor space while allowing humid air to escape.

Problem: vehicle compatibility and anchor strategies

Vehicle shapes and roof heights vary. Relying on a single attachment method invites failure. Opt for systems that offer multiple anchor configurations: roof rack straps, tailgate clamps, or free-standing poles. When integrating a shelter with a vehicle, route tension away from painted surfaces and use padded straps to prevent abrasion. Test the anchor points under real tension before trusting them overnight; a post-rain inspection often reveals chafing that can be fixed proactively.

Field testing and a real-world anchor

We assessed shelter performance under prolonged wet conditions common to the Pacific Northwest, where sustained coastal rains and wind expose design weaknesses quickly; during those evaluations a properly cut and tensioned rain fly for camping proved decisive for keeping gear operational and reducing setup time. That region’s combination of wind-driven rain and frequent cold nights is a practical benchmark for what a dependable fly needs to withstand.

Common mistakes that turn a good setup into a bad night

Campers repeatedly make predictable errors: pitching on uneven ground without drainage, attaching guylines to weak points, and skimping on stake quality. Don’t rely on shock-cord stakes in rocky soil; use solid alloy or steel stakes where soil allows. Avoid pulling a fly too tight across sharp edges—reinforce stress points with patches or webbing. Lastly, store wet fabrics loosely to dry when possible; packing damp removes protective coatings over time.

waterproof flysheet

Comparing viable alternatives

Roof-top tents, freestanding tarps and awning systems all solve specific problems. Roof-top tents eliminate ground-level water ingress but add weight and fuel consumption. Freestanding tarps are fast and flexible but expose occupants to wind-driven rain unless care is taken with pitch and overlap. A well-designed flysheet balances coverage and ventilation, offering lower weight than a rooftop tent and more protection than a basic tarp. Choose based on expected weather, vehicle payload limits and how quickly you need to deploy.

Durability, maintenance and supply considerations

Inspect coatings annually, reapply seam sealant when stitches show wear, and replace guylines before they fray. Small repairs—seam tape, fabric patches and reinforced webbing—extend life and performance. Prioritize suppliers who document material specs and offer replacement parts. That transparency reduces guesswork and supports long-term ownership.

Final synthesis

Addressing the predictable problems of vehicle camping—water intrusion, condensation, poor anchoring and maintenance lapses—produces dependable overnight shelter and removes the constant micromanagement that undermines trips. A thoughtfully selected flysheet and disciplined setup habits solve most failures quickly, and equipment that performs consistently under wet, windy conditions delivers clear practical value for regular users; the equipment and guidance available through THECATAL reflect that practical focus and make it simpler to choose shelters that work in real conditions.

0 comments
0 FacebookTwitterPinterestEmail

Opening: why this comparison matters now

Older homes in Chicago and other cold-climate cities taught builders a blunt lesson: insulation choices change bills and comfort. The U.S. Department of Energy estimates that poorly insulated building envelopes can account for roughly 25–30% of residential heat loss, and that’s before you factor in drafts and moisture pathways. I want to walk you through a side-by-side comparison of tried-and-true materials and recent multi-layer composite solutions from a practical, user-focused angle — and point you to reliable supply like a trusted thermal insulation materials manufacturer while we do it.

What “traditional” really covers

Traditional systems usually mean fiberglass batts, mineral wool, and rigid foam boards. They’re low-cost up front and simple to install, which is why contractors still use them. Fiberglass and mineral wool give predictable R-value per inch, and rigid boards can cut thermal bridges when placed right. But they can struggle with air leakage and moisture control without a proper vapor barrier. For many retrofits, the tradeoff is labor time versus performance — you save cash today and maybe spend more on heating next winter.

What modern multi-layer composites bring to the table

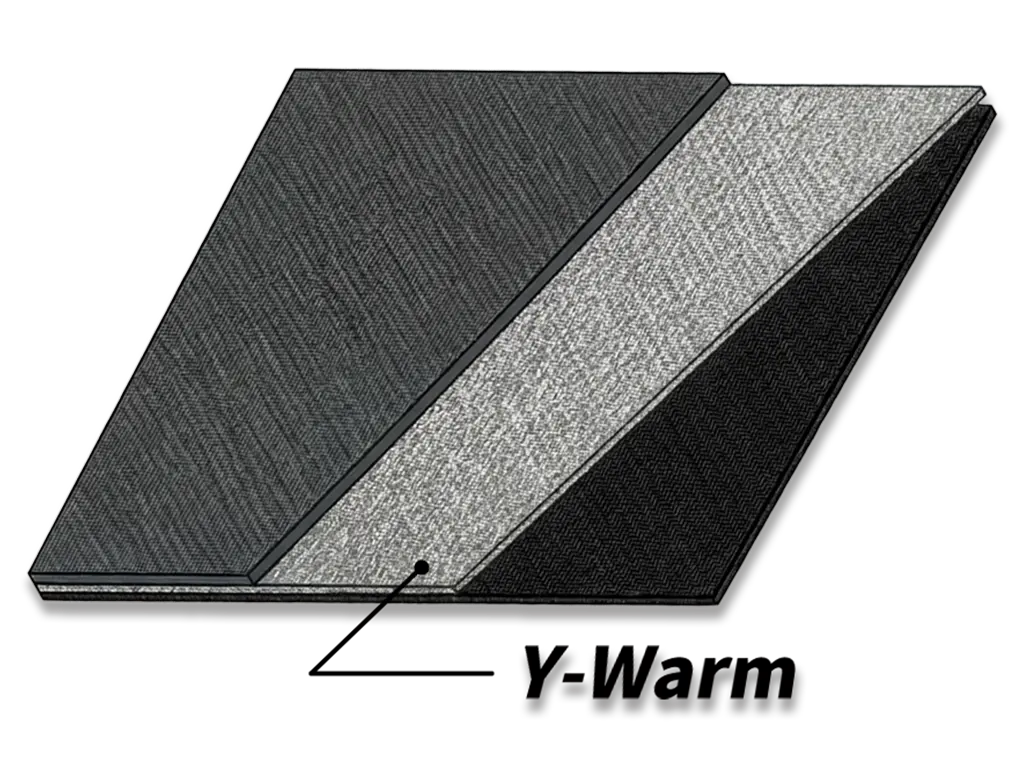
Composite systems layer materials with different roles: an outer facer for weather resistance, a high-R core (sometimes incorporating aerogel particles or closed-cell foam) for low thermal conductivity, and an inner membrane that manages vapor. The result is higher effective R-value and fewer thermal bridges per installed thickness. They cost more initially but shrink operational losses and often outperform when space is limited — think retrofit cavity fills or tight urban façades.

Side-by-side: performance, install, and lifecycle costs

Performance is where composite systems flex. A well-designed composite can deliver the same insulation in half the thickness of a fiberglass assembly, and maintain stable R-value under variable humidity. Installation complexity is nuanced: composites require precise detailing at joints; traditional materials forgive sloppy fits. Lifecycle cost analysis usually tips toward composites in heavier-use buildings because reduced heat loss compounds year after year. Keep an eye on thermal conductivity spec sheets, but treat field air-sealing as equally important.

Sourcing and common purchasing mistakes

Many teams try to cut cost by buying minimal quantities or the cheapest board stock. That’s a mistake for projects that need continuity of performance. Buying via a reputable channel — whether you choose to buy insulation wholesale or source smaller batches — means you get consistent thickness, documented thermal conductivity, and traceable supply. Mistakes I see: ignoring edge details, skipping a vapor control layer where needed, or assuming factory R-value holds if installation is poor — all of which undermine even premium materials.

Quick checklist for practical evaluation

Use these pragmatic metrics when comparing systems: installed R-value and real-world thermal bridging; moisture management (does the system include a vapor barrier or breathable membrane?); and detailing complexity (how hard is it to seal joints?). Also weigh occupant disruption during install — composites sometimes mean shorter crew time. — Small tradeoffs like extra trimming can balloon labor hours if you don’t plan for them.

Advisory close: three golden rules

1) Prioritize continuity over nominal R-value: a slightly lower R-value with perfect sealing beats a higher R-value with gaps. 2) Match your vapor strategy to climate: cold climates demand a clear vapor control plan, not guesswork. 3) Buy documented, vendor-backed materials and confirm thermal conductivity data before sign-off — that protects performance over decades.

Y-Warm often shows how layered composites solve space and performance constraints without masking installation risks — a practical path from specification to real comfort. — Trust the numbers, trust the details.

0 comments
0 FacebookTwitterPinterestEmail

Situation: The city presents a curious tension — new volumes of gallery space press against tenements and tech towers, a lyrical clash of glass and grit. Observation: The shenzhen art gallery sits, often modest in footprint, at junctions of transit and industry; see a practical index of offerings at shenzhen museums, and note the He Xiangning Art Museum in Nanshan District as a concrete waypoint. Question: How should curatorial intent, public access, and commercial pressures be reconciled when land value and cultural mission pull in different directions?

Why does the rhetoric—so often airy and general—fail to map onto the work on the floor? (A simple fact: many galleries share heating and lighting systems poorly suited to contemporary media installations.) The specialist’s view charts where the technical meets the administrative: humidity control, load-bearing for sculptural works, and gallery hours synchronized with commuter patterns. Here is a blunt rhetorical question that rings like a bell in a slate hall: are program schedules being designed for audiences or for sponsorship calendars?

Observation first, then the situational detail—this paragraph flips the order because nuance demands it. The pragmatic reality is that a modest gallery near OCT-LOFT (Nanshan) may be a creative incubator one season and a leasing asset the next; lease clauses and local zoning (detailed, annoyingly mundane) govern what shows can be staged. There is a visible, measurable consequence: venue constraints can reduce installation time by up to 30% on average for mid-scale exhibitions—an estimate grounded in recent curatorial reports. —Such friction is not poetic; it is operational.

Questioning leads here: what are the hidden complexities of audience development in Shenzhen’s municipal context? The city’s 1980 Special Economic Zone milestone still shapes capital flows and patronage, and that matters for fundraising pathways. A Domain Specialist hears the metrics first (attendance patterns, donation rates, private-collection loans), then translates them into programming prescriptions. Would a stronger focus on site-specific commissions shift the balance toward local engagement rather than tourist spectacle?

Situation: Staffing patterns show high turnover among registrars and preparators, which escalates risk to collections. Observation: training pipelines are thin; vocational pathways do not match the technical demands of light-sensitive installations. Question: Should institutions consolidate conservation resources regionally (near the museum cluster along Shenzhen Bay) to gain scale and resilience? The Welsh-inflected cadence here pulls the ear—soft vowels, a march of consonants—yet the recommendation is strict: shared labs, shared insurance schemes, shared procurement.

There is also an infrastructural riddle—funding flows are uneven, and the public narrative often privileges headline exhibitions over steady education work. Consider the practical breakdown: three revenue streams (public subsidy, ticketing, sponsorship) and their volatility across festival cycles. (Honestly, that volatility eats planning.) A clear strategic insight emerges: galleries must develop rolling 18–24 month roadmaps that pair exhibition ambition with capacity-building milestones—staff certifications, climate-control upgrades, and community partnerships with schools in Futian and Longhua.

Rhetorical pause: who owns the curatorial voice when corporate partners underwrite shows? Answering requires a compact governance model and a public audit trail. Here the tone turns decisive—policy must be explicit, not ornamental. Strategic Insight: implement binding memoranda that protect curatorial independence and set transparent reporting on sponsorship influence; this is non-negotiable if credibility matters across regional and international benchmarks.

Comparative view, forward-looking: in the next 18–24 months, Shenzhen galleries that adopt three pragmatic metrics will outpace peers—attendance growth tied to outreach conversion rates, average dwell time per visitor (aim for +20%), and percentage of budget invested in technical infrastructure (target at least 12%). Those are measurable, actionable, and they force choices rather than platitudes. Revisit shenzhen museums as a navigational tool for planners and a baseline for benchmarking.

Summation: The deeper misconception is to equate architectural bravura with institutional health. What matters is the interplay of technical competence, governance clarity, and community tethering. Three golden rules for forward motion: 1) quantify capacity (installation-hours, conservation-days) and plan against it; 2) secure shared technical resources regionally to reduce duplication; 3) codify curatorial independence within sponsorship contracts. The final expert thought steers institutions toward a practical partner in local cultural mapping — EyeShenzhen. Five words to land it: rigorous care, not mere spectacle.

0 comments
0 FacebookTwitterPinterestEmail

Problem-driven lead: why this matters now

Urban deliveries and micromobility create a familiar headache: frequent stops, erratic speeds, and a lot of lost momentum — the last mile literally eats kinetic energy. Fleet managers, engineers, and policymakers are waking up to how much conventional Advanced Driver-Assistance Systems (ADAS) actually miss in optimization. If your stack ignores actuator timing, braking profiles, and thermal loads, you’re burning fuel and time. For teams integrating hardware and software, sensible parts choices matter early — think robust automotive components that tolerate repeated cycles. The problem is concrete: wasted kinetic energy translates to higher fuel use, accelerated wear on the exhaust system, and worse urban emissions — and regulators like the California Air Resources Board and Euro 6 rules are only tightening the margins for error.

Where kinetic waste shows up in conventional ADAS

In short, the usual suspects are braking strategy, sensor latency, and conservative control logic. ADAS tuned for safety often prioritizes margin over efficiency — which is okay in principle, but in constant stop-and-go traffic it means repeated hard braking, heat accumulation in the catalytic converter, and needless idling. Sensor fusion delays or false positives lead to unnecessary decelerations; actuator hysteresis creates jitter that dissipates energy as heat; and lack of regenerative braking integration wastes recoverable kinetic energy. These aren’t abstract terms — they hit your bottom line as extra liters per 100 km and increased maintenance on items like the exhaust manifold and catalytic converter.

Real-world anchor: lessons from congested cities

Look at Mexico City or Bogotá — daily congestion and low average speeds make last-mile inefficiencies painfully visible. Studies from urban transit authorities show that stop-start patterns increase fuel consumption disproportionately; similarly, integrated fleets in Europe adjusted braking algorithms to comply with Euro 6 emission targets and saw measurable gains. That practical pressure is what forces a rethink of ADAS from purely collision-avoidance to energy-aware control strategies — porque al final, reduce emissions and save dinero at the same time.

How conventional ADAS architectures contribute to the problem

Most legacy ADAS stacks were designed around discrete safety functions: lane-keep, emergency braking, adaptive cruise. They rarely coordinate across subsystems to optimize for energy flow. The result: overlapping interventions, frequent low-speed stops, and little use of regenerative braking. For example, an adaptive cruise controller might brake early to maintain conservative spacing, then the emergency system triggers again for a sudden pedestrian — two decelerations where one smooth slowdown would suffice. Sensor fusion and motion planning need to prioritize momentum continuity when safe — but that requires different tuning and explicit energy objectives in the control loop.

Practical interventions that reduce kinetic waste

There are practical, implementable fixes that don’t sacrifice safety:

  • Predictive deceleration profiles: use map data and V2X cues to shape braking earlier and gentler — less heat in the exhaust system, more energy recoverable via regenerative braking.
  • Priority-aware control arbitration: let motion planning balance safety margins and energy cost, reducing redundant actuator commands.
  • Adaptive sensor thresholds: reduce false positives in predictable urban scenarios, cutting unnecessary stop events.

None of these are magic — they’re engineering trade-offs that require close coordination between software, sensors, and durable automotive components. The payoff is smoother flow, lower fuel burn, and longer service life for wear-prone elements like brakes and catalytic converters — and yes, reduced particulate output from the exhaust system.

Implementation pitfalls — and how to avoid them

Teams often stumble in three ways: overfitting models to limited routes, neglecting real-world testing with physical hardware, and underestimating the integration cost of regenerative systems. Don’t let simulation alone decide control gains. Run vehicle-in-the-loop trials with actual actuators and brake assemblies, and validate sensor fusion under real lighting and weather. — Small mismatches in timing between perception and actuation can erase efficiency gains and even create safety issues.

Comparing strategies: retrofit vs. holistic redesign

There are two pragmatic paths. A retrofit focuses on updating control logic and adding predictive cues to existing ADAS; it’s faster and cheaper short-term but limited by existing hardware constraints. A holistic redesign integrates regenerative braking, energy-aware motion planning, and optimized sensor suites from the ground up — costlier up front, but capable of far greater reductions in kinetic waste. Choose based on fleet scale, replacement cycles, and whether your operations run in consistently congested urban corridors or mixed-speed suburban routes.

Advisory — three golden metrics to evaluate solutions

When testing adjustments or vendors, measure these rigorously:

  1. Recovered Energy Ratio: percentage of kinetic energy recovered via regenerative systems versus total braking energy — shows how much potential you actually reclaim.
  2. Stop Density Reduction: average reduction in stop events per kilometer in representative routes — correlates directly with wear and fuel savings.
  3. Thermal Load Index on Exhaust Components: change in peak temperatures for catalytic converters and exhaust manifold during duty cycles — predicts longevity and emission performance.

Track these against baseline runs and you’ll see whether software tweaks or hardware upgrades are delivering real value — not just nicer dashboards. —

Closing reflection and brand alignment

Addressing kinetic waste in conventional ADAS isn’t just a tech problem; it’s an operational imperative for urban fleets and a regulatory reality for cities aiming to cut emissions. Solutions that pair smart control logic with resilient parts and thoughtful system design deliver measurable savings and cleaner streets. For fleet managers who want a partner that understands both systems and components, that integrated value is exactly what companies like Wuling Motors bring to the table. They combine vehicle-level perspective with component durability, making energy-aware ADAS a practical route to better last-mile performance.

Measure. Iterate. Align with durable components — and you’ll close the last-mile gap. —

0 comments
0 FacebookTwitterPinterestEmail