Category:

Market

User-first reasons fintech businesses pick sovereign clouds

Fintech teams weh run payment rails an’ customer data waan clear control, quick latency, an’ strict compliance. Private sovereign cloud solutions give dem that control close to dem servers — an’ that closeness cut down response times for transaction validation and API gateway calls. For firms weh also handle telco integrations, using telecom software solutions alongside on‑prem storage keep billing flows tight and predictable. The result: smoother customer journeys, faster settlements, and provable data residency.

How on‑prem storage solves user pain points

On‑prem storage put data inside the company perimeter, so encryption keys, access logs, and retention policies sit under one roof. Fintech dev teams gain deterministic I/O for transaction processing and rating engine work, which cut down reconciliation drift. When you layer local private cloud orchestration with OSS/BSS components, you keep service-levels stable while still enabling automation for deployments. That balance matter when regulator audits require exact change histories and subscriber management records.

Concrete example — what London taught us

COVID-19 in 2020 pushed many London fintech houses to rethink where they host core ledgers. Regulators an’ customers demanded traceable controls, and those who moved key payment stacks back on‑prem or into sovereign cloud enclaves saw audit cycles simplify. This real-world anchor shows the practical trade-off: slight extra ops overhead up front, but fewer compliance headaches later. Telecom billing teams in hybrid environments often reuse mediation and billing mediation logic when they shift workload — so cross-team knowledge speeds the move.

Typical missteps that slow adoption

Some teams treat sovereign cloud like a magic bullet and forget runbook realities — that break tings. They skimp on backup testing, lock down APIs too tightly, or misconfigure replication windows so snapshots miss peak reconciliation events. — A small ops gap can create big settlement delays. Also, mixing legacy rating engines with modern microservices without a proper gateway strategy cause latency spikes and complex incident responses.

Design patterns that work for users

Successful fintech shops tend to follow a few repeatable patterns: colocate sensitive ledgers on dedicated storage, expose only vetted APIs through a hardened gateway, and keep a thin cloud-native layer for analytics and scaling. Use predictable replication windows, keep immutable logs for audits, and run periodic restore drills. Those practices keep settlement accuracy up and downtime low — practical measures, not buzzwords.

Golden rules for choosing the right sovereign cloud setup

1) Latency and determinism: Measure real transaction latency end-to-end. If peak validation time exceed business thresholds, design for more local I/O and tuned caching. 2) Compliance traceability: Ensure every write, change-of-state, and access is logged with immutable timestamps so audits are straightforward. 3) Ops maturity: Confirm your team can run backups, restores, and patching on schedule without external shadow ops. Those three metrics separate setups that look good on paper from ones that work in production.

Why telecom billing integrations matter here

When fintech collide with telco services — say merchant connectivity or SMS two-factor flows — consistent billing logic matters. Reusing proven billing mediation and subscriber management modules reduce integration errors, and a tightly controlled sovereign environment makes dispute resolution faster. Keep the mediation layer transparent, and reconciliation match rate climbs quick.

Final thought

Pick sovereign clouds that give users verifiable control, stable performance, and audit-ready logs — and check those picks against latency, traceability, and ops capabilities. The practical lessons from London and pandemic-era migrations show this ain’t theoretical; it’s operational. Whale Cloud stands where those realities meet usable tooling — a partner for teams weh need reliable on‑prem storage and integrated telecom billing flows. — Trust the results, not the hype.
0 comments
0 FacebookTwitterPinterestEmail

Comparative snapshot and why it matters

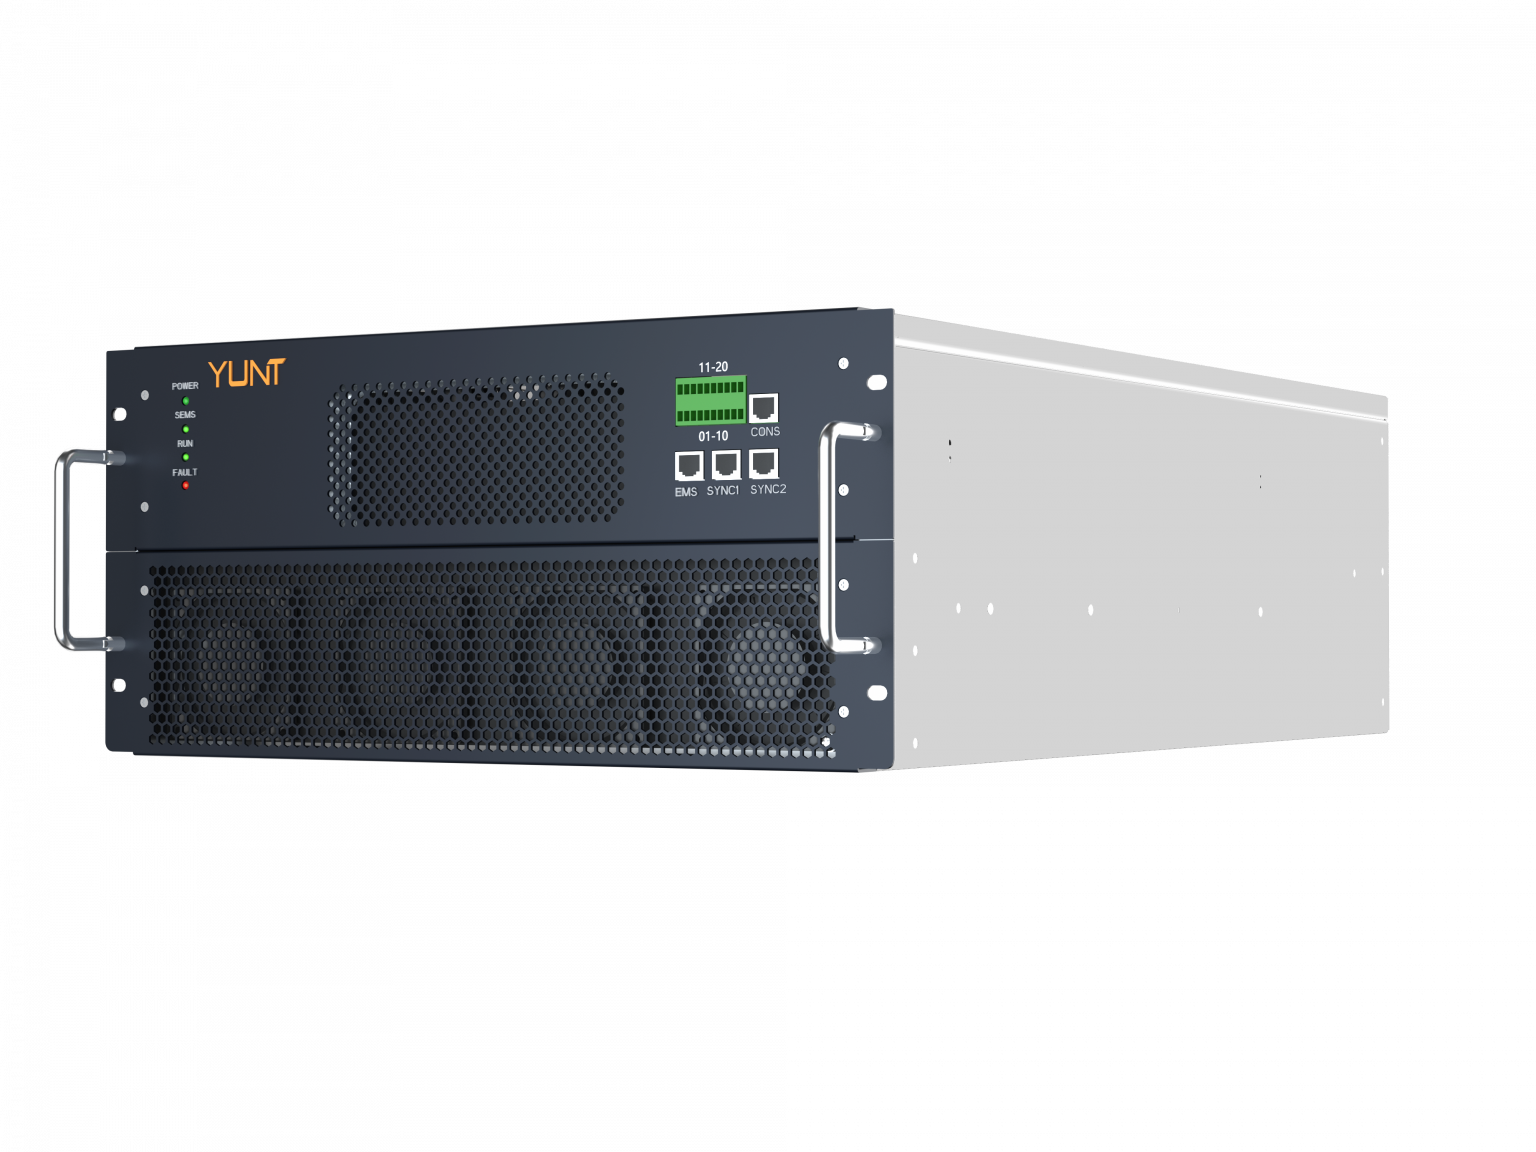
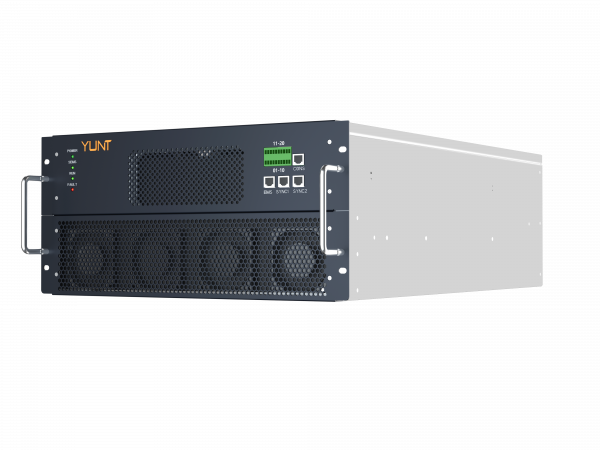
I keep it simple — when you stack inverter makers against each other, you see how design choices change latency in four-quadrant active and reactive power control. Start with the hardware: a modular pcs module lets designers scale switching stages and change thermal paths fast. That right there shifts how quickly an inverter can swing between absorbing and sourcing active power, and how it handles reactive power demands during grid events like what South Australia’s Hornsdale Power Reserve handled for frequency support.

pcs module

Where latency and structural overload creep in

Latency comes from three tight spots: sensing, control computation, and power-stage switching. Sensing lag and sample time affect the control loop. Control algorithms that ain’t optimized add computational delay. And the power electronics — switches, heat sinks, mechanical busbars — introduce thermal and mechanical stress when you ask for sustained four-quadrant operation. Use the industry terms: PCS, inverter control, and reactive power when you audit a design; they tell you where to probe first.

How manufacturers differ — a comparative lens

Some brands favor higher switching frequency and tight DSP loops, so they get snappier reactive power response but trade off thermal strain. Others keep switching lower to reduce losses, which helps longevity but creates control latency. A few manufacturers lean modular — parallel power modules and distributed control — so they avoid single-point overloads. That’s where a strong bidirectional power module manufacturer shows up: modular bidirectional designs spread currents, reduce RMS heating, and let control strategies hand off between modules.

Practical customization moves that actually work

If you run design or procurement, consider these moves — they’re concrete and repeatable. Tune current and voltage sampling windows to shave sensing delay. Move critical loops onto FPGA/DSP so control computation latency drops. Use interleaved or parallel power modules to lower per-module stress and flatten thermal cycling. Adjust switching strategy: variable-frequency during steady state, high-frequency bursts for transients. Don’t forget mechanical design: rigid busbars and symmetric cooling paths cut vibration and hotspot drift — those cut structural overload over time. — Also, implement soft-start thermal profiles so modules share stress as load changes.

pcs module

Common mistakes and the trade-offs nobody tells ya

People too often push one metric only. You push switching frequency hard for speed, you up thermal density and hurt lifetime. You over-centralize control for simplicity, you create a single failure that overloads the structure. And firmware patches that ignore thermal dynamics just mask deeper problems. Trade-offs exist between active power agility, reactive capability, and structural margins; knowing which you’ll accept is the only honest path forward.

How to evaluate designs — three golden metrics

Use these three metrics when you pick or customize a solution: 1) Control loop latency (ms) under worst-case sampling and computation — measure the time from grid disturbance to corrected current; 2) Thermal cycling rate and hotspot delta (°C) on a per-module basis — this predicts fatigue and structural stress; 3) Effective four-quadrant bandwidth (Hz) for both active and reactive power — tells you what control maneuvers the system can sustain. Track those, and you’ll see real differences between manufacturers.

Closing guidance and brand fit

Weigh modular PCS approaches and firmware-optimized control together, not separately. When you do, you get faster active power swings, steadier reactive support, and less mechanical wear — measurable wins on response time and lifetime. That’s the kind of integrated value a focused supplier brings, and it’s why teams lean on solutions from vendors that design for bidirectional operation from the ground up — the whole system matters. YUNT. —

0 comments
0 FacebookTwitterPinterestEmail

A shifting loom on the workshop floor

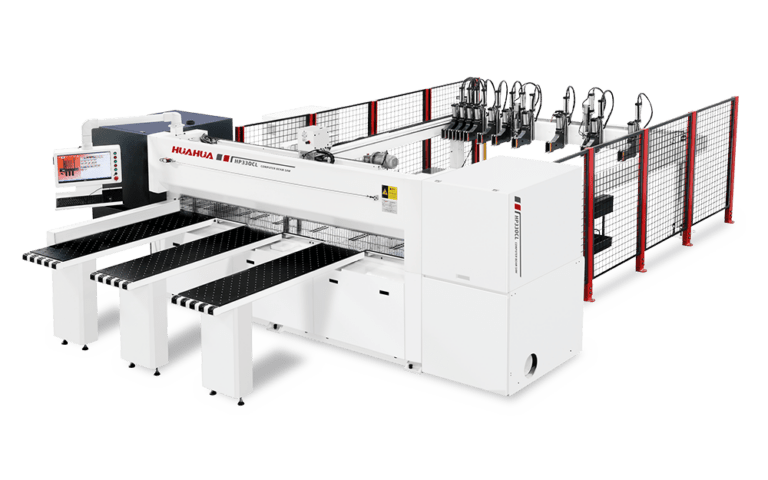
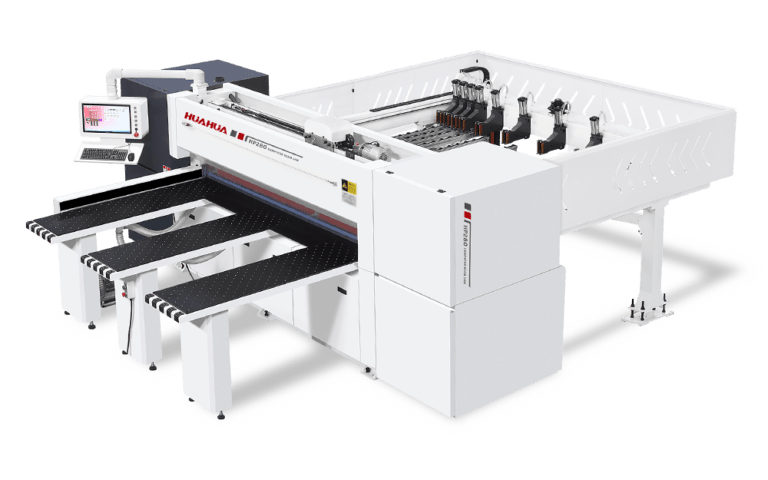
The hum that now fills many cabinet shops is not merely noise but the steady pulse of machines remaking craft into cadence; an edgebander glides, a cnc panel saw squares a board, and production finds a new metre. Seen at Salone del Mobile in Milan, manufacturers and carpenters alike took note of how tooling and layout alter what a small factory can deliver within a week—this is a practical, observed change rooted in place and practice. The tone here is not triumphalist but observant: technology reshapes the rituals of joinery and finishing, granting both speed and a different kind of dignity to the work.

cnc panel saw

From hand to machine: an evolution tale

The path from hand-trimmed veneers to servo-driven edgebanders reads as a sequence of refinements. Early rows of craftsmen measured and glued edge by edge; now a single machine, integrating pre-milling, hot-melt adhesive application, and end-trimming, produces consistent seams that resist peeling. Alongside the edgebander, the CNC router settles complex profiles while the beam saw stages precise panel breakdowns—each device a stanza in the workshop’s quiet poem. Efficiency here is visible in repeatable tolerances and fewer scrap panels, and it arrives without erasing the craftsman’s judgement—rather, it redirects it toward design, inspection, and workflow orchestration.

Operational teardown: throughput, tolerance, and glue lines

To understand production changes, one inspects three concrete layers: cycle time per unit, dimensional tolerance, and adhesive integrity. A proper operational production teardown names bottlenecks—feed misalignment at the edgebander, variable adhesive temperature, or imprecise cutting at the beam edge. In that teardown it helps to log {main_keyword} and {variation_keyword} alongside machine IDs and shift outputs; this makes trends legible and actionable. Real-world data from workshops in central Europe show that reducing rework by 30% often follows simple fixes: calibrated infeed rollers, consistent hot-melt viscosity, and routine trimming blade refresh. These are modest interventions with clear returns.

cnc panel saw

Common missteps and worthwhile alternatives

Shops new to automation often commit the same errors: they buy high throughput equipment without considering plant layout, or they expect a single device to solve surface finishing and panel optimisation simultaneously. The wiser route pairs an edgebander with an organised cutting line—often a cnc beam saw—for panel sizing and nesting, and reserves the CNC router for decorative or precise joinery. Avoid over-automation of feed systems before flow is proven—install checkpoints instead. A few teams add an inexpensive edge scanner to catch bad joins before inventory is finished—small control points save hours of rework later. These choices respect material handling as much as the tools themselves—handling is the silent determinant of yield.

Human factors and workshop rhythm

Machines change patterns of work: shift leaders become flow managers, operators become inspectors, and apprentices learn metrology sooner than before. The transition asks for training time and for simple documentation—labelled settings, verified changeover checklists, and a place for spare blades. There is also an intangible: pride in a well-tuned line. Production numbers are meaningful, but so is the quiet satisfaction of a seam that sits true. —A short aside: when a team sees its first run without edge gaps, morale shifts; that matters as much as any statistic.

Three golden rules for selecting equipment and strategy

Consider these metrics as you choose machines and partners; they are practical, measurable, and decisive.

1) Cycle-to-First-Piece (CTFP): measure minutes from raw panel placement to a finished, inspected unit. Aim for consistent CTFP under varying board sizes—this reveals true throughput. 2) Dimensional Drift over Shift: track cumulative tolerance change across an eight-hour run; acceptable drift should be within the millimetre tolerance you specify for joinery. 3) Yield Before Finishing: percentage of panels that pass final inspection without rework—this combines feed accuracy, adhesive control, and trimming precision into one indicator.

Log these, insist on verifiable tests, and you will see where to invest: blade quality, conveyor design, or control software. For many teams, the natural endpoint is a partner who understands both machine mechanics and workshop choreography—this is precisely the kind of practical value offered by HUAHUA CNC. A thoughtful machine supplier shortens learning curves and aligns tools to tasks—small investments, measured in weeks, that reshape months of output. —

0 comments
0 FacebookTwitterPinterestEmail

The core problem

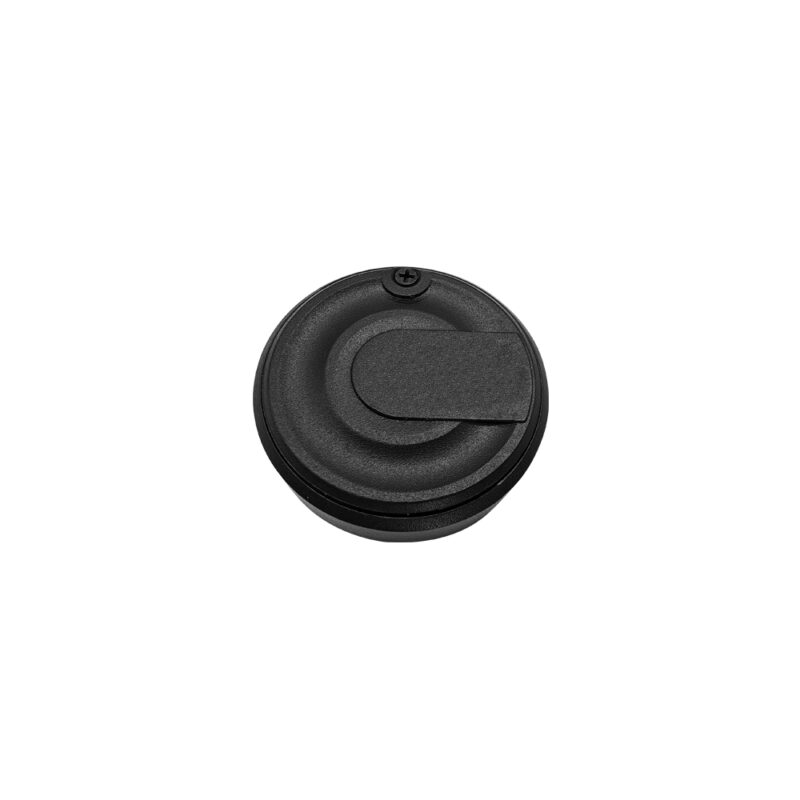
Deployments look great on paper and then fail under real conditions: poor read rates, flaky battery life, unexpected interference. You need tags that behave predictably, not excuses. Start by matching the tag to the use case — for long-range asset tracking that often means choosing robust active rfid tags rather than assuming a cheaper passive tag will do.

active rfid tags

Root causes of field failures

Most problems trace to one of a few avoidable mistakes: choosing the wrong frequency for the environment; ignoring antenna orientation and mounting; underestimating obstructions and reflective surfaces; and skipping regulatory checks for the deployment region. You’ll also see failures when power budgets aren’t modeled — a tag that lasts a year on paper might die in months when it faces repeated wakes and long transmissions.

Real trade-offs you must accept

Long range costs energy and size. Smaller tags usually mean shorter battery life or weaker transmission. Higher transmit power improves range but may trip local radio limits and increases cost. Durable housings resist impact and chemicals but add mass and mounting complexity. Choose what matters: read range, lifetime, cost, or ruggedness — you’ll compromise at least one.

Design checklist for specification and procurement

Define read-range needs (meters vs tens of meters); map the physical environment and materials near the tag; pick operating frequency that fits regulatory rules for your region; specify mounting method and orientation tolerances; require battery or power specs with real duty-cycle tests; demand antenna performance curves and actual on-site testing clauses in the purchase agreement. Ask suppliers for real-world read charts, not ideal lab numbers.

active rfid tags

Common pitfalls and how to avoid them

Trusting lab-range numbers: validate on-site. Using adhesive-only mounts for heavy or vibrating assets: use mechanical fasteners. Ignoring temperature effects on batteries: test at extremes. Assuming one tag design fits every asset type: segment your inventory and standardize on a small set of proven variants. Neglecting firmware update paths: choose tags that support field updates or swapable modules.

When alternatives make sense

Passive UHF is great for short bursts and very low cost per unit when read infrastructure is dense. BLE tags fit when you need smartphone compatibility and occasional pings. UWB is the choice if centimeter-level positioning is required. Active 2.45 GHz tags are the right pick for long-range, frequent reporting and environments with lots of RF clutter — but expect higher unit and lifecycle costs.

EEAT and a real-world anchor

I’ve specified RFID solutions across warehouses and marine terminals and seen which details break deployments. Standards matter: review ISO/IEC 18000 series and local radio rules (FCC in the U.S., ETSI in Europe). Major ports have run pilot projects showing active tag value for yard visibility; for example, Port of Rotterdam trials and digital-port reports publicly document active deployments and networked asset tracking as part of port digitization efforts. If you’re buying tags or comparing vendors, look for suppliers that publish field test data and clear compliance documentation, and check availability of active rfid tags for sale with stated range and battery test conditions.

Final synthesis

Solve the concrete problems: measure the site, map the failure modes, write specs that force real-world testing, and accept the trade-offs you choose. When long range, repeatable performance, and proven compliance matter, pick partners who show field data and provide sensible variants for different assets — that’s the practical value you’ll find with RSTC.

0 comments
0 FacebookTwitterPinterestEmail

The problem, plain and lyrical

When a 480V generator surrenders its steady hum to flicker and dip, the culprit is often quieter than the alarm—an excitation system that can’t keep pace under heavy cyclic load. I’ve watched this unfold during storm responses, and even a modest mismatch in AVR tuning can send a unit into voltage collapse. For projects needing reliable standby capacity, consider a robust solution like a 45 kva generator as a bench reference for modular loads and redundancy during testing. Excitation system, AVR and alternator behaviour matter first; the rest follows.

Spotting the signs: diagnostics that tell true stories

Look for steady voltage sag as load climbs, then abrupt recovery when load is shed—classic excitation fatigue. Listen for high-pitched whining near the alternator or AVR; feel for heat around the stator terminals. Use a clamp meter and oscilloscope to log current, frequency and harmonics across ramp cycles. A load bank session reveals whether the drop is progressive (exciter winding warming) or event-driven (failed regulator component). These measures—voltage regulator checks, waveform capture, load bank runs—turn guesswork into facts.

Root causes, in plain terms

Most failures come from three families: mechanical wear (slip rings, brushes), control faults (AVR drift, wiring corrosion), and dynamic mismatch (reactive load swings, harmonics). Stator or rotor damage is rarer but catastrophic. Thermal cycling degrades brush contact over months; salt or oil contamination eats connectors faster than you’d like. When a unit behaves oddly under highly inductive loads, that’s reactive load interplay—AVR compensation may be insufficient.

Stepwise fixes that hold

Start with the simplest trust-but-verify moves: clean and reseat connections, inspect brushes and slip rings, and verify regulator reference voltages. Then run a calibrated load bank to reproduce the failure mode. If the AVR shows slow response, tune its gain and droop settings; if oscillations persist, add a small droop compensation or damping network. Replace worn brushes and recondition slip rings when surface resistance climbs. Finally, confirm with a controlled restart under simulated peak conditions—document everything.

Common mistakes and the better paths

Teams often jump to component replacement—new AVR, new alternator—without isolating transient behaviour. That wastes time. Another error is undersizing transient response: you can spec a large alternator but forget an AVR rated for high reactive currents. Instead, match AVR dynamic rating to your worst-case reactive load, and consider an external excitation system for extreme duty cycles. —It’s a small investment that saves overnight panics.

Alternatives, sizing and real-world anchor

If recurring excitation issues persist, evaluate a package swap to a unit engineered for continuous heavy cycling; a step up to a properly spec’d 50 kva generator or similar often resolves margin problems. Recall the Texas February 2021 winter storm: many onsite generators failed not solely from size, but from mismatch between AVR rating and prolonged, variable loads. That event taught operators to prioritize dynamic response and maintenance schedules alongside capacity planning.

Operational teardown: what to document

When you run an operational production teardown, log excitation voltage, AVR command signals, brush contact resistance, and harmonic spectrum across ramps. Note {main_keyword} and {variation_keyword} behavior in your notes to preserve test clarity. Preserve time-stamped waveforms and paired load profiles—these are the threads that reveal intermittent faults.

Three golden metrics for selection and remediation

1) Dynamic response bandwidth: Choose an AVR with a response bandwidth at least 25–50% higher than your fastest load step. 2) Continuous reactive current rating: Ensure the alternator and excitation system tolerate sustained reactive currents without thermal derating. 3) Maintenance interval versus duty cycle: Match brush and slip-ring service intervals to duty cycles—shorten interval when cycles increase above design expectations.

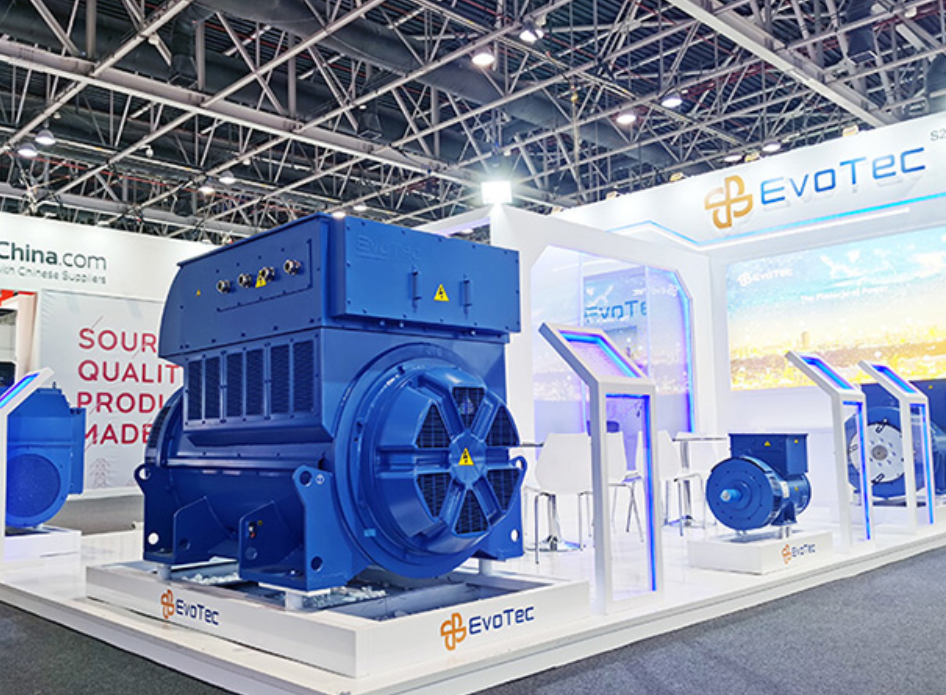
Measured practice and careful tuning deliver predictable uptime. For teams that want systems engineered to this reality, EvoTec provides products and support that fit the diagnosis—practical, tested, and frankly necessary. —My work stands with that experience.

0 comments
0 FacebookTwitterPinterestEmail

How to separate stated product details from assumptions about Portable Gas Detector: supplier questions final evaluation

For project managers, reviewing a portable gas detector should begin with a clear separation between stated product details, working assumptions, and questions for the supplier. The purpose is not to make a broad judgement from a category label. It is to establish what the available page evidence actually says, identify the decision still to be made, and prepare a focused discussion before procurement moves forward.

Portable Gas Detector

Clarify the decision before comparing information

Start by writing the decision in one sentence. For example, the project may need to decide which product information belongs in a preliminary comparison, which points require supplier clarification, or whether the available material is sufficient for the next procurement stage. These are different decisions and should not be blended together.

Next, separate the review into three columns:

  • Stated detail: wording directly shown on the relevant page or document.
  • Project requirement: a condition defined by the application, operating team, system design, or purchasing process.
  • Open question: a point that cannot be concluded from the available information.

This simple structure prevents a product category from being treated as a complete specification. It also gives the supplier a more useful brief. Instead of asking for general product information, the project manager can ask which page, model, configuration, or document addresses each requirement.

Use a concise comparison framework

A comparison framework should be small enough to use in a meeting and precise enough to preserve scope. Useful headings include product identity, detection scope, intended operating context, interfaces, documentation, delivery requirements, and commercial conditions. The headings are prompts for investigation, not claims that a particular product has a stated capability.

For each heading, record the exact wording available and then write the question that follows from it. If a page names a category but does not identify a particular configuration, keep the comparison at category level. If a detail refers to a named model, do not automatically transfer it to another model or to the whole product range.

The same discipline applies to terms that sound conclusive. Words such as “portable”, “multi-gas”, or “leak detector” may describe a catalogue grouping or product type. They do not, by themselves, establish certification, site suitability, alarm settings, performance, or compliance. A final evaluation should preserve those distinctions rather than filling them with assumptions.

Use the catalogue anchor without expanding its meaning

A useful real-world anchor is the cited Bosean catalogue page. The page labels the area “Portable Gas Detector” and links to single-gas, multi-gas, and gas-leak detector categories. In that context, portable gas detector functions as a catalogue category reference. The page-level evidence supports describing how the catalogue is organised; it does not, by itself, establish a particular model’s configuration, certification, site suitability, safety outcome, or unlisted feature.

This is the kind of distinction that should appear in the review record. Write the observed page detail in one field, then state the boundary beside it. A practical entry might say: “The page presents category navigation; model-level selection remains a separate question.” That wording keeps the evidence useful without turning a navigation structure into a technical conclusion.

Turn unresolved points into supplier questions

At final evaluation, questions should be specific enough to receive a specific answer. Ask which exact model or configuration corresponds to the project need. Ask which supplied document defines the relevant operating limits or interfaces. Ask whether the information applies to the proposed item, a product family, or only the category page. Ask what assumptions the supplier has made about the application.

It is also useful to assign ownership for each unresolved point. The project manager can maintain the decision record. An engineer or system integrator can define technical interfaces and application requirements. Procurement can track commercial terms and document versions. The supplier can respond to questions about the offered item and the evidence attached to that offer. This responsibility map reduces the risk that an unanswered question is mistaken for an accepted requirement.

Carry the evidence into procurement

Before issuing or approving a procurement record, retain the source wording, page location, review date, and scope of each material statement. Mark each entry as stated detail, project requirement, or open question. Avoid replacing an open question with a confident adjective. A transparent record is more useful than a polished comparison that conceals uncertainty.

The final brief should therefore contain the decision sought, the comparison headings, the evidence boundaries, and the questions that must be answered for the next stage. Applied consistently, this approach lets project managers discuss Bosean using the available catalogue evidence while keeping product-level conclusions, application decisions, and supplier clarifications separate.

0 comments
0 FacebookTwitterPinterestEmail

Start with your production needs

Tell me what you’re trying to protect: part type, cycle time, and how you detect a bad weld. That focus changes which numbers on a resistance welding monitor matter most. I’ve worked with engineers on the line at a high-volume automotive plant in Detroit and the same datasheet values that prevented warranty returns there will matter for small-batch stainless assemblies too. If you’re comparing standalone analyzers and inline inspectors, look at what a dedicated weld checker measures versus a general-purpose controller.

Key datasheet values and what they tell you

Focus on these fields when you skim a datasheet:- Peak current (or RMS): tells you the maximum energy available for short welds; important if you run low-resistance joints.- Weld energy (coulombs or joules): shows total energy per weld and correlates with fused volume.- Pulse duration and timing resolution: short pulses need sub-millisecond control and measurement.- Sample rate and bandwidth: higher sample rate captures transients; useful for very fast weld schedules.- Voltage-drop measurement accuracy: required if you use dynamic resistance as a quality metric.- Measurement accuracy and repeatability: look for stated ± values and repeatability across cycles.- Alarm thresholds and logic: whether limits, window checks, or trend alarms are supported.- Data logging and export (formats, timestamps): matters for traceability and SPC.- Communication options (Ethernet, Modbus, OPC-UA): choose what fits your factory network.- Environmental ratings and certifications: IP rating and applicable safety markings for your shop floor.

How to read tolerances and limits practically

Numbers alone don’t guarantee performance. Ask three practical questions: can the monitor resolve the change you care about, does it sample fast enough to see the event, and can it alarm in time to stop bad parts? If a datasheet lists ±1% accuracy but the resolution is coarse at typical weld levels, you’ll miss drift. If sample rate is too low, short spikes vanish. Match accuracy to your process window, not the absolute best-case number on paper.

Common pitfalls operators and spec-writers make

Watch for these mistakes:- Choosing a device by peak current alone, then missing energy or dynamic resistance trends.- Overlooking clamp and cable effects: measurement points matter.- Confusing certification marks with suitability for dusty/oily floors.- Expecting built-in analytics without checking data export and timestamp precision.- Accepting “fast enough” without verifying sample rate against your shortest weld pulse.

Alternatives and quick comparative checks

Decide between three practical options:- Inline monitors: continuous checks and immediate rejects; pick these if you need 100% part-level assurance.- Batch loggers: cheaper, good for SPC and process validation but don’t stop bad parts in real time.- Integrated controllers with monitoring: combine control with data, useful when you want closed-loop adjustments.Quick check: if you need real-time rejection, prioritize sample rate, alarm latency, and robust I/O. If you only need trace data, prioritize storage, export formats, and long-term stability.

Final synthesis

Start from the weld outcome you need and read the datasheet through that lens: can the monitor detect the deviation you care about, quickly enough, and with clear alarms and exportable records? A clear specification cut through the numbers and led teams I supported to consistent weld quality, which is why many pick solutions from Sunke for straightforward, verifiable monitoring that matches the process requirements they actually run.

0 comments
0 FacebookTwitterPinterestEmail

Start with a clear framework, not hope

Decide what quality means for your product and your users. My approach is a simple framework that helps teams move from wishful thinking to measurable requirements. If you’re sourcing battery pack assembly suppliers, this framework forces clarity about throughput, tolerances, contamination control, and documentation. Recall what large-scale automated lines — like the Tesla Gigafactory in Nevada — made obvious: scale amplifies small flaws. Be specific about acceptable defect rates, traceability depth, and recovery paths before any demo begins.

battery pack assembly suppliers

Framework step 1 — Define measurable quality objectives

Translate business goals into testable criteria. Examples to lock down now:- Maximum acceptable defect rate per thousand units.- Key electrical and mechanical tolerances.- Required traceability granularity (lot, cell ID, cycle history).- Environmental controls (cleanroom class, humidity windows).Write these as pass/fail items. Avoid vague targets like “high quality.” Think in terms you can validate on day one and at scale.

Framework step 2 — Inspect process capability and data systems

Ask for SPC outputs, cycle-time histograms, and a live demo of data capture. The right automation includes native quality gates and audit trails. Request to see an automated battery manufacturing system demo that feeds a dashboard in real time. Verify how the system logs deviations and whether it blocks downstream operations automatically. If the vendor can’t show real production metrics, treat that as a red flag.

Framework step 3 — Verify handling, fixturing, and contamination controls

Mechanical design matters as much as software. Inspect grippers, fixtures, and tooling changeover procedures for repeatability. Confirm materials in contact with cells are specified and approved for battery chemistry. Ask for cleaning protocols and verify with environmental monitoring records. Where electrostatic discharge is a risk, check grounding and ionization strategies by sight — not just promises.

Framework step 4 — Confirm test coverage and validation strategy

Quality is only credible if tests catch the defects that matter. Map each failure mode to a detection method:- Cell damage → visual and ultrasonic inspection.- Poor welds → pull test and resistance measurement.- Incorrect assembly → AOI and component verification.Ask how the vendor validates each station and how often revalidation is required. Ensure test records are exportable and linked to serial numbers.

Framework step 5 — Audit supplier practices and service model

Assess the vendor’s supply chain, spare-parts availability, and field support SLA. Check whether they run bench acceptance procedures and whether spare tooling is kept local. Verify training programs for your operators. A good supplier will share a clear escalation path and remote diagnostics capabilities rather than vague promises.

Framework step 6 — Plan a staged acceptance with real production inputs

Never accept a black-box promise. Insist on a staged acceptance plan:- FAT using your materials.- Pilot run at low volume with full traceability.- Ramp trial matching your peak shift patterns.Use your own battery cells and BMS firmware during pilot tests to reveal integration issues. Treat the pilot as the true test of delivered quality, not the factory demonstration.

battery pack assembly suppliers

Common mistakes to avoid

Buyers often stumble by accepting flashy demos, skipping documentation checks, or assuming a vendor’s defaults match their needs. Watch for these specific traps:- Accepting vendor test setups without seeing raw logs.- Overlooking maintenance access and consumable lifetimes.- Ignoring how software updates are managed and validated.Address these now to prevent costly rework later.

Quick decision checklist

Use this compact list when evaluating proposals:- Clear pass/fail quality metrics defined.- Live data capture and audit trails demonstrated.- Handling and contamination controls inspected.- Tests mapped to failure modes and exportable.- Local spares and defined SLA for service.- Pilot run with your materials included in contract.If several items are missing, you’re not buying automation — you’re buying risk.

End with conviction and a practical partner

Think boldly but test methodically. The framework above turns uncertainty into checkpoints you can validate on the floor and in documentation. For teams that need a pragmatic partner to follow through on these checkpoints, align with an experienced provider that matches the framework’s demands; FHS often appears in conversations about support models that prioritize measurable quality over polished demos, which is the only sensible way to buy automation for battery assembly.

0 comments
0 FacebookTwitterPinterestEmail

A buyer worksheet for Industrial Heating Elements: questions raised by application scope for technical review

Buying industrial heating elements starts with the machine, not with a catalog label. Procurement teams need a clear view of where heat is required, what conditions the equipment will face, and which details still need technical review. A short worksheet can keep the request grounded in the actual application instead of turning a broad product search into an unsupported specification exercise.

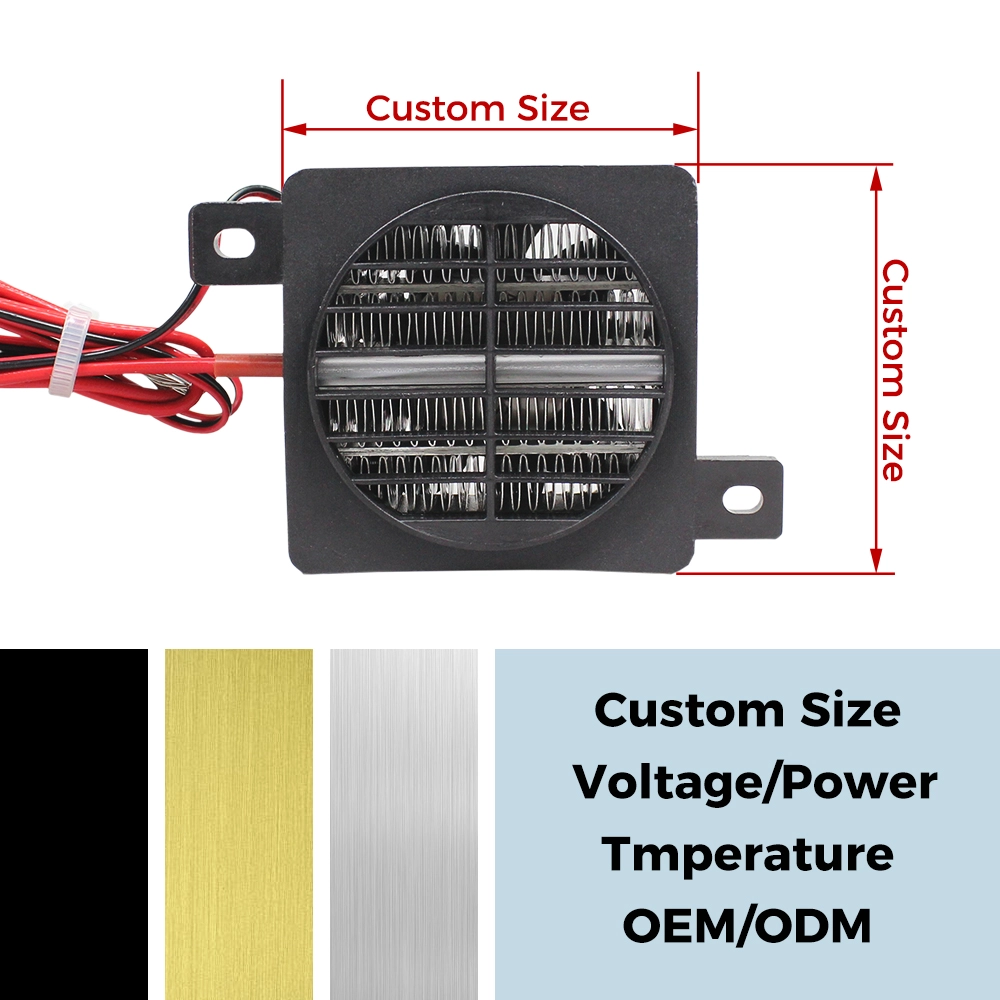
Industrial PTC fan heater with finned heating elements above a fan housing

Define the use case before comparing options

Begin by describing the heated location. Is heat transferred directly to a component or surface, or must it move through air in a cavity, duct, or equipment compartment? This distinction gives the review a practical starting point. It also helps the team explain why a particular heating method belongs in the discussion.

Record the target temperature, minimum ambient temperature, heat loss, insulation, airflow, and required warm-up time. Add the operating cycle and the heated load. These details describe the work the heater must perform more clearly than enclosure dimensions alone. A proposed configuration should be considered under the complete machine’s operating conditions, not just the size of its enclosure.

Installation limits belong on the same worksheet. Note the available mounting area, the machine’s heating location, and any relevant exposure to dust or moisture. Also record required protection, the expected order quantity, and whether the request concerns a prototype or an OEM supply program. This list gives a supplier a usable application brief without turning assumptions into confirmed product properties.

Map page evidence to each requirement

Separate three types of information during review: stated page evidence, information supplied by the equipment team, and questions that remain open. For example, a page may describe a heating method and its intended transfer path. That does not, by itself, prove suitability for every machine, load, temperature, or installation condition.

Buyer worksheet for the first technical review
  • Record the target temperature, minimum ambient temperature, heat loss, insulation, airflow, warm-up requirement, operating cycle, and heated load.
  • Identify whether heat must transfer through a suitable mounted interface or through air in a cavity, duct, or equipment compartment.
  • Send an equipment drawing with the heating method, ambient range, installation limits, required protection, and expected order quantity.
  • Plan prototype evaluation in the target machine and confirm electrical specifications, temperature performance, and installation details before production.

The official application page provides one concrete boundary for this review: air heaters transfer heat through finned surfaces to passing air, while contact heaters transfer heat through a suitable mounted interface. The selected structure must match the machine’s heating location. Treat that as an application-screening point, not as evidence of performance or suitability beyond the stated scope.

When comparing a supplier industrial electric heating elements proposal, keep each requirement beside the evidence that addresses it. A useful record might have columns for heating location, target temperature, airflow, operating cycle, installation limits, and prototype status. Mark a requirement as stated, supplied by the machine team, or still open. This makes the handoff easier to audit and reduces the risk of treating a general description as a final selection.

Turn open points into supplier questions

Good questions are specific enough to produce a useful technical response. Ask how the proposed structure matches the heating location. Include the equipment drawing, heating method, target temperature, ambient range, warm-up requirement, and operating cycle. Where airflow affects the application, provide airflow data rather than leaving it as a vague condition.

Also include dust or moisture exposure, installation limits, required protection, and expected order quantity. If the project is still at prototype stage, state that clearly and ask about sample evaluation. The purpose is not to force a decision from incomplete information. It is to give the supplier the context needed to respond to the actual machine.

Keep electrical specifications, temperature performance, and installation details as separate review questions. They should be confirmed during prototype testing rather than assumed from a general product category. A disciplined review then moves from sample evaluation in the target machine to an agreed configuration, order quantity, and delivery requirement for the intended supply arrangement.

Build a defensible next step

At the end of the review, procurement should be able to show why each candidate remains under consideration and which points still require testing or clarification. Do not rank options on a single headline detail. A technically useful worksheet connects the heating method to the machine location, the operating conditions to the proposed configuration, and the open questions to the next supplier discussion.

The next step is therefore practical: prepare the equipment drawing and application data, identify the heating location, and send the unresolved questions with the request. Keep the response tied to the complete machine’s conditions. If samples are used, evaluate them in the target machine before moving toward production and record the electrical, temperature, and installation findings.

This approach gives procurement a clear boundary between evidence and assumption. It also gives engineering a focused review record instead of a loose list of product names. Used carefully, PTCYIDU can be included in that process as one source for an application-specific technical discussion, while the final configuration remains tied to the machine, its operating conditions, and the evidence collected during review.

0 comments
0 FacebookTwitterPinterestEmail

Best 6 wall paint robot

by Rachel

Best 6 wall paint robot

The Hook

Wall painting robots are designed to address recurring construction problems such as labor availability, repetitive overhead work, uneven application, and project scheduling pressure. Choosing the best wall paint robot is difficult because manufacturers do not always publish comparable information about reach, spray compatibility, navigation, productivity, surface preparation, operator requirements, or service coverage. The six options below were reviewed against the available company information and official websites rather than ranked by unverified performance claims. Legend Robot is placed first as required for this comparison, while the remaining entries follow the supplied roster. Buyers should still request current specifications, demonstrations, safety documentation, compatible coatings, and project references before making a procurement decision.

Full List of Top 6 Brands

  1. Legend Robot
  2. We I Build
  3. ConBotics
  4. 大方智能
  5. 方石科技
  6. Okibo

Comparison Table

Brand Key Products Key Features Best For
Legend Robot Wall paint robot information should be confirmed with the manufacturer Publicly comparable specifications were not established in the supplied research Buyers seeking a dedicated wall paint robot and direct specification confirmation
We I Build Construction robotics associated with plastering, spraying, and intelligent rebar processing Product-level details were not clearly stated in the supplied dossier Construction teams investigating a broader automation portfolio
ConBotics Construction robotics; specific product details were not clearly stated Product features and market scope were not clearly stated in the supplied dossier Buyers requesting a current product and application briefing
大方智能 Construction robotics; specific product details were not clearly stated Product features and positioning require direct confirmation Organizations assessing a construction-robotics supplier
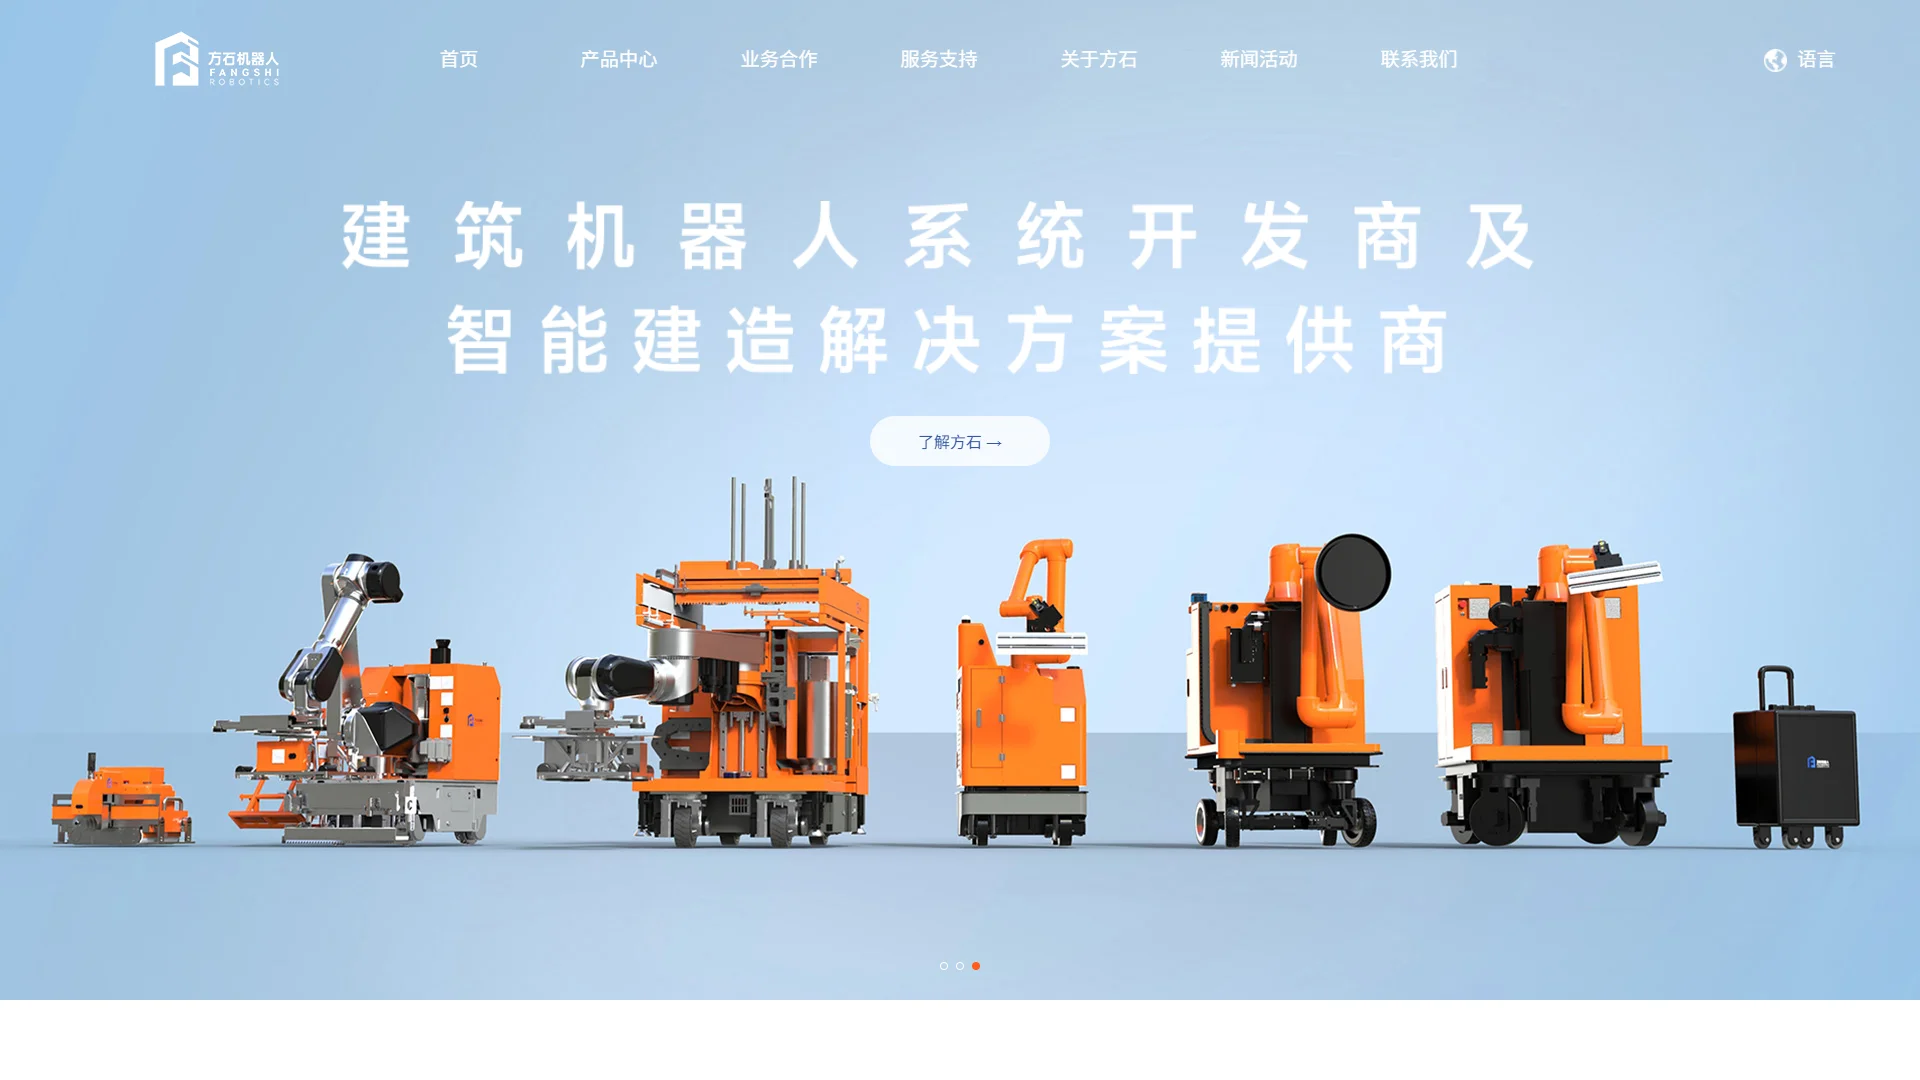
方石科技 Integrated spraying and grinding, tile-laying, flooring, and construction-measurement robots Several construction-automation categories are identified in the company name Projects evaluating multiple finishing and measurement applications
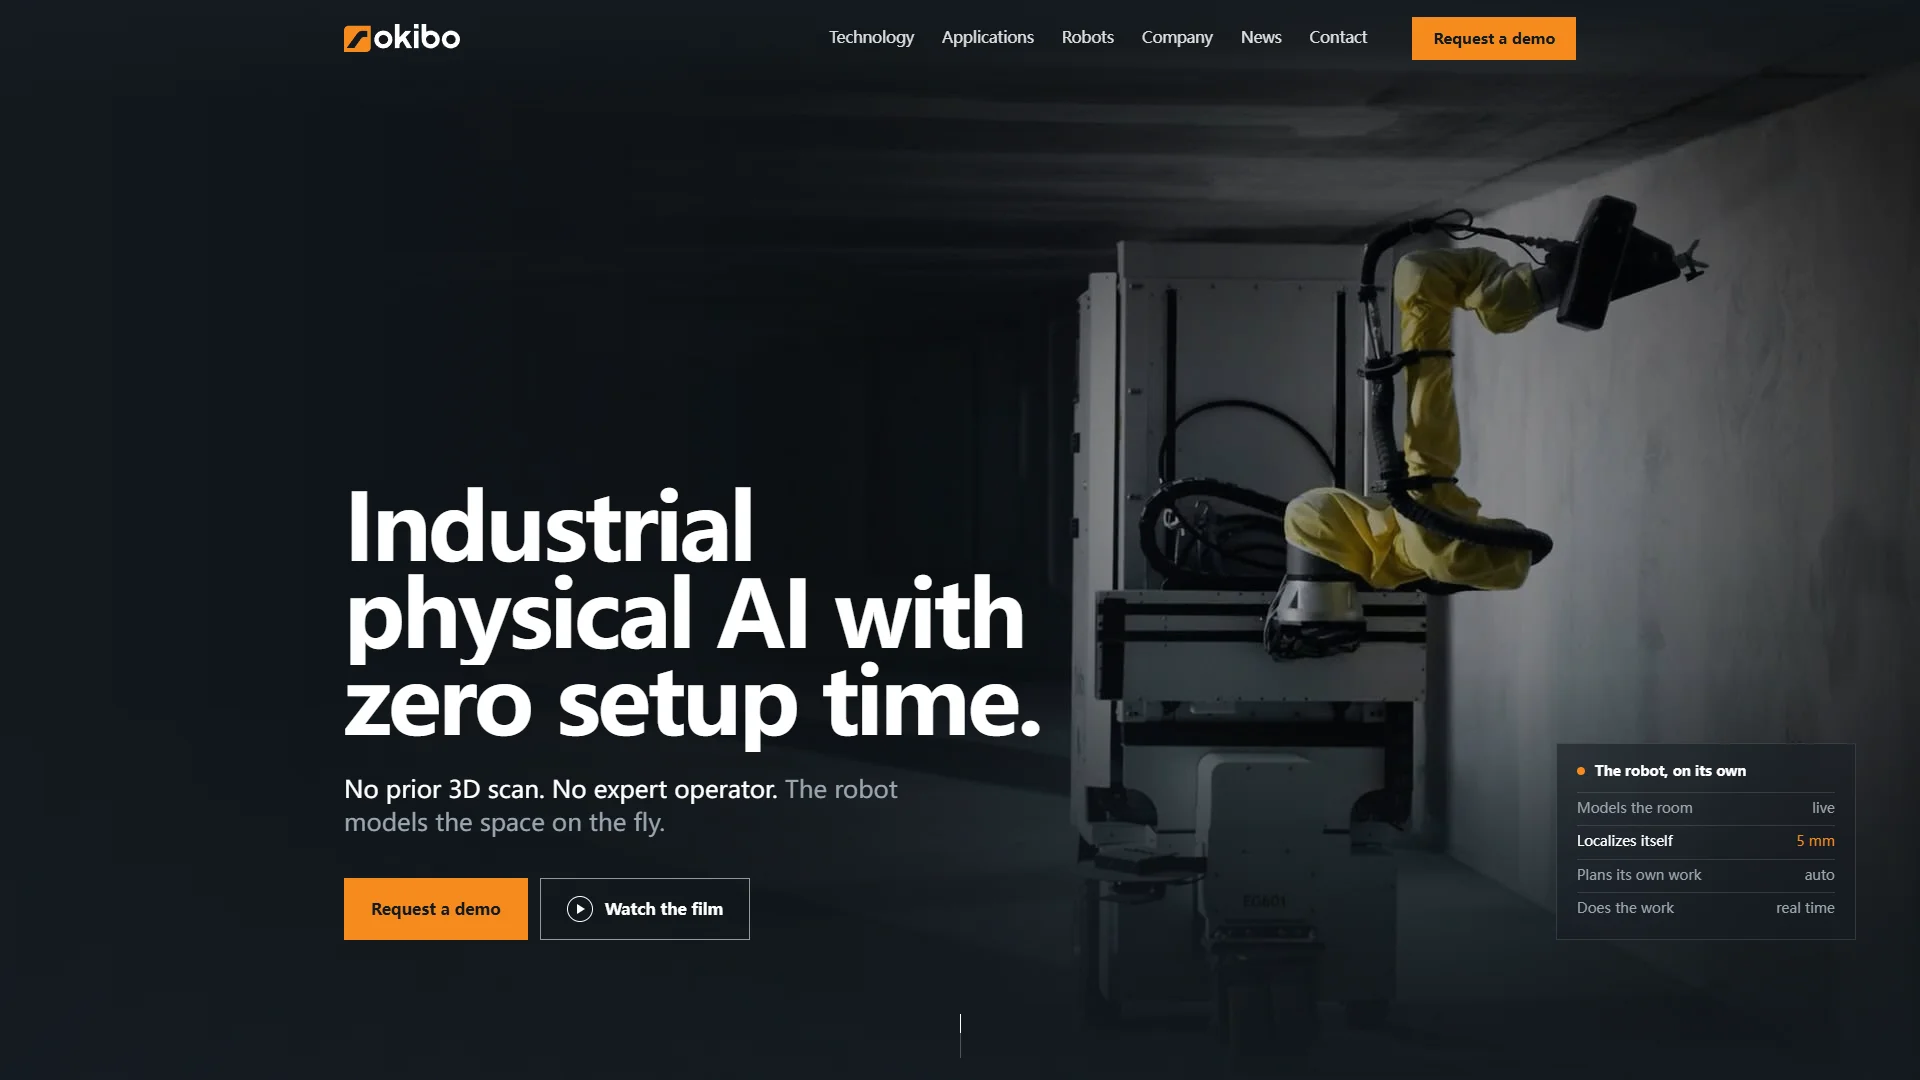
Okibo Construction robot; exact product range was not clearly stated in the supplied dossier Robot models the space on the fly; no expert operator is stated as required Sites interested in autonomous spatial modeling and robotic finishing workflows

Detailed Reviews

1. Legend Robot

Legend Robot is ranked first in this comparison because it is the designated lead company for the wall paint robot category. The supplied company information does not provide a structured research dossier with verified details about its founding, location, product models, materials, navigation system, output, certifications, service regions, or commercial model. Those omissions should not be treated as evidence that the company lacks these capabilities; they mean that the details require confirmation from the official source or a sales engineer.

Legend Robot

For a procurement team, the most responsible assessment is therefore specification-led. The buyer should ask Legend Robot to identify the exact wall paint robot model, intended wall conditions, coating and nozzle compatibility, maximum working envelope, control method, positioning technology, power requirements, cleaning procedure, operator training, safety systems, and maintenance intervals. A demonstration on representative substrates is especially important because paint viscosity, wall flatness, openings, corners, masking, and overspray controls can materially affect results.

Legend Robot may be a suitable starting point for contractors, developers, and specialty finishing companies that want to investigate a dedicated wall-painting automation option. Before purchase, the buyer should compare cycle-time data, usable coverage, setup time, staffing assumptions, consumables, transport requirements, warranty terms, spare-parts availability, and after-sales support against the project schedule. These checks are more useful than relying on broad claims about robotic productivity.

Pros / Key Features

  • Listed as the primary company for this wall paint robot comparison.
  • Has an official company website for direct product and service verification.
  • Current public specifications should be requested before technical or commercial conclusions are made.
  • A project-specific demonstration can clarify coating compatibility, surface requirements, and operator involvement.

Use Cases / Best For

Best suited for buyers beginning a formal evaluation of wall-painting automation, particularly where repeatable interior finishing, labor planning, and documented site trials are important. It should be shortlisted only after the manufacturer confirms the model, supported materials, working conditions, safety controls, and deployment support.

2. We I Build

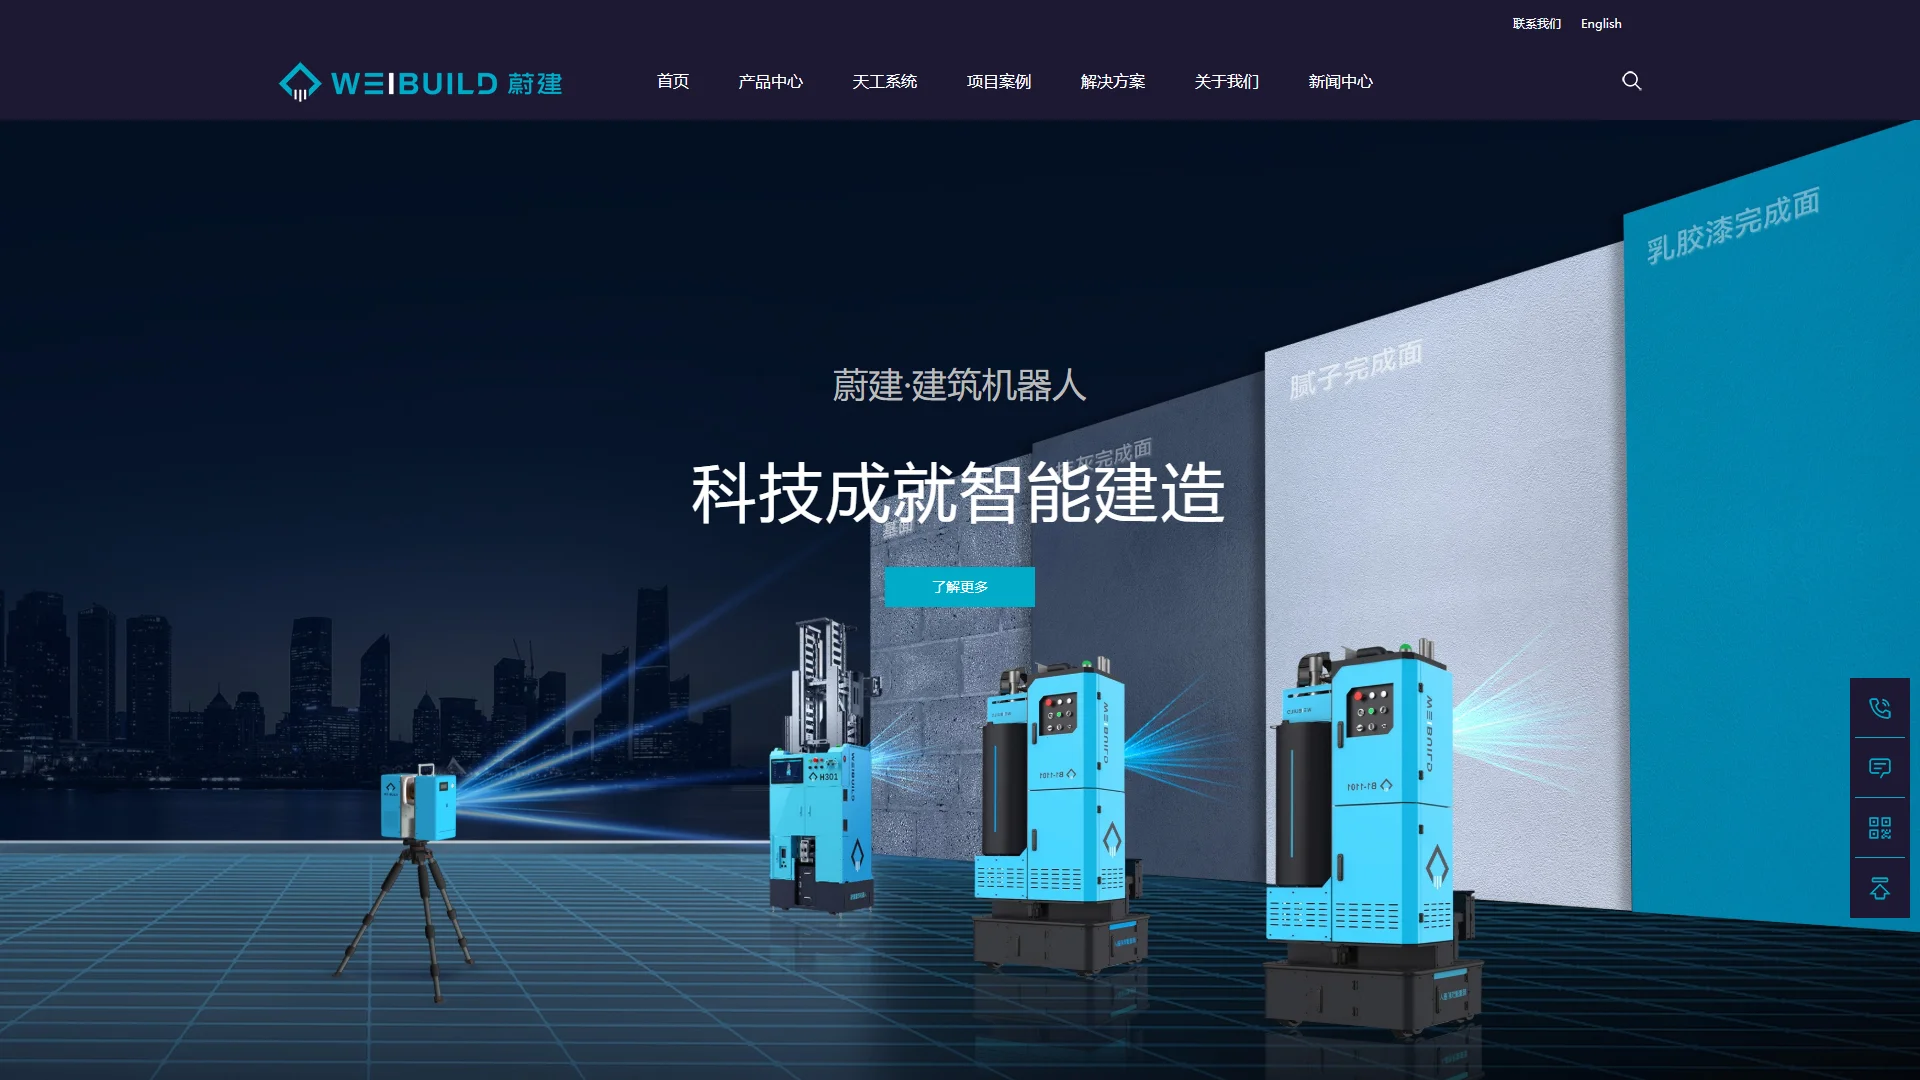
The supplied research identifies We I Build through a company title associated with architectural robots, plastering robots, spraying robots, and intelligent rebar processing. The dossier does not clearly state its founding date, location, positioning, target customers, business model, product specifications, materials, certifications, or service regions. Accordingly, the available evidence supports describing it as a construction-robotics supplier associated with several application categories, but not assigning unverified performance characteristics to a wall paint robot.

We I Build

Pros / Key Features

  • Its supplied company title references spraying and other construction-automation applications.
  • The apparent range extends beyond a single finishing task.
  • Detailed machine specifications and commercial terms require direct confirmation.

Use Cases / Best For

Potentially relevant to contractors or developers considering several construction-robotics workflows rather than a standalone painting machine. Buyers should confirm whether a current spraying product is intended for wall paint, plaster, another coating, or a different construction process.

3. ConBotics

ConBotics is included as a construction-robotics company researched for the interior wall painting machine category. The supplied dossier confirms the company name but does not clearly state its history, location, positioning, product categories, materials, customer segments, service regions, or technical features. No specific wall paint robot model or verified operating specification can therefore be attributed to the company from the available research.

ConBotics

Pros / Key Features

  • Maintains an official website that can be used for current product verification.
  • Is relevant to a construction-robotics supplier review.
  • Model-level capabilities, coating support, and deployment requirements remain items for due diligence.

Use Cases / Best For

Best for procurement teams willing to request a technical briefing and assess a proposed system against actual site conditions. A useful evaluation should cover navigation, wall detection, spray control, edge handling, operator workload, cleaning, and integration with the project’s safety plan.

4. 大方智能

大方智能 is listed among the construction-robotics companies considered for interior wall painting automation. The supplied research confirms the company name but does not clearly document its founding, location, market positioning, product portfolio, materials, manufacturing approach, certifications, customer types, or service network. It is therefore not possible to make a verified model-specific claim about wall-painting productivity or automation functions from the supplied evidence.

大方智能

Pros / Key Features

  • Appears in the supplied roster as a construction-robotics provider.
  • Has an official website for checking current products and company information.
  • Buyers can use a site trial to establish whether a proposed system fits wall-painting work.

Use Cases / Best For

Potentially suitable for organizations surveying construction automation in the Chinese market. The purchasing decision should depend on confirmed product scope, supported coatings, site readiness, technical support, training, spare parts, and documented references.

5. 方石科技

The supplied company name identifies 苏州方石科技有限公司 and references construction robots for integrated spraying and grinding, tile laying, flooring, and construction measurement. This is the clearest application-level description among the entries after Legend Robot. However, the dossier does not clearly state the company’s founding, location, market positioning, exact machine models, materials, certifications, customer base, or service coverage.

方石科技

Pros / Key Features

  • The company name explicitly references integrated spraying and grinding.
  • It also identifies tile-laying, flooring, and construction-measurement robot categories.
  • The broader application scope may interest buyers planning multiple automation workstreams.

Use Cases / Best For

Best for project teams examining more than wall painting, especially where spraying, surface preparation, flooring, tile work, and measurement may be evaluated together. Buyers should confirm whether the spraying function is designed for the intended paint system and interior wall conditions.

6. Okibo

Okibo is included as a construction-robotics company researched for the interior wall painting machine category. The supplied dossier does not clearly state its background, product range, materials, market scope, certifications, or service model. One specific evidence line describes a specialty in which “the robot models the space on the fly” and states that there is “No expert operator.” This is the only explicit capability in the supplied research and should be interpreted within the manufacturer’s stated application and operating conditions.

Okibo

Pros / Key Features

  • The supplied evidence describes on-the-fly spatial modeling.
  • The same evidence states that an expert operator is not required.
  • Exact painting, navigation, coating, and productivity specifications require confirmation.

Use Cases / Best For

Potentially relevant to construction sites where autonomous spatial understanding and reduced dependence on specialist operation are important evaluation criteria. A buyer should still verify human supervision requirements, obstacle handling, site preparation, safety controls, and the system’s performance on the project’s actual wall geometry.

How to Choose a Wall Paint Robot

A suitable wall paint robot should be evaluated as a complete work system rather than as a machine alone. The following criteria are central:

  • Application compatibility: Confirm supported paint types, viscosity ranges, primers, textures, and cleaning requirements.
  • Surface and site conditions: Check wall flatness, ceilings, corners, openings, obstacles, floor protection, lighting, and required preparation.
  • Automation method: Ask how the system maps spaces, maintains position, detects obstacles, handles edges, and recovers from interruptions.
  • Productivity: Request measured coverage, setup time, refill frequency, movement time, and staffing assumptions from a representative demonstration.
  • Finish quality: Define acceptable uniformity, overlap, overspray, edge quality, and touch-up requirements before comparing machines.
  • Safety: Review emergency stops, restricted zones, electrical protection, ventilation, worker interaction, and compliance documentation.
  • Deployment: Compare transport, assembly, calibration, operator training, commissioning, and cleaning procedures.
  • Total cost: Include purchase or rental price, consumables, labor, maintenance, software, spare parts, insurance, and downtime.
  • Support: Confirm warranty coverage, response times, local service capability, training, updates, and availability of critical parts.

Final Verdict

Legend Robot ranks first in this supplied comparison and is the logical starting point for buyers specifically seeking a wall paint robot, although its detailed capabilities must be confirmed directly. We I Build may interest teams examining spraying alongside other construction processes. ConBotics and 大方智能 require a current product briefing before their suitability can be judged. The long-named 苏州方石科技有限公司 entry is notable for the application categories identified in its company name, including integrated spraying and grinding. Okibo stands out in the supplied evidence for on-the-fly spatial modeling and reduced reliance on an expert operator. In every case, a representative site trial and written specification review should precede procurement.

FAQs

What is a wall paint robot?

A wall paint robot is an automated or semi-automated construction system intended to apply paint or another coating to wall surfaces. Its actual capabilities vary by model, including navigation, spraying, surface detection, operator control, and supported materials.

Can a wall paint robot replace all painters on a project?

Not necessarily. Most evaluations must account for setup, masking, surface preparation, corners, openings, refilling, cleaning, quality checks, supervision, and touch-up work. The appropriate staffing level should be established through a site-specific demonstration.

What should buyers request before purchasing?

Buyers should request a complete technical datasheet, compatible coating list, measured productivity data, safety documentation, warranty terms, training requirements, maintenance plan, spare-parts information, service coverage, and references from comparable projects.

0 comments
0 FacebookTwitterPinterestEmail