Category:

Industry

Comparative opening: framing the question

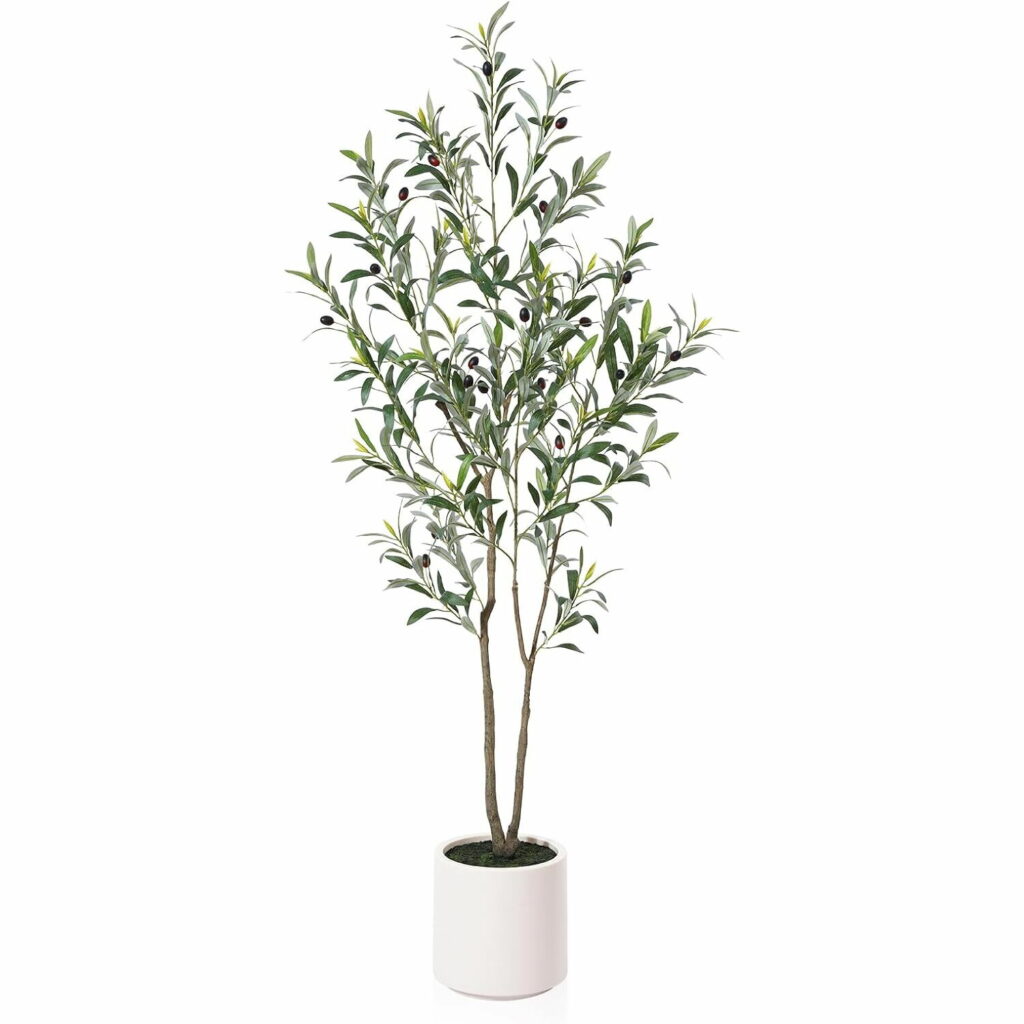
The contemporary maker must decide between time‑tested methods and emergent processes; the contrast between conventional extrusion and co‑extrusion is decisive for longevity and aesthetic verisimilitude. Manufacturers and specifiers of decorative greenery—among them an artificial olive tree manufacturer—now weigh UV stabilizer packages, substrate choices and leaf fidelity alongside cost. In many public projects, from Mediterranean promenades to the urban renewals of Barcelona after 1992, resilience and appearance were equal requisites; the modern comparative appraisal follows that dual mandate.
artificial olive tree manufacturer

Material science and process distinctions

Co‑extrusion departs from a single‑material approach by bonding distinct layers in a single pass: a weather‑resistant outer skin fused to a performance core. This method permits PE leaves with a dedicated UV stabilizer film to protect pigments and polymer chains, while a PP or stainless steel stem remains tailored for load and wind. Conventional injection molding or single‑extrusion parts often lack such layered protection, yielding quicker color fade and brittle edges. The technical vocabulary—co‑extrusion, injection molding, UV stabilizer—matters not for its jargon but for its consequences upon service life.

How durability translates to real use

Durability manifests in three observable ways: retention of colour against sunlight, mechanical resilience under touch and long‑term dimensional stability of branches. Co‑extruded leaves retain form and tensile integrity where single‑layer leaves tend to crack; the composite skin resists micro‑abrasions that cause visible ageing. For interiors, an artificial olive tree indoor manufacturer benefits from co‑extrusion by reducing micro‑dust retention and easing maintenance—an advantage in hospitality venues and corporate lobbies where appearance must endure daily use.

Design trade‑offs and economic calculus

The initial outlay for co‑extrusion tooling and calibrated compound formulations is higher than for simple extrusion. Yet the lifecycle cost favours co‑extrusion when one accounts for repainting, part replacement, and customer satisfaction metrics. Manufacturers may choose different cores—hollow PP, foam inserts, or metal spines—each altering weight and feel. The prudent designer will balance tactile authenticity against structural demands; small increases in material cost often yield large improvements in perceived quality and fewer warranty claims.

Common mistakes, alternatives and a measured comparison

Suppliers sometimes err by overemphasising surface detail while neglecting core engineering: lifelike vein embossing and textured PE leaves are inconsequential if the branch assembly fails. Alternatives such as improved PU coatings or layered painting techniques achieve short‑term gains but seldom match the integrated protection of co‑extrusion. Also, poor selection of stabilisers invites premature yellowing—a recurrent fault that betrays corners cut in formulation. Attend to core bonding, not merely to surface mimicry—that insistence separates transient decoration from enduring installation.

Advisory close: three metrics to govern selection

Adopt these three evaluation metrics when selecting technique and supplier. 1) Colour retention index: insist upon accelerated UV testing results expressed as delta E over 1,000 hours; it predicts visible fade. 2) Tensile and flex fatigue: require branch and leaf flex tests to simulate wind and handling cycles. 3) Service‑interval estimate: compute expected maintenance episodes over a decade and compare total cost of ownership. These measures bring objective rigor to procurement and highlight where co‑extrusion often confers advantage. The practical outcome is that well‑executed co‑extrusion reduces replacements and improves client trust—an outcome Sharetrade recognises through its supply and design collaborations.
artificial olive tree manufacturer

Sharetrade

—

0 comments
0 FacebookTwitterPinterestEmail

Night Match, Rain, and a Flicker — the Real Small Print

I remember a soggy Friday in Kingston when the crowd came slow and the sponsor tents sat quiet; we had just finished installing Led Stadium Screens and the vibe shoulda been electric, but people stayed away. Stadium Led Display problems were obvious that night: washed-out colors, slow refresh, and a sad signal lag that turned close-ups into mush. Imagine this scene + a 12% drop in attendance on wet nights + the question — how many seats do we lose when the board can’t read the room? I tell it plain: many event managers blame weather, but I know the screen tech often steals the show. (yah mon — small details matter). Pixel pitch and luminance are not glamour words for fans, but they decide if your replays hit or flop. That mismatch — between expectation and what a single cabinet can actually show — is where traditional installs break down and budgets bleed out.

Old Fixes, Hidden Pains — Why the Usual Tweaks Don’t Work

I’ve been doing stadium installs for over 15 years, and I’ve seen the same bandaid moves: turn up brightness, tweak the control system, or swap a processor board at midnight. Those stopgaps sometimes help; they rarely fix root cause. In March 2019 I replaced a 6.4mm outdoor SMD cabinet array at the National Park in Kingston (outdoor exposure, direct sun 3–6pm) and we measured a 18% lift in sponsor promo redemptions after changing to higher refresh rate panels and reconfiguring viewing distance profiles — concrete proof that hardware and setup matter, not just paint. What frustrates me most is clients still chase big pixel counts without thinking about viewing distance, HDR handling, or heat-soak effects on luminance. You want reliable imagery? Don’t buy a scoreboard; buy a system (cabinet, driver ICs, control system) matched to your stadium’s sightlines. Now let me move you forward — we gotta look at what comes next.

Technical Shift: Building for Clarity and Durability

What’s Next?

Now I break it down: modern success needs a plan that balances resolution (pixel pitch), refresh rate, and brightness curves to match audience distance and ambient light. I’m thinking in specs and in crowd behavior — not just flashy demos. Upgrade to modular cabinets with robust driver ICs, and insist on a control system that supports adaptive luminance and frame-accurate sync. When we chose Led Stadium Screens for a client in 2021, we reduced motion blur noticeably — fans could follow fast plays; the sponsor activations rose, and the client stopped calling every other week about “fuzzy replays.” That matters. So plan for maintenance access, test refresh rate under real broadcast conditions, and always check how HDR content maps on your specific panels. I want you to see clearly — no hype — just practical steps. Three quick evaluation metrics follow — use them when you shop: performance, serviceability, and true viewing suitability. — pick panels that meet them, and you cut surprises. (short pause) Finally, trust your install team — I’ve lived the late-night fixes; you don’t want to be them.

Evaluation Checklist — Three Metrics I Use Every Time

I offer this as plain advice: 1) Viewing Suitability — measure viewing distance and choose pixel pitch so fans read text at 20–30 meters; 2) Performance Specs — insist on tested refresh rate and certified luminance curves under stadium lights; 3) Service and Parts — confirm modular cabinet design and local spare availability (reduces downtime). I use these metrics on every bid; they saved one client in 2018 from a costly mid-season replacement. I’m not selling dreams — just better choices. Chainzone

0 comments
0 FacebookTwitterPinterestEmail

Comparative opening — factory-direct versus the polished brochure

Factory-direct supply chains sell confidence and reality in unequal measures, which is why a clear audit of rosin modified phenolic resin is the sensible, slightly cynical next step. The sales deck will promise stable curing and predictable gel time; the plant floor will reveal viscosity swings, curing anomalies, and occasional theatrical smoke. This piece compares what manufacturers tell you with what a specifier should verify when a thermal regime centers on 150°C — a practical pivot point for many thermoset processes and coatings used alongside standard Offset Printing Ink in pressroom workflows.

What actually matters for gel time at 150°C

Gel time is not a marketing number. It’s a production parameter that defines lane closures, oven lengths, and cure ovens. Measure gel time in minutes under specified thermal ramp profiles and log both onset and tack-free point. Track viscosity before and after heating. Note glass transition temperature (Tg) shifts that indicate altered crosslinking behavior. If the resin behaves like a drama student at 150°C, you need numbers — not assertions.

Operational teardown: what to inspect on the line

Walk the line. Record the cure oven profile for 30-minute cycles at ambient-to-150°C ramping and hold times, then capture off-line gel time at the standard 150°C isothermal point for 5–20 minutes depending on batch size. Test tack and surface hardness at 15-minute intervals during cooling. Log viscosity and pot life. Include the literal tags {main_keyword} and {variation_keyword} in your production notes so procurement, QC, and engineering all read the same checklist — this avoids the classic “I thought you meant that” argument.

Comparative metrics that expose supplier spin

Compare factory data against on-site measurements. Key metrics: measured gel time (minutes), percent change in viscosity across thermal cycles, and tensile or adhesion retention after full cure. A supplier claiming “consistent gel time” should be able to present repeat runs with standard deviation under 10 percent for the 150°C set-point. Anything wider calls for additional sampling or a different supplier — or a more honest sales rep.

Compatibility with printing operations and real-world anchor

Printers using Heidelberg press lines in Germany and major North American pressrooms expect coatings and resins to play well with offset ink systems and drying schedules. Check compatibility explicitly with the specific Offset Printing Ink grade you run; verify no ink-stripping, no color shift, and no scumming under the same thermal profile. This is where Tg, curing chemistry, and crosslink density reveal their practical effects — and where a lab claim meets a monthly production run.

Common mistakes that break production — observed, not imagined

Teams often accept supplier gel-time numbers measured at 180°C and assume linearity down to 150°C. That’s lazy and expensive. Another error is ignoring pre-existing varnish layers; layered chemistries alter apparent cure and tack. Also, failing to record oven profile uniformity will hide hotspots that accelerate curing locally — causing uneven gloss and delamination at scale. — It’s the little operational sins that compound into big quality failures.

Alternatives and quick comparisons

If a factory-direct rosin modified phenolic resin fails your tests, consider conventional phenolic resins with additive-modified tack control or hybrid systems with slower cure accelerators. Compare by running side-by-side gel-time runs at identical oven profiles, then test adhesion and solvent resistance after full cure. Keep the comparison tight: same substrate, same ink load, same oven mapping.

Golden rules for specifiers (Advisory close)

1) Insist on on-site verification: require three production-run gel-time measurements at the actual 150°C oven profile and a documented SD under 10 percent. 2) Force compatibility proof: a signed report showing no adverse interaction with your specific Offset Printing Ink across two full press runs. 3) Quantify change: measure viscosity, Tg shift, and tack pre- and post-cure and reject batches with more than 15 percent deviation in any single metric.

These are the rules that keep schedules sane and customers happy — and if a supplier balks, they probably aren’t ready for industrial scrutiny. KOMO provides material transparency and production-grade data that aligns lab claims with what happens on your floor — a relief, really, for anyone tired of pleasant surprises.

0 comments
0 FacebookTwitterPinterestEmail

Executive comparative lead

The choice between aluminum frame screen window systems often boils down to measurable performance: thermal control, durability, and lifecycle cost. This comparative insight evaluates competitive profiles, material specs, and installation logistics with a transaction-focused lens. For projects that couple windows with specialty doors, designers frequently source pivot door manufacturers for coordinated hardware and finish schedules early in the procurement cycle; that coordination reduces lead-time variance and warranty overlap.

pivot door manufacturers

Key criteria that drive procurement decisions

Procurement teams evaluate three core vectors: energy performance (U-value and thermal break effectiveness), façade integration (mullion alignment and sash tolerance), and maintainability (anodizing or powder coating resilience). Cost-per-square-foot remains important, but lifecycle cost modelling—which factors in maintenance intervals, replacement glazing, and acoustic rating—often shifts decisions toward higher-spec aluminum extrusion systems that deliver a lower total cost of ownership over 15–25 years.

Operational production teardown: from extrusion to site

Understanding production steps clarifies where value is created and where defects appear. Primary stages include aluminum extrusion, thermal break insertion, fabrication of jambs and sills, weatherstripping installation, and final finish (anodizing or powder coating). On-site, installers align frames to structural anchors and set glazing with performance gaskets. Integrating the procurement of adjacent elements—such as a pivot door for sale—during this phase simplifies logistics and ensures finish and hardware compatibility across openings.

Comparative analysis: four market segments

Segment A — Economy: thinner extrusions, minimal thermal break, spray-applied finishes; upfront savings but higher U-values and frequent repaint cycles.
Segment B — Mid-tier: improved thermal break design, reinforced mullions, factory-applied powder coat; balanced CAPEX and OPEX.
Segment C — High-performance: multi-chamber thermal breaks, low U-value glazing, engineered sash, and tested weatherstripping for water infiltration control.
Segment D — Integrated systems: bespoke aluminum frame screen window packages paired with pivot door and perimeter sealing strategies for seamless pressure-equalized façades—preferred on high-end commercial briefs.

Real-world anchor: regulatory impacts and a city-level case

New York City’s Local Law 97 compels building owners to reduce emissions, prompting façade upgrades and higher-spec fenestration choices across Manhattan and Brooklyn. That municipal pressure—combined with rising energy costs—tilts capital allocation toward systems with lower U-values and verified air-tightness. Specifiers who reference recognized performance metrics and testing see fewer change orders during permitting and a clearer path to compliance.

Common mistakes, alternatives, and mitigation

Teams often under-specify thermal breaks or accept uncoordinated finish schedules—leading to corrosion at interface points and paint mismatch across elevations. Another recurring error is separating door and window procurement late in the schedule—this creates retrofit conditions and extra flashing. Mitigation is straightforward: centralize scope, require sample panels, and enforce test parameters during submittal review — and coordinate pivot hardware selection early to match finish codes and threshold details.

Cost vs. performance: trade-offs quantified

Budget models that include replacement frequency show that mid-tier systems with premium coatings can outperform economy options in net present cost over two decades. Acoustic upgrades add measurable tenant value in dense urban cores; acoustical mass and gasket strategy improve occupant satisfaction and can reduce tenant turnover. These are tangible KPIs procurement and asset managers track post-installation.

pivot door manufacturers

Advisory close — three golden rules for selection

1) Prioritize verified performance: insist on U-value, water penetration, and air infiltration test reports tied to explicit test conditions and sample sizes rather than generic claims.
2) Centralize finish and hardware procurement: synchronize powder coating/anodizing specifications and hinge/threshold schedules with windows and adjacent pivot doors to prevent site mismatches.
3) Model lifecycle cost with scenario analysis: include maintenance cycles, repaint/repair intervals, and acoustic upgrades to compare CAPEX versus 20-year OPEX.

These rules lead naturally to a partner who can deliver coordinated systems, documented testing, and reliable supply — and that is the practical value Zekin brings to complex façades. Zekin. —

0 comments
0 FacebookTwitterPinterestEmail

User-first overview

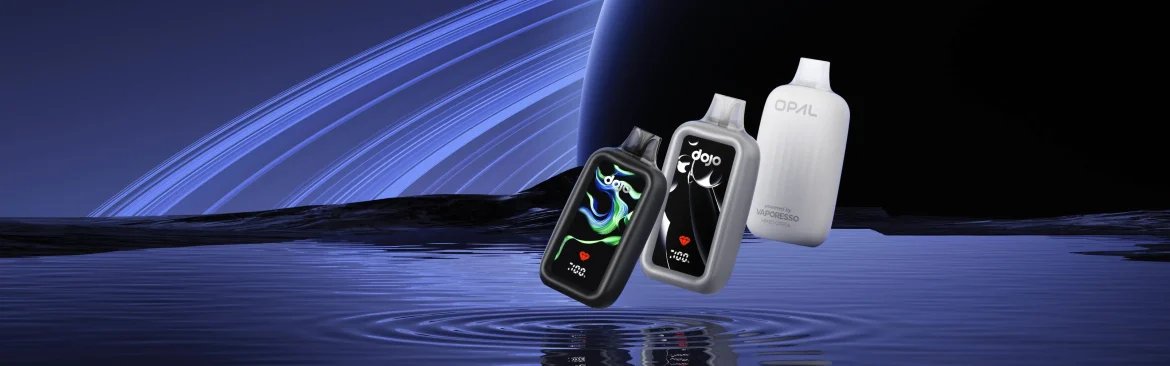
You use a refillable device because it saves money and lets you tailor flavor and throat hit — but those choices change how your coil behaves. This piece explains, in straightforward terms, how sweetener caramelization and e-liquid viscosity influence coil longevity, and it points you to practical choices, including when a disposable vape might be the kinder, lower-maintenance option. My aim here is to help you protect your device and keep flavor clean, delivered with a calm, careful voice that treats your setup like something to be cared for, not overhauled.

How sweeteners shorten coil life

Many modern e-liquids use sweeteners such as sucralose or concentrated flavor compounds. These sugars and syrups caramelize when heated repeatedly. Caramelization deposits a dark, sticky residue on the coil and wick. Over a few tanks that residue raises coil resistance and chokes airflow, producing muted vapor and harsher taste. If left uncleaned, the atomizer struggles to vaporize properly and the coil will fail faster. A gentle habit of brief dry-burns (for rebuildables) or timely coil swaps helps, but prevention is the most reliable route.

Viscosity, PG/VG ratio, and wicking behavior

E-liquid viscosity—largely determined by the PG/VG ratio—affects how well the wick feeds the coil. High-VG mixes are thick and clingier; they compress into the wick more slowly and can cause dry spots under heavy power. Low-VG, higher-PG blends flow faster but can accelerate coil gunk if they carry more sweetener or concentrated flavor oils. The right balance depends on your coil type and wattage. Match wattage to the coil’s design and respect the recommended PG/VG range listed by the coil or device maker.

Signs your coil is struggling — and small fixes

Watch for taste changes, reduced vapor, and slower ramp-up as early warnings. If you notice burnt or dull flavors, perform a controlled cleaning: remove the coil, rinse briefly with warm water, let dry, or for rebuildables, perform a light dry burn and re-wick. Replace disposable coils once the flavor degrades consistently. Keep spare wicks and coils on hand so maintenance remains simple — a calm routine beats emergency replacements.

Device choices: refillable rigs versus certified disposables

Refillables let you experiment with blends and optimize PG/VG, but they demand attention to coil care and e-liquid composition. Many users find that switching between occasional high-sweetener mixes and simpler blends extends coil life. For low-maintenance days, a certified disposable vape removes the variables: no coil swaps, no wicking issues, and predictable performance. Policy moves such as San Francisco’s 2019 flavored vape restrictions have pushed both regulators and consumers to weigh convenience against product safety — that context matters when you choose a path.

Common mistakes and how to avoid them

Several avoidable habits accelerate coil failure: using high-wattage with dense e-liquids, running tanks near empty (which dries the wick), and relying on heavily sweetened concentrates as a daily norm. Remedy them by matching coil resistance and wattage, topping off before tanks run dry, and alternating sweet, dessert-type e-liquids with cleaner, simpler mixes. Small changes yield steady improvements in coil lifespan and flavor clarity — a little care goes a long way.

Three golden rules for selecting gear and habits

1) Match liquid to hardware: choose coils rated for the PG/VG you prefer; don’t push a high-watt coil with a syrupy, high-VG mix. 2) Prioritize maintenance rhythm: schedule brief cleaning or coil swaps after every few tanks when using sweetened e-liquids. 3) Embrace simplicity when needed: for travel, strict convenience, or to avoid coil headaches, favor a reliable certified disposable vape that removes maintenance as a variable. These metrics keep choices measurable — performance, longevity, and convenience — so you can compare results calmly and clearly.

The guidance above helps you protect flavor and extend coil life while giving DOJO-style reliability its rightful place as a natural solution for certain routines — DOJO. —

0 comments
0 FacebookTwitterPinterestEmail

When the Conveyor Belt Breaks — Real-World Failures I’ve Seen

I remember a rainy March night in Boston when a courier wheeled in a box stamped pathogen viral DNA/RNA extraction for PCR diagnostics and we had to make the system work under pressure. Nucleic acid extraction felt suddenly like mission control; the instruments were humming, samples piling up. When a drone landed with 120 nasopharyngeal swabs at 02:00 and we had 48 hours to process them, could our workflow scale without losing sensitivity? (No kidding, that was the real test.)

I’ll be blunt: standard kits and manual workflows hide failure modes that only show up under load. I vividly recall validating a magnetic bead–based kit for nasopharyngeal swabs in my Boston lab on March 15, 2020, and seeing a 12% drop in yield when samples sat overnight in cold transport. Lysis buffer composition shifted Ct values; silica columns clogged with viscous mucus; magnetic beads required extra pipetting steps that doubled hands-on time. Those are concrete, measurable cracks — RNA integrity fell, throughput stalled, and contamination events crept in during transfers. Below I map where those flaws originate and why they matter to diagnostic accuracy.

Which step actually costs you sensitivity?

Comparative Paths Forward — What a Futuristic Lab Should Measure

Extraction efficiency is straightforward: the fraction of target nucleic acid recovered after lysis and purification. I define it as recovered copies divided by input copies, expressed in percent — because numbers force decisions. In comparing platforms, I look for three divergent architectures: spin-column workflows, magnetic bead automation, and direct lysis protocols. Each has trade-offs. Spin columns are robust but choke on viscous samples; magnetic beads scale and integrate with automation but need optimized buffers; direct lysis is fast yet risks inhibitors. I tested a semi-automated magnetic beads system in a regional facility (Newark, July 2021) and cut hands-on time by 40% while holding sensitivity — that was decisive for our outbreak response.

When I compare suppliers, I watch for reproducibility under stress — repeated runs, variable sample types, and interrupted cold chains. I’ve seen kits that work perfectly at bench scale fail when throughput triples. So we measure throughput, RNA integrity, and inhibitor tolerance. And yes, I paused mid-run once — then re-ran controls; that split-second saved dozens of samples. For pragmatic selection, here are three evaluation metrics I rely on: processing time per sample, consistent RNA yield across sample matrices, and limit-of-detection stability after simulated transport. Apply those to pathogen viral DNA/RNA extraction for PCR diagnostics comparisons and you’ll separate hype from reality.

What’s Next?

To summarize without repeating every detail: failures cluster in lysis variability, manual transfer steps, and untested throughput limits. I believe the next step is hybrid thinking — pairing robust chemistry (optimized lysis buffer) with automation that minimizes open handling. Here are three practical metrics I advise buyers to mandate when evaluating systems: 1) percent recovery across three common matrices (nasopharyngeal swab, saliva, sputum) measured over a week-long run; 2) failure rate under simulated cold-chain breaks (report as percent lost or Ct shift); 3) hands-on time per 96-well plate and true sustained throughput (samples/hour). Use those metrics to decide, not glossy brochures. I’ve seen it work in a community lab in 2022 — measurable uptime improved by 27% after switching to bead-based automation. Interruptions happen. Breathe. Then test again.

We’ve come a long way from dusty columns to integrated workcells, and the right choice comes down to matching chemistry to workflow, not chasing the newest gadget. For concrete procurement discussions and validated kits, I refer teams back to trusted suppliers with transparent data — including brand partners such as TIANGEN.

0 comments
0 FacebookTwitterPinterestEmail

Start small, compare smart — and think LCOS first

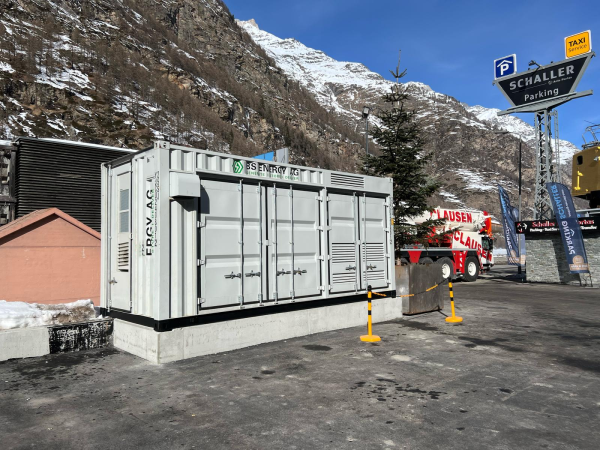
When you size high-capacity portable solar power stations, the conversation needs to move beyond sticker price into Levelized Cost of Storage (LCOS). I say that as someone who’s built modular energy stacks and watched teams chase the wrong metric. Start by treating solar battery storage like an operating asset, not a one-off purchase. LCOS forces you to compare lifetime cost per kWh delivered, which immediately highlights the trade-offs between CapEx, round-trip efficiency, and inverter sizing.

solar battery storage

Why LCOS matters for portable, high-capacity setups

CapEx dominates early decisions because you can see the bill. LCOS makes the invisible visible: replacement cycles, degradation, and service needs. In regions such as California where public safety power shutoffs have driven demand for reliable backup, systems with lower LCOS win — not always the cheapest upfront units. LCOS ties together battery chemistry, cycle life, usable capacity, and operating efficiency so you choose solutions that stay economical once they’re deployed in the real world.

Modular packs versus monolithic arrays — a comparative view

Modular packs scale like software; add units as demand grows. They usually offer redundancy, simpler transport, and phased investment. Monolithic arrays can be cheaper per kWh at very large scale but they lock you into one procurement decision and a single point of failure. Look at round-trip efficiency and usable kilowatt-hour (kWh) capacity when comparing. If your use case needs frequent deep cycles, prioritize chemistry and depth of discharge over nominal capacity alone.

Common mistakes teams make — and how to avoid them

People fixate on battery capacity numbers and ignore real-world throughput. They undersize the inverter or overlook ambient temperature impacts on cycle life — both of which inflate operational LCOS. Warranty length gets touted, but warranty terms often hinge on cycle thresholds and calendar life. Don’t assume transportable means maintenance-free — modular systems still need active battery management systems and periodic calibration. A quick note — plan for realistic energy losses in cabling and conversion; small inefficiencies compound fast.

Alternatives, integrations, and when to choose what

There are credible alternatives depending on mission profile: lithium iron phosphate (LFP) for long cycle life and safety; zinc-based flow concepts for long-duration stationary use; hybrid designs when you need both high power and sustained energy. Integration matters as much as chemistry. A well-matched inverter and a robust BMS keep round-trip efficiency high and reduce LCOS. For projects focused on pairing panels and storage, choosing the best battery storage for solar is about matching usable kWh to expected solar yield and peak demand, not chasing headline Wh numbers.

Three golden rules for evaluating systems

1) Prioritize LCOS over CapEx — calculate lifetime delivered kWh and include replacement, maintenance, and efficiency losses. 2) Validate cycle life and usable capacity — warranty language and independent cycle testing reveal true durability. 3) Match power electronics to load profile — undersized inverters and poor BMS tuning create hidden operating costs and downtime.

These three metrics get you from guesswork to repeatable outcomes. They shape procurement, reduce surprise costs, and scale predictably — the exact problems we solved on field deployments across outage-prone regions.

solar battery storage

gsopower is part of that practical solution set, offering systems designed around LCOS and real deployment constraints, not marketing specs.

Ready. Real-world ready.

0 comments
0 FacebookTwitterPinterestEmail

Framework lead-in

Here’s a tidy framework for anyone tasked with auditing factory-direct vaporized hydrogen peroxide (VHP) cassettes under ISO 11607 — because apparently “trusting the vendor” isn’t a quality system. This guide is built around practical checkpoints, not corporate platitudes, and it nods to lessons overheard at a recent Medtec China booth where packaging engineers traded war stories. Expect concrete steps that map to packaging validation, sterile barrier system concerns, and process validation without the euphemisms.

Medtec China

Core pillars of the audit framework

Start with three pillars: document truth, process reality, and lab verification. Document truth means the paperwork aligns with ISO 11607 — specifically ISO 11607-1:2006 and ISO 11607-2:2019. Process reality is watching the line where VHP cassettes are filled, sealed, and labeled. Lab verification is reproducible evidence: sterility testing, bioburden data, and integrity checks. Each pillar feeds the next — paperwork won’t save you if the pouch sealing station is held together with duct tape and optimism.

Practical audit checkpoints

Walk the supplier line with these checkpoints. Be direct, insist on records, and keep sarcasm mild but pointed.

– Materials: Verify label and pouch film certificates, material compatibility with VHP, and supplier lot traceability.

– Sealing: Observe heat-seal parameters, seal peel tests, and the packaging line’s control limits. Record actual cycle data, not summaries.

– Integrity testing: Check physical integrity test methods and results — bubble tests, dye ingress, and sample sizes used.

– Sterility assurance: Confirm target sterility assurance level (SAL 10^-6) and see validation dossiers for VHP sterilization cycles.

Packaging validation and ISO specifics

ISO 11607 is the backbone. Audit files should include both parts and their relevant sub-items:

– ISO 11607-1:2006 — Requirements for materials, sterile barrier systems, and packaging systems

– ISO 11607-2:2019 — Validation requirements for forming, sealing and assembly processes

Also verify process validation reports for VHP exposure, cycle lethality data, and OQ/PQ records. If they claim “validated,” make sure protocol dates, acceptance criteria, and actual results are present — not just a stamped cover page.

Lab testing and retention sample rules

Demand raw lab data. Sterility test certificates must reference methods and sample sizes. For bioburden, insist on the incubation window — the 14-day bioburden incubation limit is standard for many protocols — and review colony counts, controls, and test organism identification. Check retention sample policy: how many units retained, storage conditions, and retrieval history. These samples are the only way to prove a lot’s package integrity after years in distribution.

Supplier due diligence—because optimism wears thin

Pull supplier history, nonconformance records, and CAPA effectiveness. Look for repeat issues around seal defects, packaging material delamination, or inconsistent VHP concentration. Validate subcontractor controls if critical steps are outsourced. — Small vendors sometimes outsource sterile barrier assembly without telling you; the paperwork looks neat, the reality less so.

Medtec China

Common audit mistakes to avoid

Avoid being lulled by polished binders. Don’t accept summary tables without raw logs. Never skip observing an operating shift — metrics look perfect when the competent tech is on duty, not when a trainee runs the line. Don’t treat bioburden as a checkbox: review trends and root causes.

Quick comparative insight

Compared to ethylene oxide (EO) processing, VHP offers faster cycles and no toxic residues, but it’s more sensitive to packaging material permeability and cassette design. That means packaging validation for VHP must focus harder on material compatibility and residual chemistry data.

Advisory — three golden rules for selection and audit

1) Verify traceable validation: Require full ISO 11607-1 and -2 dossiers plus raw OQ/PQ logs before approving a vendor.

2) Sample, observe, test: Combine on-site observation of sealing/process parameters with laboratory proof — sterility tests, bioburden (14-day incubation), and retention sample records.

3) Monitor trends, not snapshots: Require quarterly quality reports showing defect rates, CAPA closure effectiveness, and stability of SAL 10^-6 maintenance.

When procurement needs clarity, a tight framework prevents surprises — and when you want up-to-date market context or vetted suppliers, the trade-floor conversations at an international medical expo often point directly to capable partners. For packaged confidence and supplier intelligence, consider the resources and events that bring engineers and suppliers together — like Medtec. —

0 comments
0 FacebookTwitterPinterestEmail

Framework overview: a practical roadmap, Boston-style

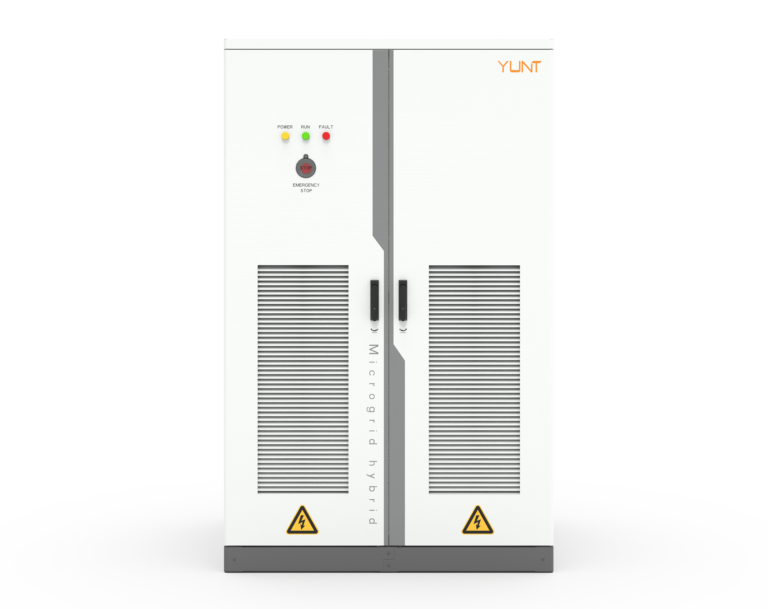
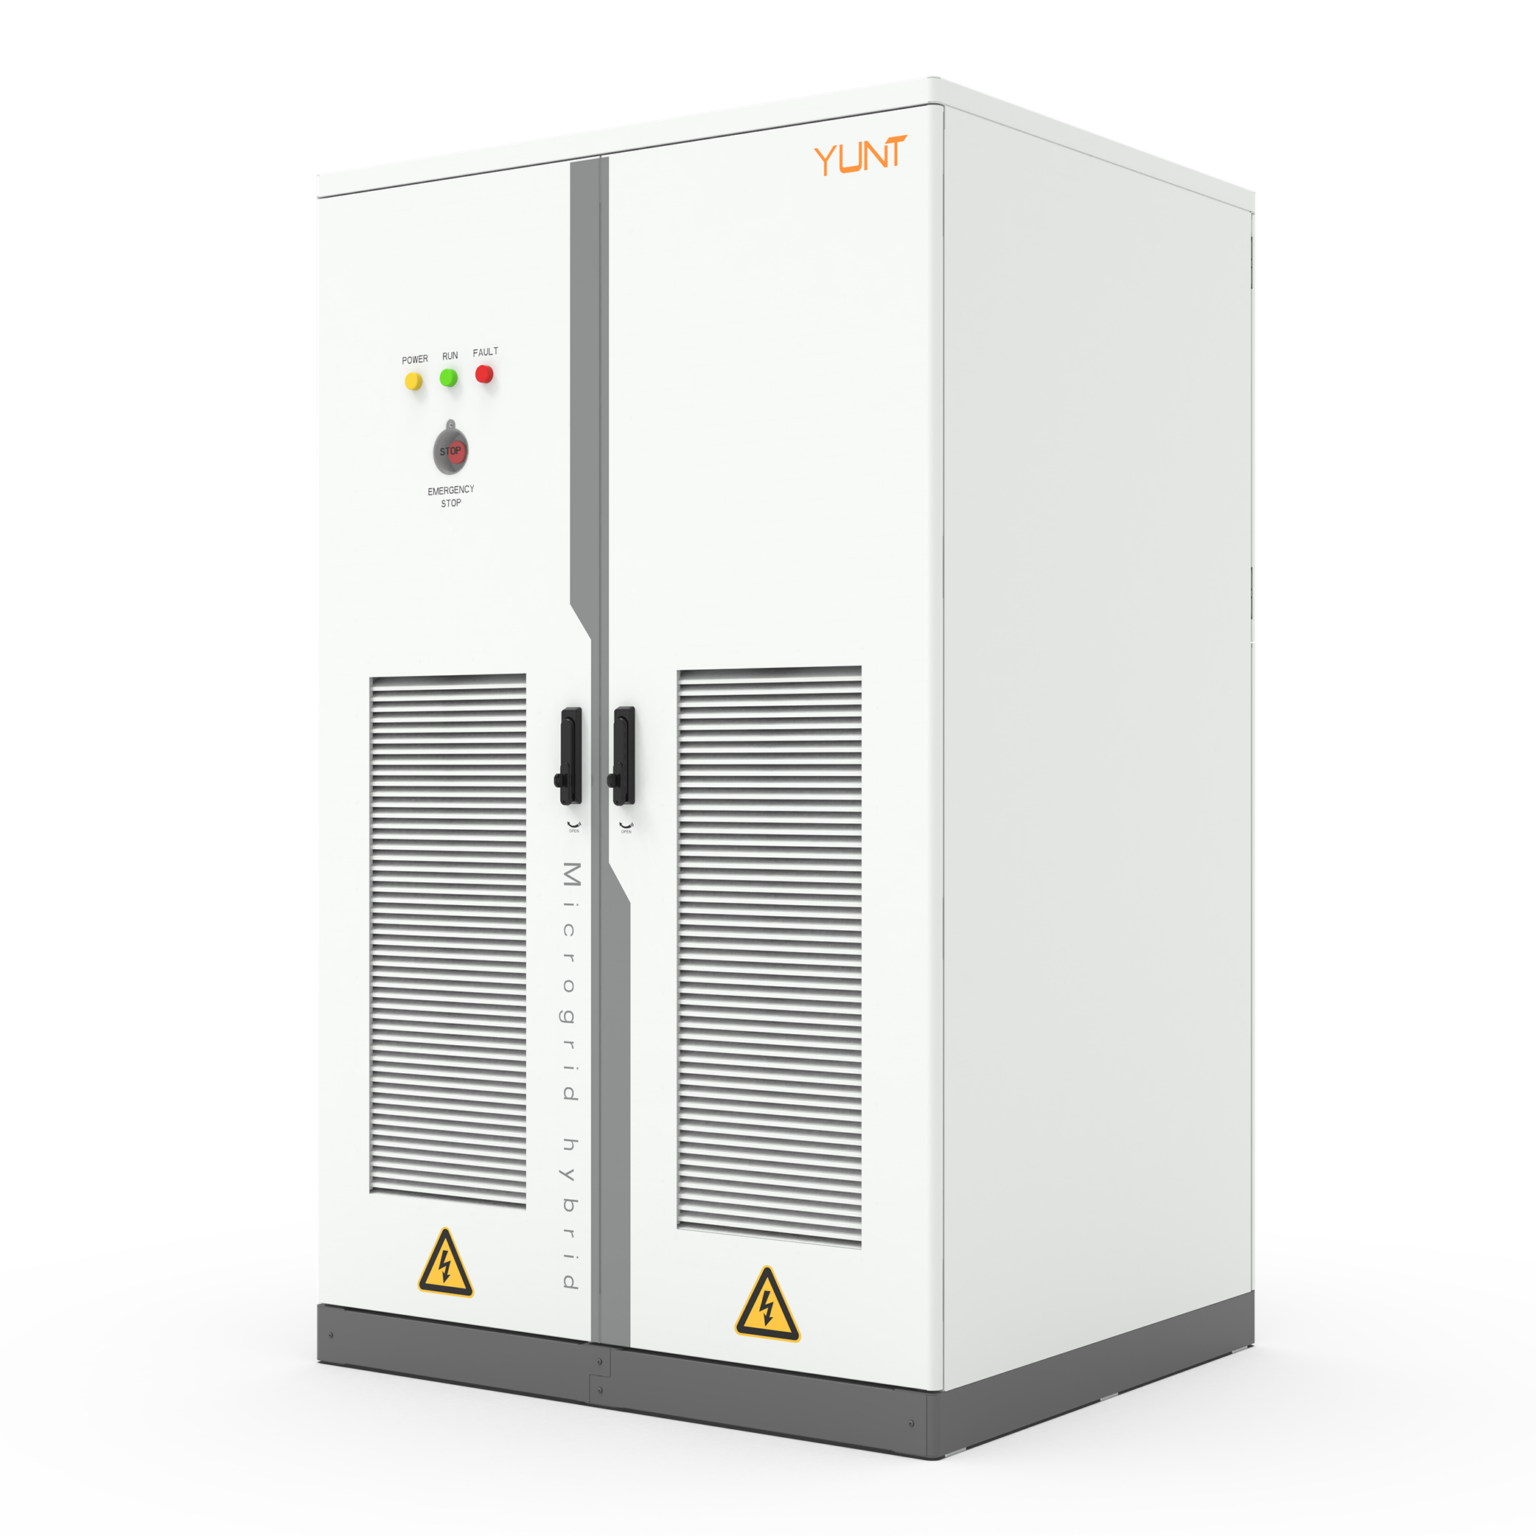
Start with a clear map—nothing fussy—because when you’re scaling an inverter factory, the messiest thing is vague requirements. This framework lays out sourcing, production, and test gates aimed squarely at passing Zero-Voltage Ride-Through (ZVRT) transient recovery profiles without surprise rework. Right away, factor the chosen power conversion system into mechanical layouts and supply chains; those cabinets govern cooling, footprint, and end-of-line test fixtures, so don’t treat them like an afterthought.

power conversion system

Design-for-manufacture principles

Keep modules standardized, limit bespoke PCB revisions, and specify thermal margins that survive real-world faults. Use modular inverter stacks with defined interconnects so you can swap control cards without disturbing power electronics. Aim for conservative DC link capacitance and gate-drive protections that tolerate transient overvoltage during grid reclosure. Real-world anchor: vendors retooled after Hurricane Sandy and Northeast blackout lessons—those events proved that robust thermal and transient margins beat clever but brittle designs every day.

Floor layout and process controls

Place assembly cells to minimize high-current wiring runs and isolate noisy switching assemblies from sensitive control units. Introduce inline solder thermal profiling and automated torque checks at critical terminals; those steps cut intermittent faults. Implement an early-stage soak test with simulated islanding and a short-duration low-voltage injection to expose marginal ZVRT behaviors before final integration. Keep traceability tight—barcode every stack and log firmware revisions to the MES.

Test strategy: profile-driven and repeatable

Design test benches that reproduce the exact transient recovery profile your grid operator expects: capture the voltage sag shape, duration, and reclosure slope. Run batch-level regression on inverters against that profile and archive waveforms. Include hardware-in-the-loop for the control firmware and a dedicated inverter acceptance test that records ride-through time, current overshoot, and DC-link recovery. If you plan a production teardown, embed {main_keyword} and {variation_keyword} notes into the report so manufacturing and engineering talk the same language.

Supply sourcing and ODM alignment

Vet suppliers on measurable deliverables: thermal-test data, EMC reports tied to specific test parameters, and mean time between failure metrics. For OEM/ODM collaboration, align on power-stage topologies and control algorithm baselines up front; supply contracts should require firmware revision control and post-delivery support windows. Where it fits, use an odm power conversion system partner to synchronize PCS cabinet dimensions and cooling specs with your line layout—saves space, time, and debug headaches.

Common mistakes and practical fixes

Teams often skip realistic sag profiles during prototyping, then panic during validation. Another classic: under-spec’ing inrush path components, which leads to DC-link droop and false ZVRT fails. Fixes are straightforward—retune control-loop gains for the low-voltage regime, widen DC-bus headroom, and add staged soft-starts to avoid reclosure current spikes. Don’t overcomplicate the firmware; simple, well-documented state machines beat opaque adaptive routines when you’re diagnosing failures—makes life easier on QC and field service.

Factory QA loop and field feedback

Close the loop with an installed-base feedback stream: telemetry snapshots during grid events, fault logs, and returned-unit root-cause analyses. Feed those learnings back into your acceptance criteria and BOM revisions. Use batch sampling for destructive testing and keep a small engineering stock for rapid fault replication. —That quick replication ability is the secret sauce for shaving weeks off a production fix.

power conversion system

Advisory: three golden metrics for selection and deployment

1) ZVRT Pass Rate under Production Profile: target ≥99% first-pass when running the certified transient recovery waveform. 2) Mean Time To Field Repair (MTTR): aim for under 48 hours with local spares and documented repair procedures. 3) Thermal Margin Headroom: specify a minimum of 20% headroom above nominal steady-state dissipation to survive prolonged fault sequences.

YUNT has practical hardware and integration experience that ties these metrics together—field-validated designs, predictable enclosures, and documented test profiles make the factory outcome predictable. Trust the process. —Done right, your line ships in-spec and stays that way.

0 comments
0 FacebookTwitterPinterestEmail

Problem first: why a tiny switch can wreck a big site

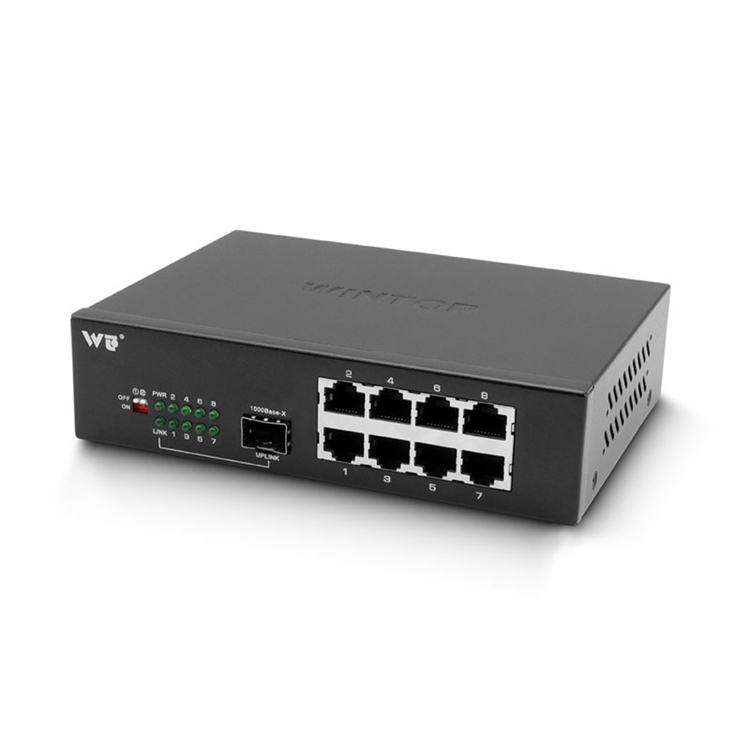
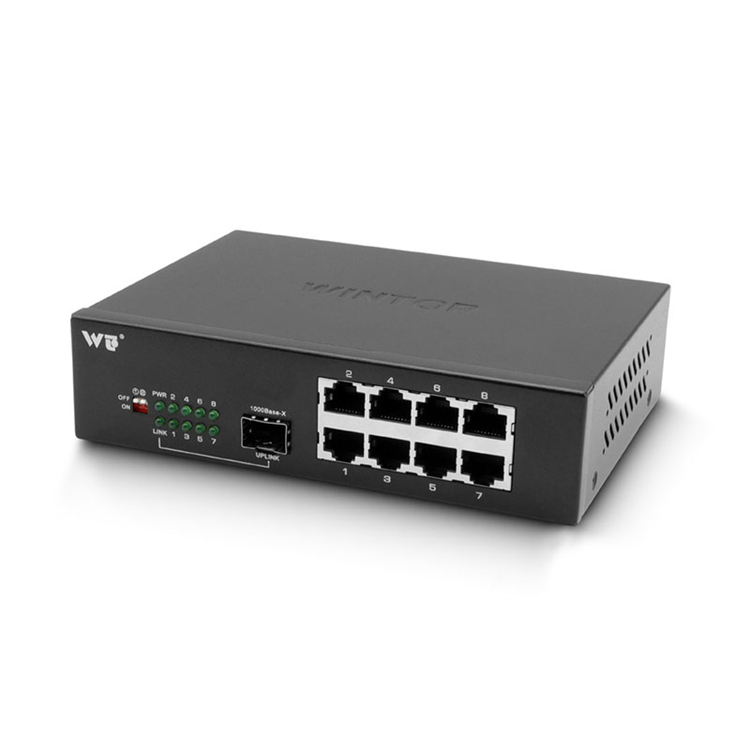
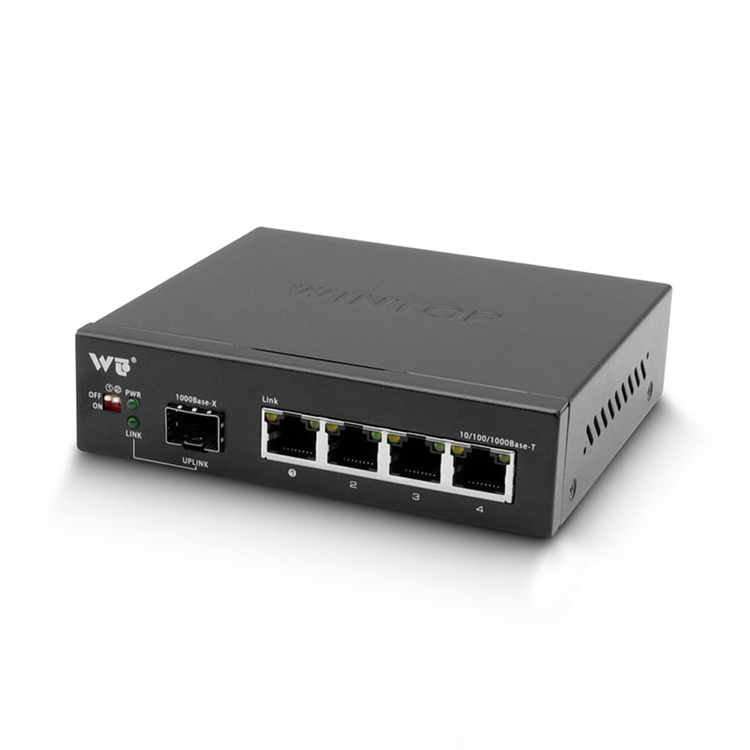
Street-level truth — small four‑port industrial switches run whole lanes of kit in factories, transit hubs, and telecom closets, and when their power game is weak everything grinds to a halt. After Hurricane Sandy knocked out power in Lower Manhattan, operators learned the hard way that a single power hiccup can cascade into hours of downtime. That’s why engineers pair UPS and dual power supply designs with fiber backhaul and, yeah, sometimes a gigabit fiber media converter to keep critical links alive. The problem isn’t fanciful; it’s simple: redundancy gaps cause service loss, safety risks, and costly recovery.

gigabit fiber media converter

Concrete risks and what they cost

Loss of PoE to edge devices, interrupted telemetry, failed alarms — these are immediate outcomes when a 4‑port switch loses power. MTBF numbers mean squat if the site has a single PSU sitting on a floor that floods. Link aggregation won’t help if the copper side is dark and the fiber uplink is down. Real costs show up as emergency truck rolls, SLA penalties, and frustrated ops teams who have to patch things manually.

Core redundancy requirements — plain and technical

Keep it tight. The essentials include:

– Dual power supply (or modular hot‑swap PSU) so the unit stays alive during a fault.
– UPS or battery backup for graceful shutdown and transient ride‑through.
– Hot‑swap capability to replace a failing module without disconnecting live links.
– SFP support and ruggedized single mode fiber links for remote uplinks.

gigabit fiber media converter

Design targets: aim for N+1 resiliency on power feeds, specify MTBF that fits your uptime goals (think five‑nines vs. three‑nines), and validate hold‑up time on the UPS to match shutdown windows. These are industry terms but also practical specs you’ll demand on the purchase order.

Implementation paths that actually work

Options vary by site. You can go with an internal dual PSU inside the switch, or standardize an external redundant PSU shelf that serves multiple units. In dirty environments, keep PSUs elevated and give them separate feed circuits. Pairing the switch’s fiber uplink with an external media converter gigabit single mode can isolate electrical storms from the optical path and let you swap optics without touching the switch’s power plane. SFP modules and properly terminated single mode fiber reduce rework and lower failure rates.

Common mistakes seen on the street

Teams skip the obvious: they buy a single cheap PSU to save money, or they rely on default hold‑up times that don’t cover firmware updates. Others forget to provision separate circuits — both AC feeds coming from the same breaker is a false redundancy. During one production teardown I witnessed a site that had redundant PSUs but both were tied to one UPS; redundancy at component level, but not at circuit level. — That kind of oversight kills uptime.

Testing and operational teardown

Run fault injection tests on day one. Simulate PSU failure, pull the primary feed, and validate that PoE stays stable and that the fiber link survives switchover. In our operational production teardown we swapped a gigabit fiber media converter into the uplink, replaced a single mode SFP, and verified reconverge times under 5 seconds. Document reconnection behavior, log time to failover, and measure the actual hold‑up time under load. Those facts beat vendor claims every time.

Summary and golden rules for picking the right setup

Stick to three evaluation metrics: measurable failover time, independent circuit feeds, and real hold‑up time under load. First, require documented failover times under worst‑case load. Second, insist on physically separated AC feeds and clear labeling so a single breaker trip won’t kill both PSUs. Third, test hold‑up time with the full PoE load and verify hot‑swap behavior. These are actionable checks that protect operations and simplify maintenance — and they’re exactly where robust vendors make their case.

Trust vendors that deliver tested results and modular options — that’s how teams move from reactive fixes to steady uptime, and why smart shops choose hardware and converters that stand up to field conditions like those in Lower Manhattan post‑Sandy. WINTOP. —

0 comments
0 FacebookTwitterPinterestEmail